Skip to content
Knurling · Fastener manufacturing process

Knurling

Send a drawing, a sample or a photograph. Samples follow within 7 days of the drawing being approved.

Request a quotation One business day for a reply.

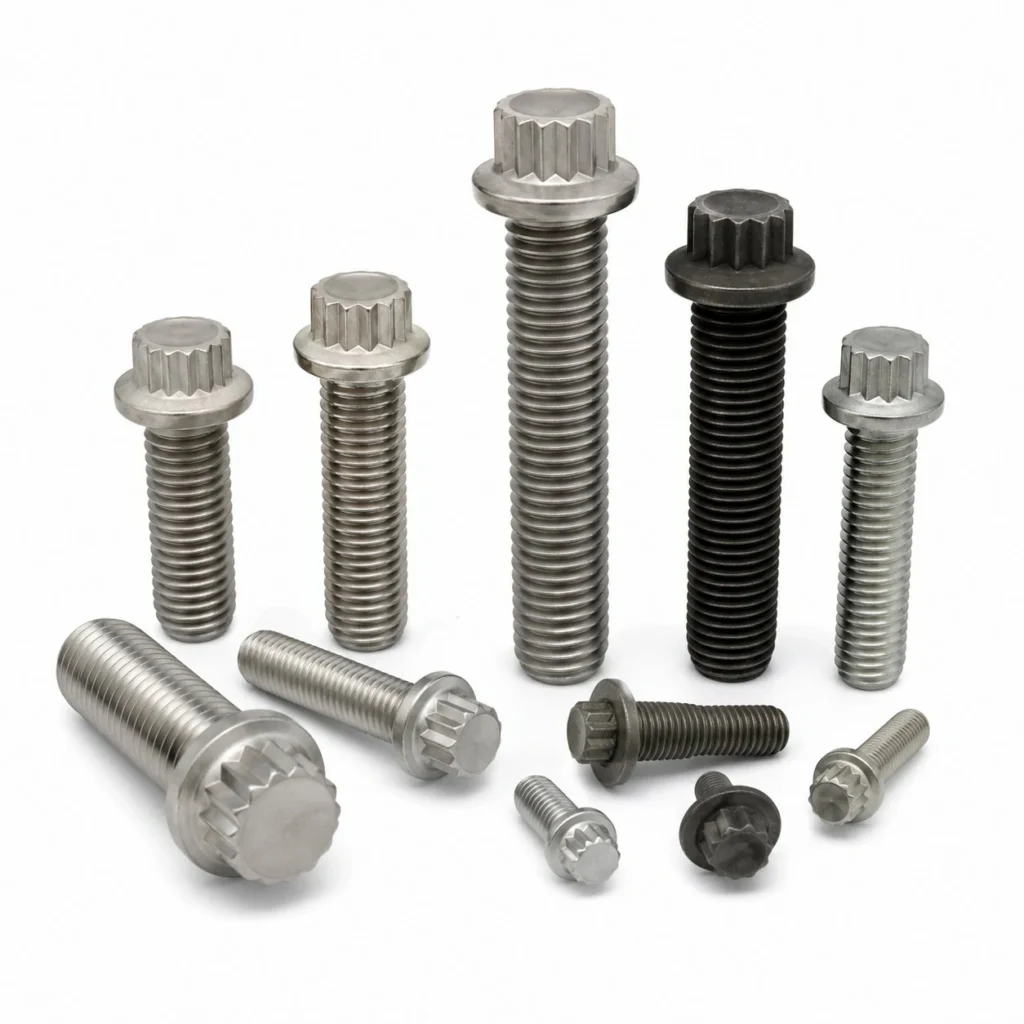
12-Point Screws – Bolts

Knurling is used at Engineering Hardware to make custom screws, threaded inserts, nuts to a customer drawing. Rolling a pattern into a surface to make it grip — either a hand or an anchoring surface. The minimum order is 2,000–5,000 pieces and samples follow within 7 days of the drawing being approved.

Rolling a pattern into a surface to make it grip — either a hand or an anchoring surface.

Two quite different jobs share the name. A straight or diamond knurl on a thumb screw is there for fingers. A knurl under the head of an insert or a press-fit part is there to bite into the parent material and stop it turning, and its dimensions are a fit calculation rather than a cosmetic choice. Like thread rolling it is a forming operation, so the material is displaced and the diameter grows.

What Knurling is the right choice for

  • Thumb screws and hand-operated parts
  • Anti-rotation on inserts, press-fit studs and moulded-in parts
  • Adding grip without a secondary component

Where it is the wrong choice

  • The diameter grows as material is displaced — the blank must allow for it
  • Brittle materials crack rather than flow

Parts produced this way

Usually combined with

Knurling is rarely the only operation on a part. On most jobs it sits in a sequence with:

Order terms

Minimum order
2,000–5,000 pieces. The exact figure depends on the part: it is set by the tooling the drawing calls for, and is confirmed when the drawing has been reviewed.
Samples
Within 7 days of drawing approval.
Drawing
Preferred, but not required — a sample, photographs or a sketch is enough to start.

What a quotation needs

Nine things, and a drawing settles most of them at once. Where a field is unknown, say so — an assumption stated is better than a blank, and several of these can be recommended rather than specified.

Drawing
A 2D drawing (PDF or DWG) or a 3D model settles almost every other question on this list at once.
Dimensions
Diameter, length, head size and any features — enough to know what is being made.
Tolerance
Tolerance is the single biggest cost driver. Tell us which dimensions are critical and which are not — holding everything tight costs money on features nobody measures.
Material
Carbon steel, alloy steel, stainless, brass, aluminium, titanium — or the application, and we will suggest one.
Strength grade
Property class to ISO 898-1 (8.8, 10.9, 12.9) or stainless class to ISO 3506 (A2-70, A4-80). This decides the material and the heat treatment together.
Thread standard
Metric coarse, metric fine, UNC, UNF, BSW or a pipe thread — and the tolerance class if it is specified.
Surface finish
Zinc, hot-dip galvanised, black oxide, Dacromet, Geomet, nickel, passivation, or plain. Salt-spray hours if you have a requirement.
Quantity
Annual volume and first-order quantity. Volume changes which process is the right one, so it changes the price more than most buyers expect.
Application & environment
What the part holds together, and what it has to survive — temperature, vibration, chemicals, salt. This is what lets us catch a specification that will not work before it is made.

Draw it here

No CAD, no account, nothing to install. Draw the part in your browser, generate a real ISO metric thread from M1 to M100 with the end treatment it needs, dimension it, and export a PDF or a DXF to attach below. Sheets run to two metres for long studs and threaded rod.

Open the drawing builder

Questions

What is the minimum order quantity for a custom part?

Between 2,000 and 5,000 pieces for most parts. The exact figure depends on the part: it is set by the tooling the drawing calls for, and is confirmed when the drawing has been reviewed.

How long does a sample take?

Within 7 days once the drawing has been approved. The drawing stage comes first, and for a part being reverse-engineered from a sample it is where most of the time goes.

Can you make a part without a drawing?

Yes. A physical sample, photographs against a scale, or a dimensioned sketch are all workable starting points. A drawing is produced from whichever of those you have and sent back for approval before anything is made.

When is Knurling not the right process?

The diameter grows as material is displaced — the blank must allow for it. Brittle materials crack rather than flow.

Which fasteners are made by knurling?

In this catalog: screw, threaded insert, nut. Whether it is the right process for a particular part depends on the drawing and the quantity.

Parts of this kind we already make

Showing 36 of 78

080 – Hex Socket Flat Point Set Screw — GB/T 77 / ISO 4026 (Series 019) — GB/T 77 / ISO 4026
082 – Hex Socket Flat Point Set Screw — GB/T 77 / ISO 4026 (Series 021) — GB/T 77 / ISO 4026
083 – Hex Socket Cone Point Set Screw — GB/T 77 / ISO 4026 (Series 022) — GB/T 77 / ISO 4026
084 – Torx Countersunk Head Screw — GB/T 2673 / ISO 14583 (Series 023) — GB/T 2673 / ISO 14583
085 – Torx Recessed Countersunk Screw — GB/T 2673 / ISO 14587 (Series 024) — GB/T 2673 / ISO 14587
088 – Hex Socket Cone Point Set Screw — GB/T 78 / ISO 4027 (Series 027) — GB/T 78 / ISO 4027
089 – Phillips Countersunk Self-Tapping Screw — GB/T 846 / ISO 7050 (Series 028) — GB/T 846 / ISO 7050
090 – Phillips Countersunk Machine Screw — GB/T 819.1 / ISO 7046 (Series 029) — GB/T 819.1 / ISO 7046
091 – Phillips Countersunk Machine Screw — GB/T 819.1 / ISO 7046 (Series 030) — GB/T 819.1 / ISO 7046
092 – Phillips Countersunk Machine Screw — GB/T 819.1 / ISO 7046 (Series 031) — GB/T 819.1 / ISO 7046
093 – Phillips Pan Head Self-Tapping Screw — GB/T 845 / ISO 7049 (Series 032) — GB/T 845 / ISO 7049
094 – Phillips Pan Head Machine Screw — GB/T 818 / ISO 7045 (Series 033) — GB/T 818 / ISO 7045
095 – Phillips Pan Head Machine Screw — GB/T 818 / ISO 7045 (Series 034) — GB/T 818 / ISO 7045
096 – Phillips Pan Head Machine Screw — GB/T 818 / ISO 7045 (Series 035) — GB/T 818 / ISO 7045
099 – Slotted Flat Point Set Screw — GB/T 73 / ISO 4766 (Series 038) — GB/T 73 / ISO 4766
100 – Slotted Countersunk Head Screw — GB/T 68 / ISO 2009 (Series 039) — GB/T 68 / ISO 2009
101 – Slotted Pan Head Screw — GB/T 67 / ISO 1580 (Series 040) — GB/T 67 / ISO 1580
102 – Slotted Long Dog Point Set Screw — GB/T 75 / ISO 7435 (Series 041) — GB/T 75 / ISO 7435
103 – Clamping Handle Screw (Short) — DIN 6336 / GN 313 (Series 042) — DIN 6336 / GN 313
104 – Clamping Handle Screw (Medium) — DIN 6336 / GN 313 (Series 043) — DIN 6336 / GN 313
105 – Clamping Handle Screw (Long) — DIN 6336 / GN 313 (Series 044) — DIN 6336 / GN 313
106 – Sheet-Metal Self-Tapping Screw — GB/T 845 / ISO 7049 (Series 045) — GB/T 845 / ISO 7049
107 – Heavy Hex Socket Head Cap Screw — GB/T 1228 / ASTM A325 (Series 046) — GB/T 1228 / ASTM A325
12-Point-Screws-Bolts-Applications
310Micro-JCIS-Micro-Screws
Adjusting Screws
Apple-iPhone-P2-Pentalobe-Bottom-Screws
Apple-iPhone-PH000-PH00-Internal-Screws
Apple-iPhone-Standoff-Screws
Apple-iPhone-Torx-Plus-4IP-Internal-Screws
Apple-iPhone-Y000-Tri-Point-Internal-Screws
asme-b18-2-1-6-unc-hex-head-cap-screw
asme-b18-2-1-8-unc-hex-flange-cap-screw
asme-b18-2-2-1ab-unc-machine-screw-nuts
asme-b18-3-1g-unc-low-head-socket-cap-screw
asme-b18-3-2-unc-flat-head-socket-cap-screw

These are catalog parts, shown to say what the tooling already covers. A special is quoted from your drawing, not from this list.

Drawing builder

Draw the part, dimension it, and export a PDF or a DXF to attach to the form below.

FASTENER DRAWING

CMD
Fastener drawing builder https://engineeringhardware.com/

Nothing you draw is uploaded until you send it, and the drawing lives in your own browser — export it before you close the tab.

Send the part

A drawing answers most of this at once. If you do not have one, fill in what you know and attach a photograph — samples follow within 7 days of the drawing being approved.

The only field we cannot do without — it is where the quotation goes.
A 2D drawing (PDF or DWG) or a 3D model settles almost every other question on this list at once.
Diameter, length, head size and any features — enough to know what is being made.
Tolerance is the single biggest cost driver. Tell us which dimensions are critical and which are not — holding everything tight costs money on features nobody measures.
Carbon steel, alloy steel, stainless, brass, aluminium, titanium — or the application, and we will suggest one.
Property class to ISO 898-1 (8.8, 10.9, 12.9) or stainless class to ISO 3506 (A2-70, A4-80). This decides the material and the heat treatment together.
Metric coarse, metric fine, UNC, UNF, BSW or a pipe thread — and the tolerance class if it is specified.
Zinc, hot-dip galvanised, black oxide, Dacromet, Geomet, nickel, passivation, or plain. Salt-spray hours if you have a requirement.
Annual volume and first-order quantity. Volume changes which process is the right one, so it changes the price more than most buyers expect.
What the part holds together, and what it has to survive — temperature, vibration, chemicals, salt. This is what lets us catch a specification that will not work before it is made.