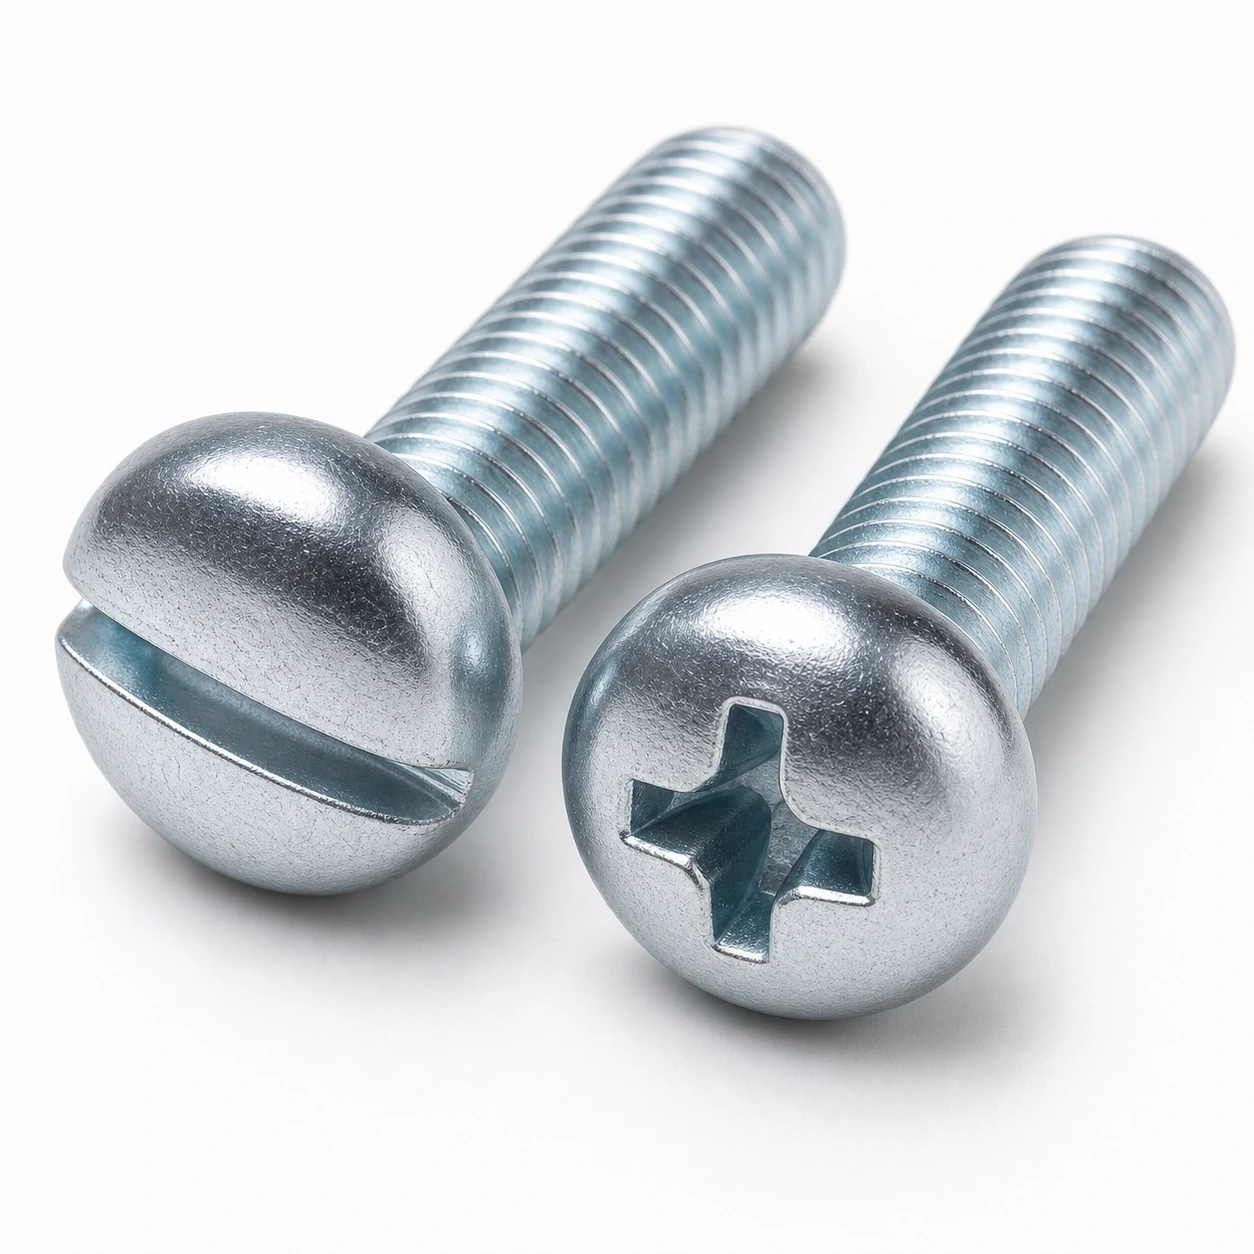
This page covers M2 Pan Head Screws to ISO 7045 / DIN 7985: the full dimensional row, hole and tool sizes, proof-load data and typical applications. All values are taken from the governing standards (ISO 7045 / DIN 7985 together with ISO 273, ISO 724 and ISO 898-1 where applicable).
M2 Dimensional Row (ISO 7045 / DIN 7985)
| Size | Pitch (mm) | Head diameter dk (mm) | Head height k (mm) | Cross recess | Reference standard |
|---|---|---|---|---|---|
| M2 | 0.4 | 3.8 | 1.3 | PH1 | ISO 7045 / DIN 7985 |
Spanner & Drive for M2 Pan Head Screws
M2 Pan Head Screws use a PH1 cross recess. Match the driver bit to the recess (Phillips PH / Pozi PZ are NOT interchangeable).
Hole Sizes for M2
| Coarse-thread pitch (ISO 724) | 0.4 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 2.4 mm |
| Tapping drill, coarse thread | 1.6 mm |
Tightening Torque for M2
| Class 8.8 (dry, ~µ 0.125) | ≈ 0.3 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 0.6 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M2
| Tensile stress area As (ISO 724) | 2.1 mm² |
|---|---|
| Proof load, class 8.8 | 1.2 kN |
| Proof load, class 12.9 | 2 kN |
| Min. ultimate tensile load, class 8.8 | 1.7 kN |
Proof load = tensile stress area × the proof stress Sp of the class, per ISO 898-1 — Sp is a lower figure than the yield stress Rp0.2 and the two are not interchangeable. The stress area is computed from this size's own diameter and pitch, so a fine-pitch designation gives the fine-pitch figure. Design the joint so the working preload stays below the proof load of the class selected.
Installation Tips for M2 Pan Head Screws
- Pozidriv (PZ) drivers ride out of Phillips (PH) recesses and vice versa — confirm the recess marking on the head before assembly.
- For automated assembly, an ACR (Anti-Cam-Out Ribs) or torx-equivalent driver gives noticeably longer bit life than plain PH.
- At M2 the joint is sensitive to over-torque — use a torque-limiting driver and check the head doesn't bury into a softer counterpart.
Mating Parts for M2
For M2, pair with a M2 hex nut (ISO 4032 / DIN 934) and, where used, a M2 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
Custom manufacturing · Made to drawing
Need pan head screws in a size this table does not list?
This page covers M2 pan head screws. Thread size and pitch, length, property class, drive form, head geometry and head marking are all specifiable — the standard part is where it starts, not where it stops. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.