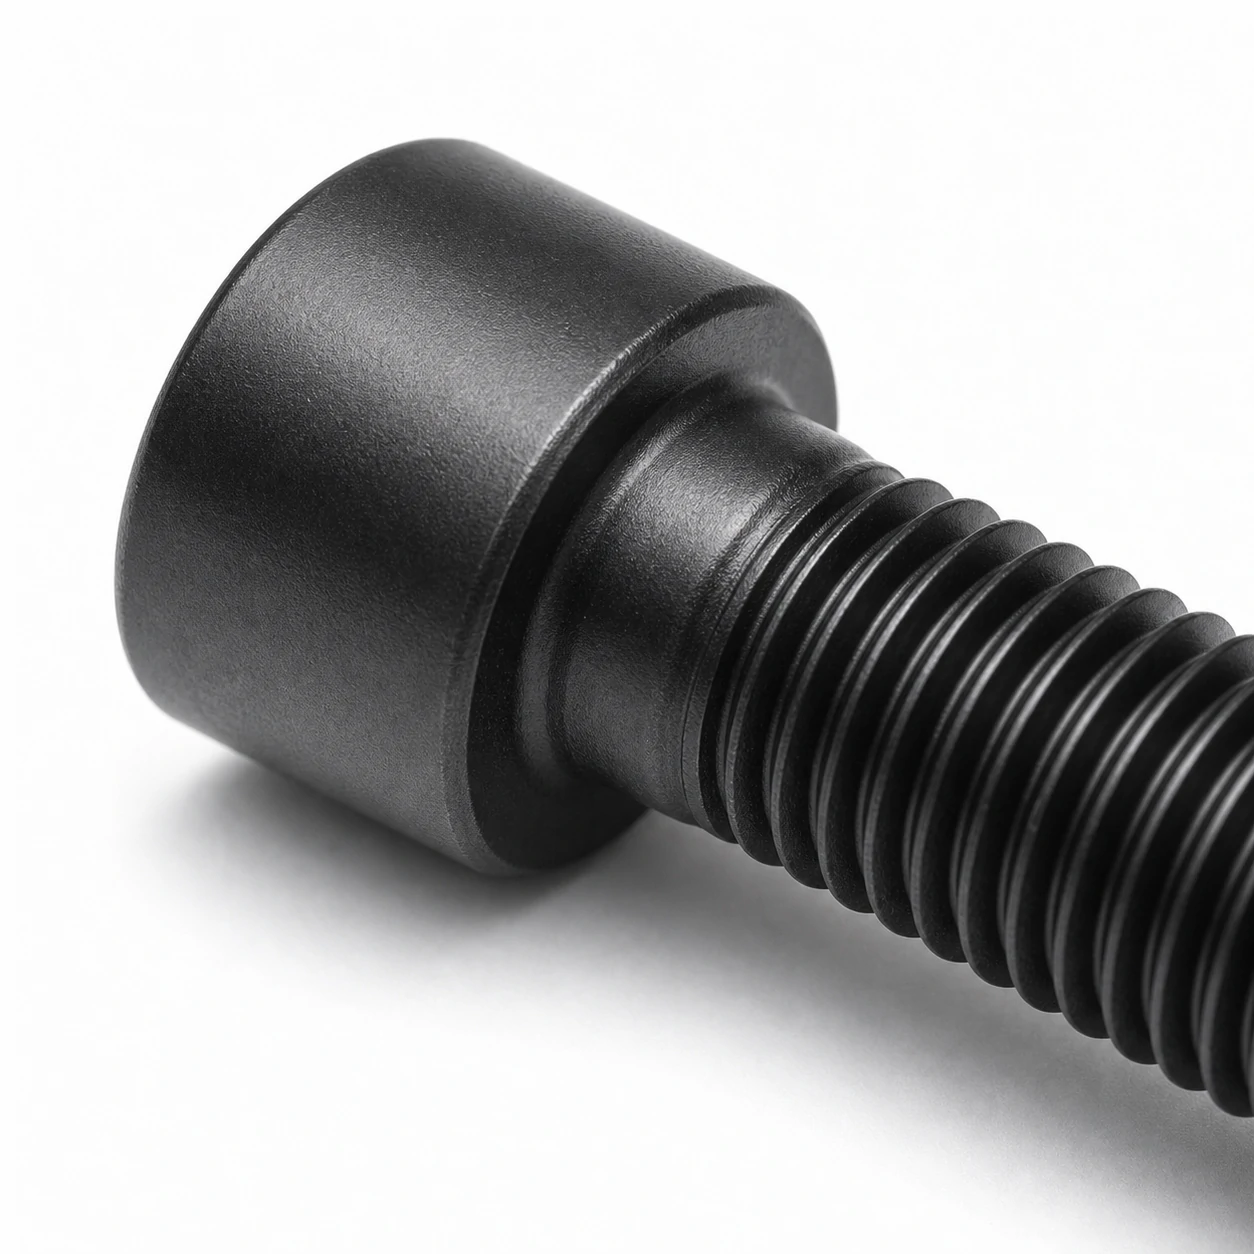
M2 Socket Head Cap Screws are manufactured to ISO 4762 / DIN 912 with a coarse thread pitch of 0.4 mm. This page lists the controlling dimensions for the M2 size — head geometry, width across flats, matching spanner size — together with the clearance hole, tapping drill and tightening torque used at assembly.
M2 Dimensional Row (ISO 4762 / DIN 912)
| Size | Pitch (mm) | Head diameter dk (mm) | Head height k (mm) | Hex key s (mm) | Socket depth t min (mm) | Reference standard |
|---|---|---|---|---|---|---|
| M2 | 0.4 | 3.8 | 2.0 | 1.5 | 1.0 | ISO 4762 / DIN 912 |
Spanner & Drive for M2 Socket Head Cap Screws
The hex socket for M2 Socket Head Cap Screws is shown in the spec table — use the matching Allen / hex key (an ISO 2936 hex key set covers the full range). Ball-end keys are for reaching the screw, not for tightening it — finish on the plain end, and on production work use a torque-controlled driver.
Hole Sizes for M2
| Coarse-thread pitch (ISO 724) | 0.4 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 2.4 mm |
| Tapping drill, coarse thread | 1.6 mm |
Tightening Torque for M2
| Class 8.8 (dry, ~µ 0.125) | ≈ 0.3 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 0.6 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M2
| Tensile stress area As (ISO 724) | 2.1 mm² |
|---|---|
| Proof load, class 8.8 | 1.2 kN |
| Proof load, class 12.9 | 2 kN |
| Min. ultimate tensile load, class 8.8 | 1.7 kN |
Proof load = tensile stress area × the proof stress Sp of the class, per ISO 898-1 — Sp is a lower figure than the yield stress Rp0.2 and the two are not interchangeable. The stress area is computed from this size's own diameter and pitch, so a fine-pitch designation gives the fine-pitch figure. Design the joint so the working preload stays below the proof load of the class selected.
Installation Tips for M2 Socket Head Cap Screws
- Use a quality Allen key fully seated in the socket — partial engagement is the most common cause of stripped sockets at this size.
- For countersunk and button-head variants, chamfer the through-hole to seat the head flush without preloading the head/shank fillet.
- At M2 the joint is sensitive to over-torque — use a torque-limiting driver and check the head doesn't bury into a softer counterpart.
Mating Parts for M2
For M2, pair with a M2 hex nut (ISO 4032 / DIN 934) and, where used, a M2 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
Custom manufacturing · Made to drawing
Need socket head cap screws in a size this table does not list?
This page covers M2 socket head cap screws. Thread size and pitch, length, property class, drive form, head geometry and head marking are all specifiable — the standard part is where it starts, not where it stops. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.