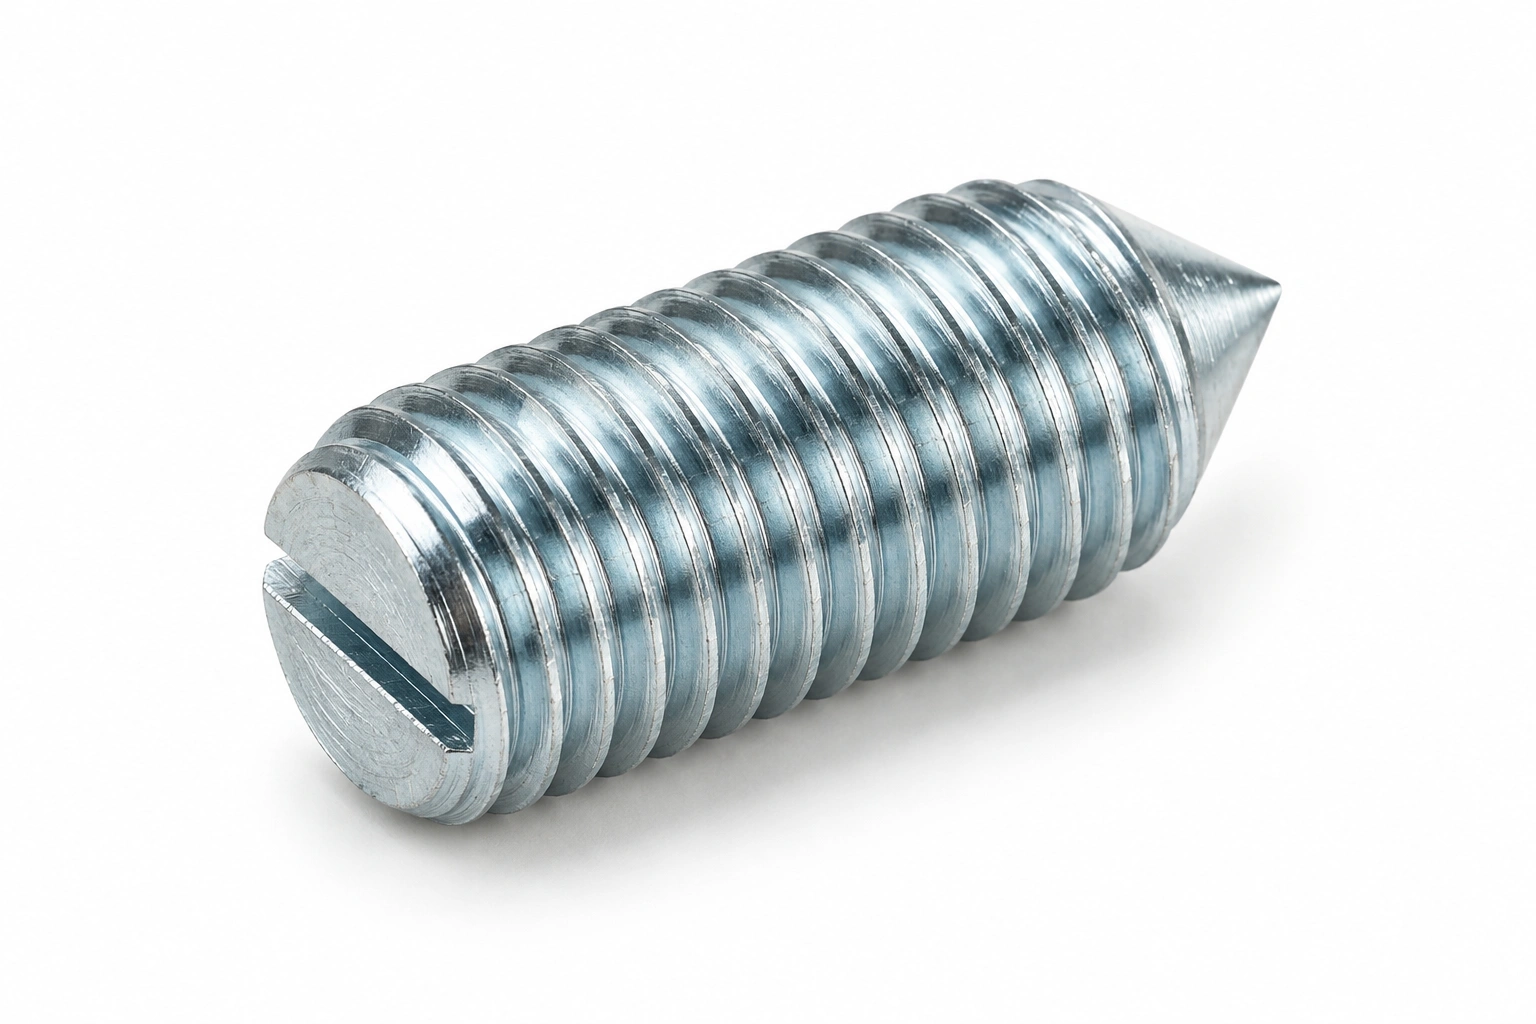
M4 Slotted Set Screws with Cone Point are manufactured to ISO 7434 with a coarse thread pitch of 0.7 mm. This page lists the controlling dimensions for the M4 size — head geometry, width across flats, matching spanner size — together with the clearance hole, tapping drill and tightening torque used at assembly.
M4 Dimensional Row (ISO 7434)
| Size | dt_max (mm) | n_nom (mm) | n_min (mm) | n_max (mm) | t_nom_min (mm) | t_max (mm) | Length range l (mm) | Reference standard |
|---|---|---|---|---|---|---|---|---|
| M4 | 0.4 | 0.6 | 0.66 | 0.8 | 1.12 | 1.42 | 6~20 | ISO 7434 |
Spanner & Drive for M4 Slotted Set Screws with Cone Point
The hex socket for M4 Slotted Set Screws with Cone Point is shown in the spec table — use the matching Allen / hex key (an ISO 2936 hex key set covers the full range). A T-handle key gives the most feel when you are judging preload by hand; anything repeated across a batch wants a torque-controlled driver instead.
Hole Sizes for M4
| Coarse-thread pitch (ISO 724) | 0.7 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 4.5 mm |
| Tapping drill, coarse thread | 3.3 mm |
Tightening Torque for M4
| Class 8.8 (dry, ~µ 0.125) | ≈ 2.9 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 5 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M4
Set screws are rated to ISO 898-5 by hardness, because they work in compression against a shaft rather than in tension. ISO 898-1 excludes them, and a set screw has no head to preload against, so neither a property class nor a preload torque applies. Seating torque depends on the point form and the shaft material.
M4 Slotted Set Screws with Cone Point Weight
A steel M4 slotted set screws with cone point at the listed 620 mm length weighs approximately 61 g each — about 61 kg per 1,000 pieces. Stainless A2/A4 weighs roughly the same (density 7.9–8.0 g/cm³).
Actual weight varies slightly with head form, thread and finish; use this figure for freight estimation only.
Mating Parts for M4
For M4, pair with a M4 hex nut (ISO 4032 / DIN 934) and, where used, a M4 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
When to Step Up or Down from M4
When the joint preload approaches the proof load of M4 class 8.8, step up to M5 class 8.8 (or move to M4 class 10.9). When the joint is over-specified, M3 often saves weight and cost without losing the safety margin.
Custom manufacturing · Made to drawing
Need slotted set screws with cone point in a size this table does not list?
This page covers M4 slotted set screws with cone point. Where the standard stops, the drawing takes over: fine pitches, left-hand threads, partial threading, and property classes above the catalogued grade where material and heat treatment allow. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.