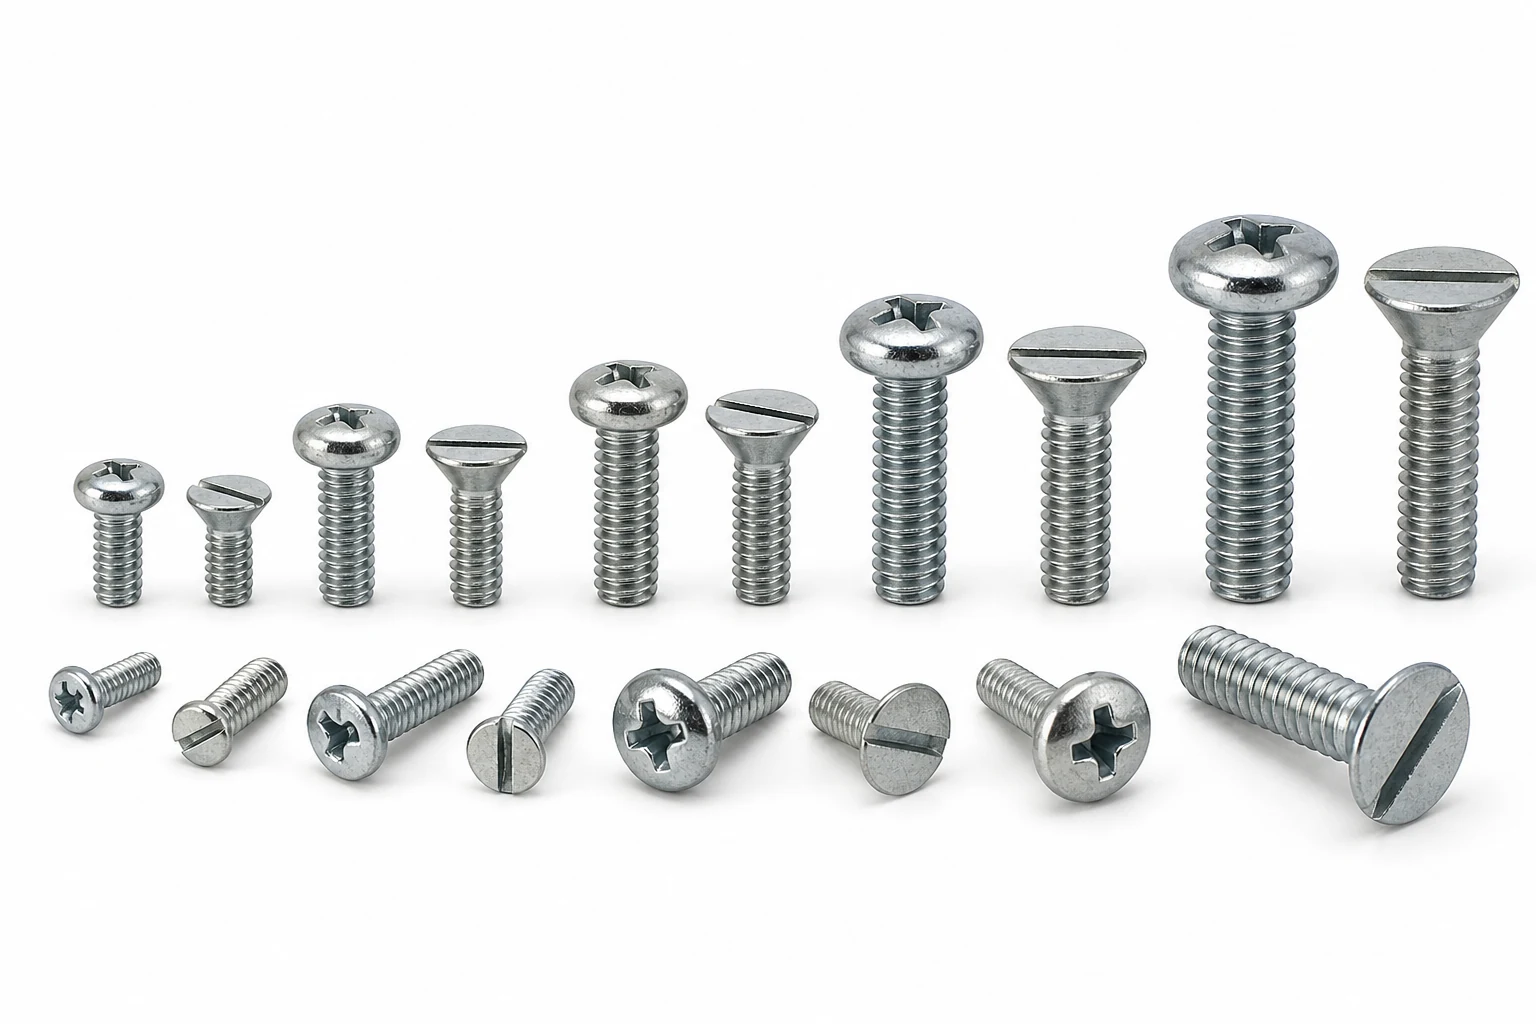
Machine Screws, Inch (UNC & UNF) (ASME B18.6.3) are specified where the joint requires assemblies dimensioned in the inch gauge series, where a metric screw of similar diameter simply will not thread. The sections below cover the typical end-uses by industry, the size and material decisions for each, assembly practice, and the applications this fastener type is not suited to. Stocked across roughly 1 to 10, they cover general to heavy-duty work.
Typical Applications for Machine Screws, Inch (UNC & UNF)
The most common settings where these are specified:
- Appliances & consumer goods: high-volume assembly with power tools and consistent seating.
- Machine guarding & panels: removable access covers that are opened for service.
- General machine building: fastening covers, brackets, motors and sub-assemblies on production equipment.
- Maintenance & repair (MRO): a stocked size for servicing existing plant where the original fastener spec must be matched.
- Fabrication & metalwork: bench and on-site assembly of steel frames, enclosures and weldments.
How to Specify Machine Screws, Inch (UNC & UNF) for Your Application
- Size: Match the nominal size to the mating thread or hole. This product spans 1–10; check the full table below for the exact dimensions of each size.
- Drive & head: Pick the drive (socket, cross, slot) and head style for the tool access and seating surface; a recessed drive resists cam-out under power tools.
- Environment: For damp, coastal or chemical exposure prefer A4/316 stainless or a suitable coating; indoors, plated steel or A2 is usually sufficient.
- Standard: This product is supplied to ASME B18.6.3. Quoting the standard on your order guarantees interchangeable dimensions between suppliers.
Installation & Assembly Practice
- Match the driver exactly to the recess (PH ≠ PZ; hex key sizes per ISO 2936) and keep the tool axial — side load is the main cause of stripped drives.
- In tapped holes, engage a thread length of at least 1× the nominal diameter in steel, 2× in aluminum.
- Set power tools to a torque that seats the head without embedding it into the mating surface.
Common Selection Mistakes with Machine Screws, Inch (UNC & UNF)
- Under-sizing the drive for the installation torque — a small recess at high torque strips before the screw is seated.
- Using a countersunk head in thin sheet where the countersink removes most of the load-bearing material.
- Specifying stainless in high-strength duty: A2-70 is roughly class 7 steel, not a 10.9 substitute.
Where Machine Screws, Inch (UNC & UNF) Are Not the Right Choice
Not for high-preload structural joints (use a property-class bolt and nut), and not in thin sheet where a self-drilling or self-tapping type suits better.
Custom manufacturing · Made to drawing
Need a machine screws, inch (unc & unf) outside the standard range?
Lengths and thread lengths outside the standard table are the commonest request, followed by a drive the standard does not offer and a head marked with your own part number. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.