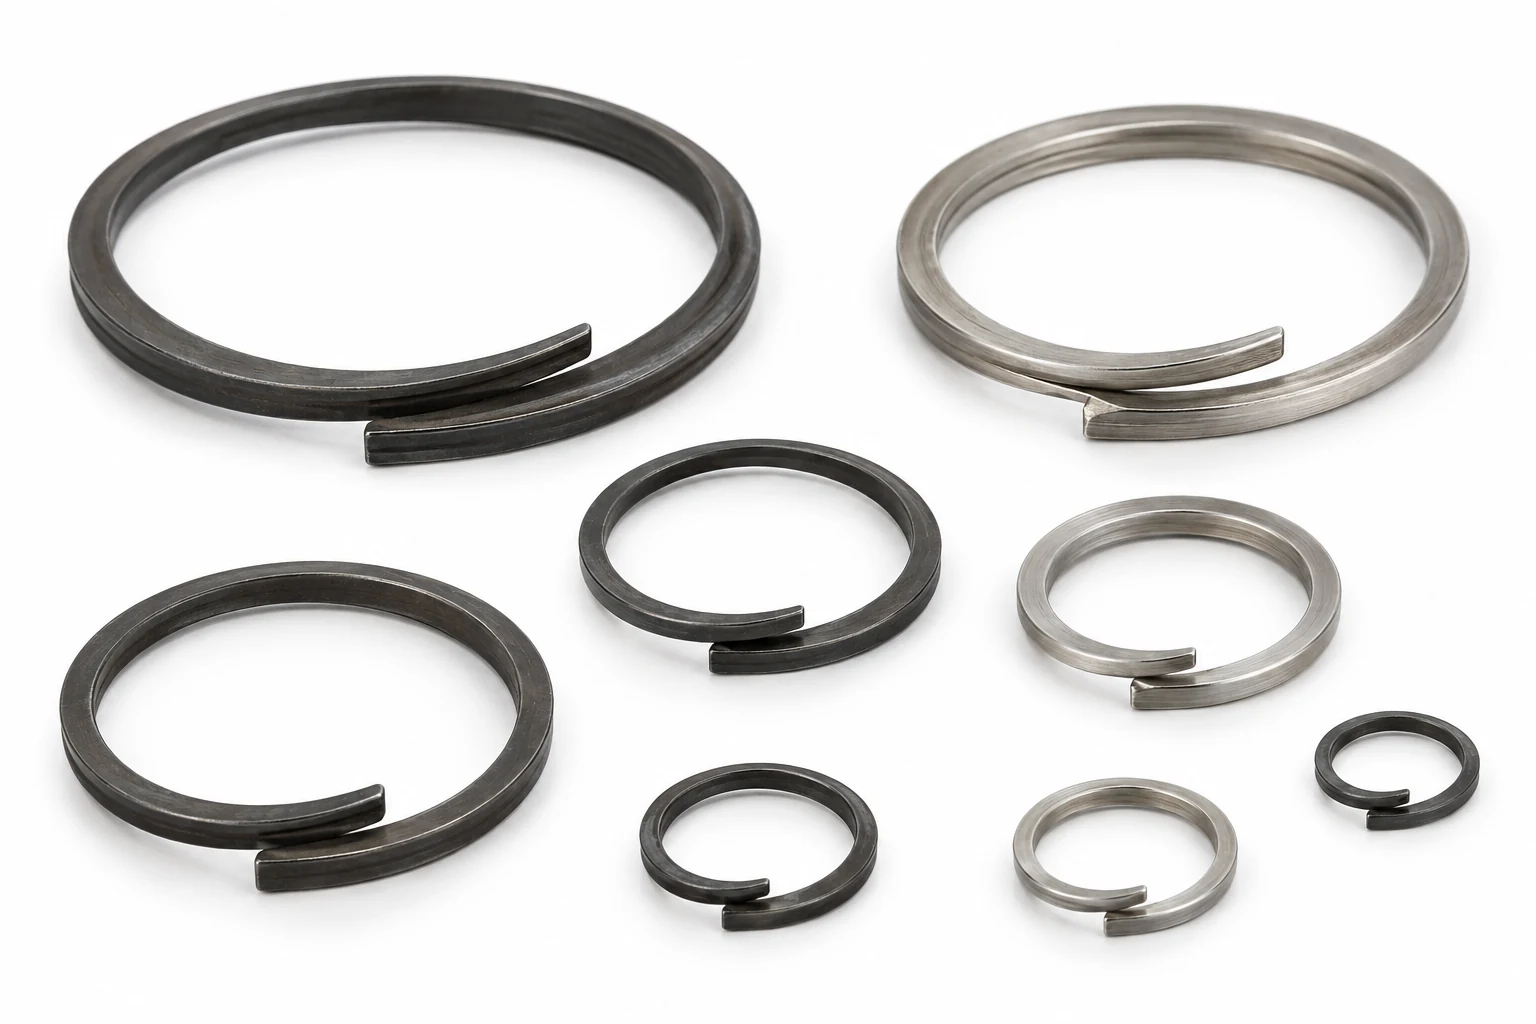
Retaining Rings (Circlips) are retaining rings manufactured to DIN 471 / DIN 472. This page lists the full dimensional range with the key specifications engineers need to select and specify them.
What Are Retaining Rings (Circlips)?
Retaining Rings (Circlips) are retaining rings defined by DIN 471 / DIN 472. They are selected by shaft / bore diameter and the dimensional characteristics shown below, and are available in a range of materials and finishes to suit the application and environment.
Materials & Finishes
Common materials include carbon steel (typically zinc plated or hot-dip galvanized), hardened or case-hardened steel where wear matters, and stainless steel A2 (304) or A4 (316) for corrosion resistance. Specify the material, hardness where relevant, and the surface finish appropriate to your application and environment.
Specification Guides
Each size, material and standard of Retaining Rings (Circlips) has its own reference page with the figures for that one configuration.
Goes With
Hardware commonly specified alongside Retaining Rings (Circlips).
Pricing
Retaining Rings (Circlips) are supplied to order. Pricing starts from approximately US$0.030 per piece for standard sizes in carbon steel; final pricing depends on size, material, finish and order quantity (MOQ applies). Submit your exact configuration with the quote form above.
Custom manufacturing · Made to drawing
Need a retaining rings (circlips) outside the standard range?
Groove dimensions, thickness, material temper and finish decide the part; the ring is made to the groove, so the groove drawing is what is actually needed. Made by stamping.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.
Manufactured in our own plant
This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.
-
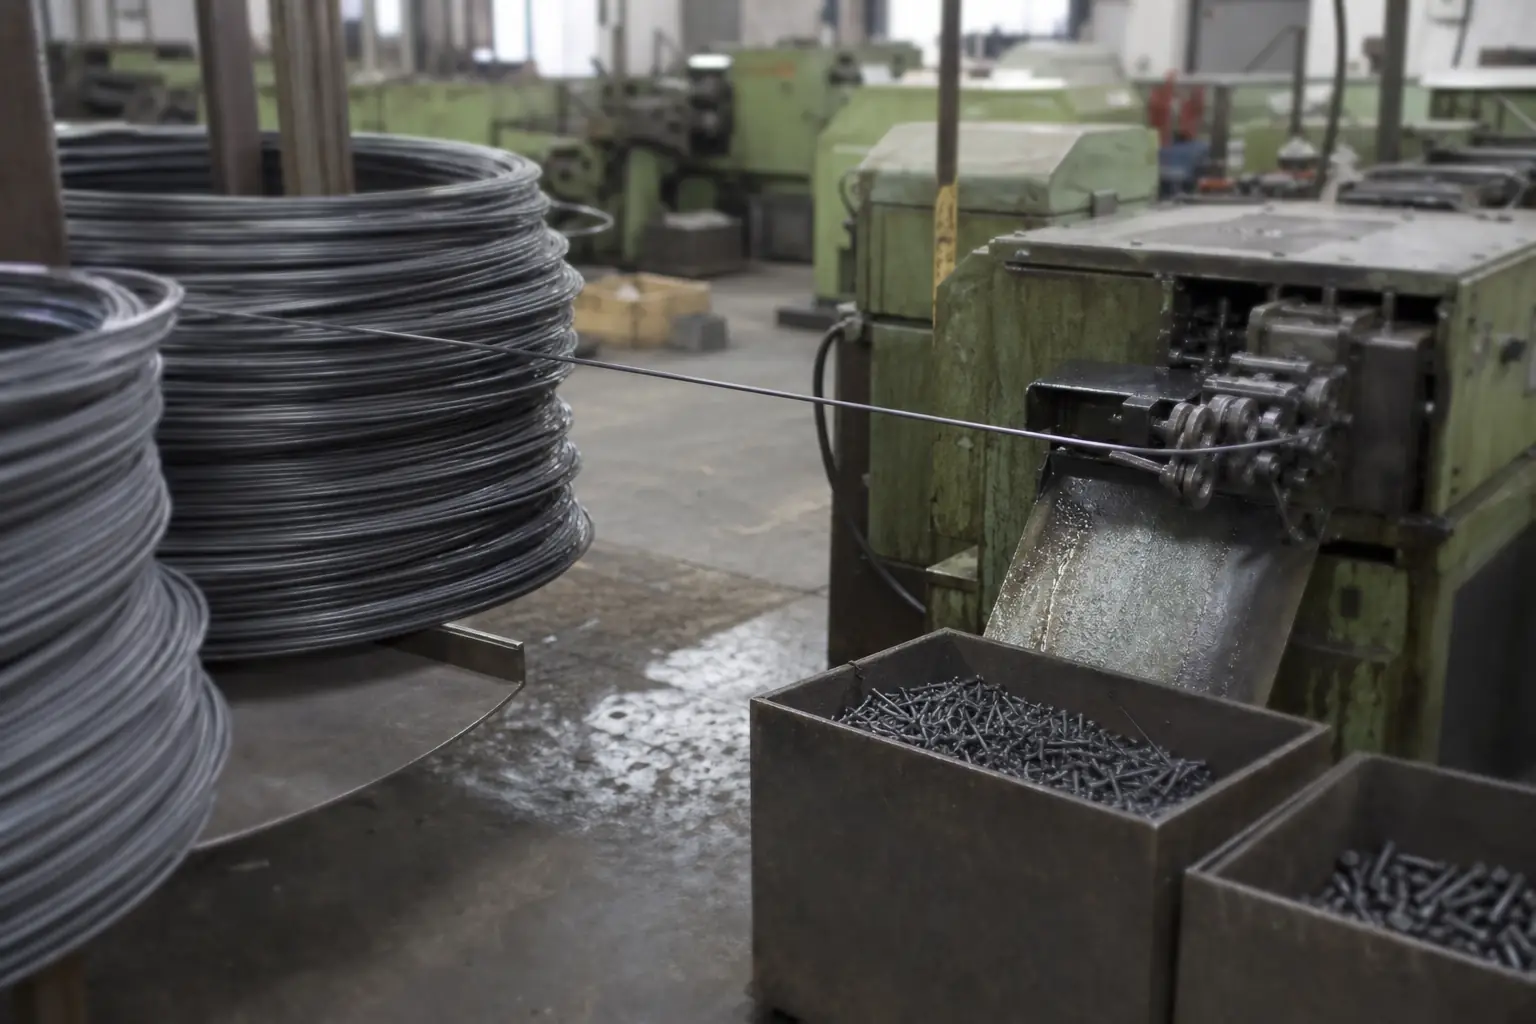
01 Cold heading
Wire rod is drawn to size and cold-formed into blanks. Forming rather than cutting keeps the grain flow continuous around the head, which is where a bolt is most likely to fail.
Head dimensions and under-head radius checked at set-up and per shift.
-
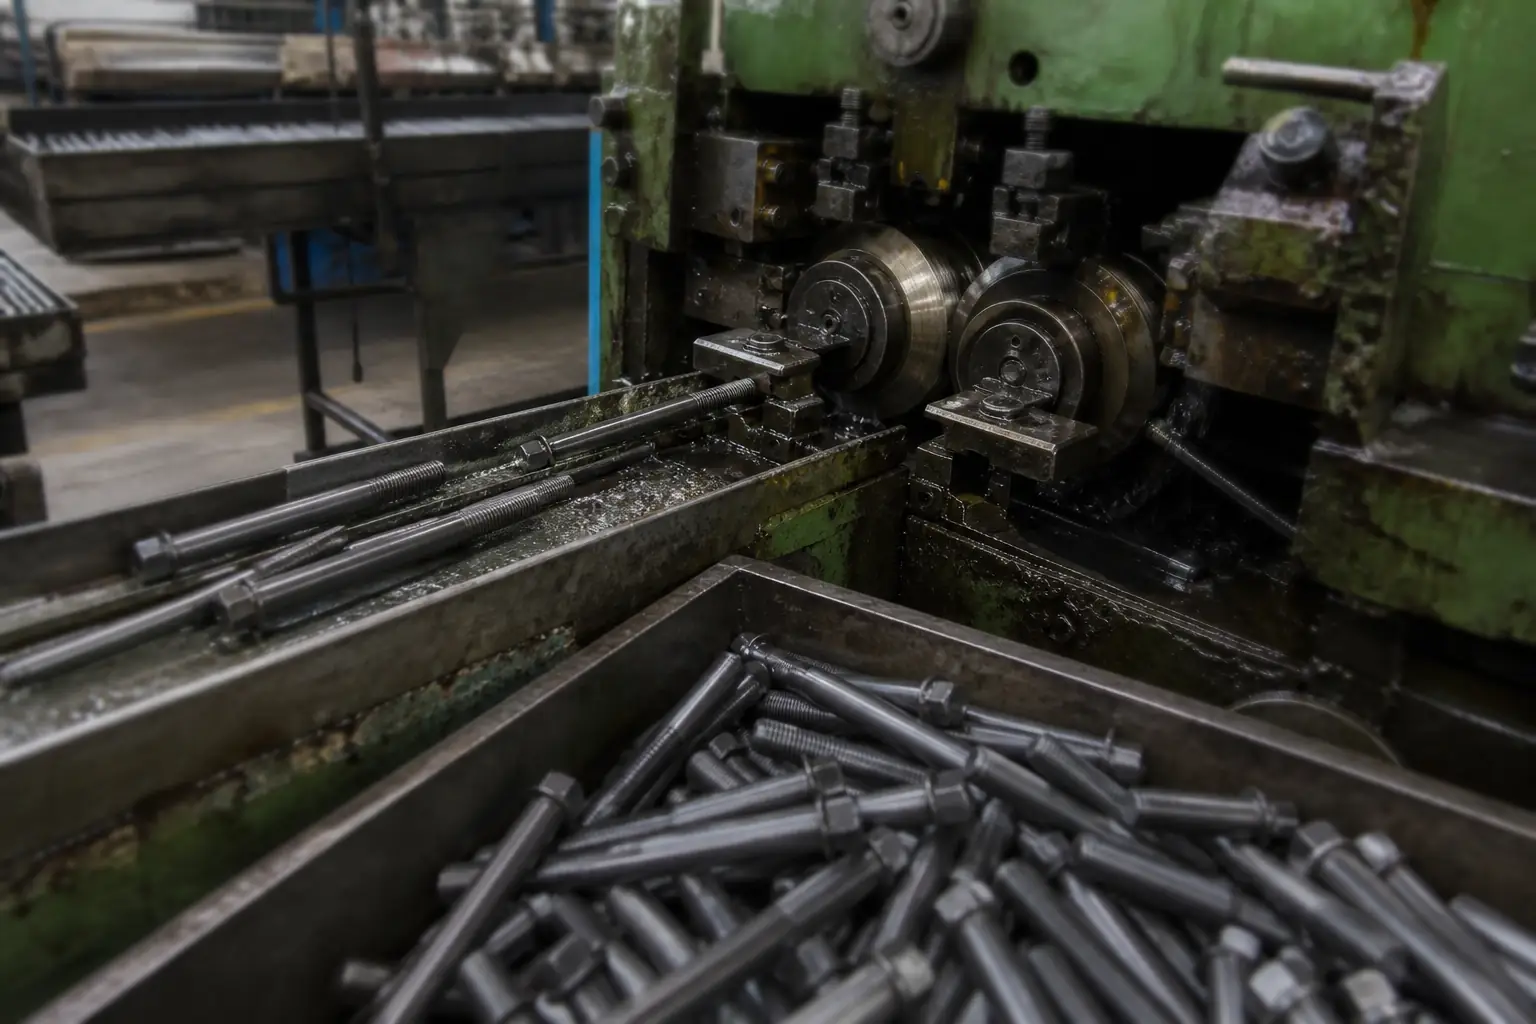
02 Thread rolling
Threads are rolled between hardened dies rather than cut. Rolled threads are stronger in fatigue than cut threads and hold pitch and flank angle far more consistently across a batch.
Go / no-go ring gauges to ISO 965 tolerance class 6g.
-
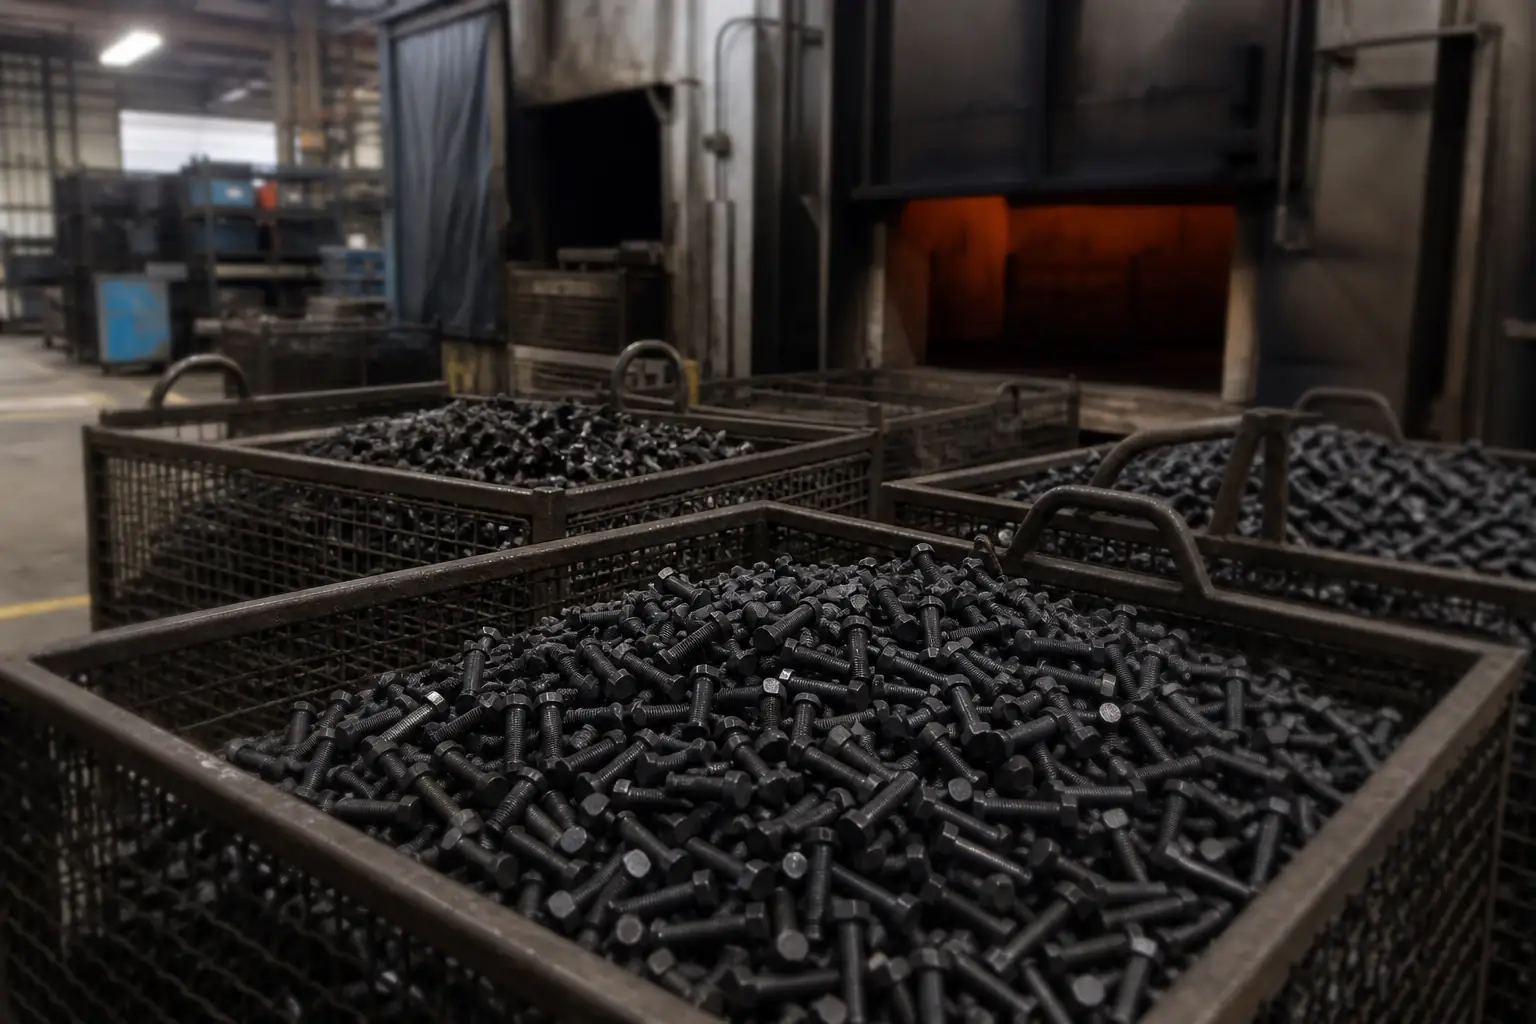
03 Heat treatment
Quench-and-temper brings carbon and alloy steel to the property class ordered — 8.8, 10.9 or 12.9 — with the furnace charge tracked so a finished lot can be traced back to it.
Core hardness and tensile tested per lot to ISO 898-1.
-
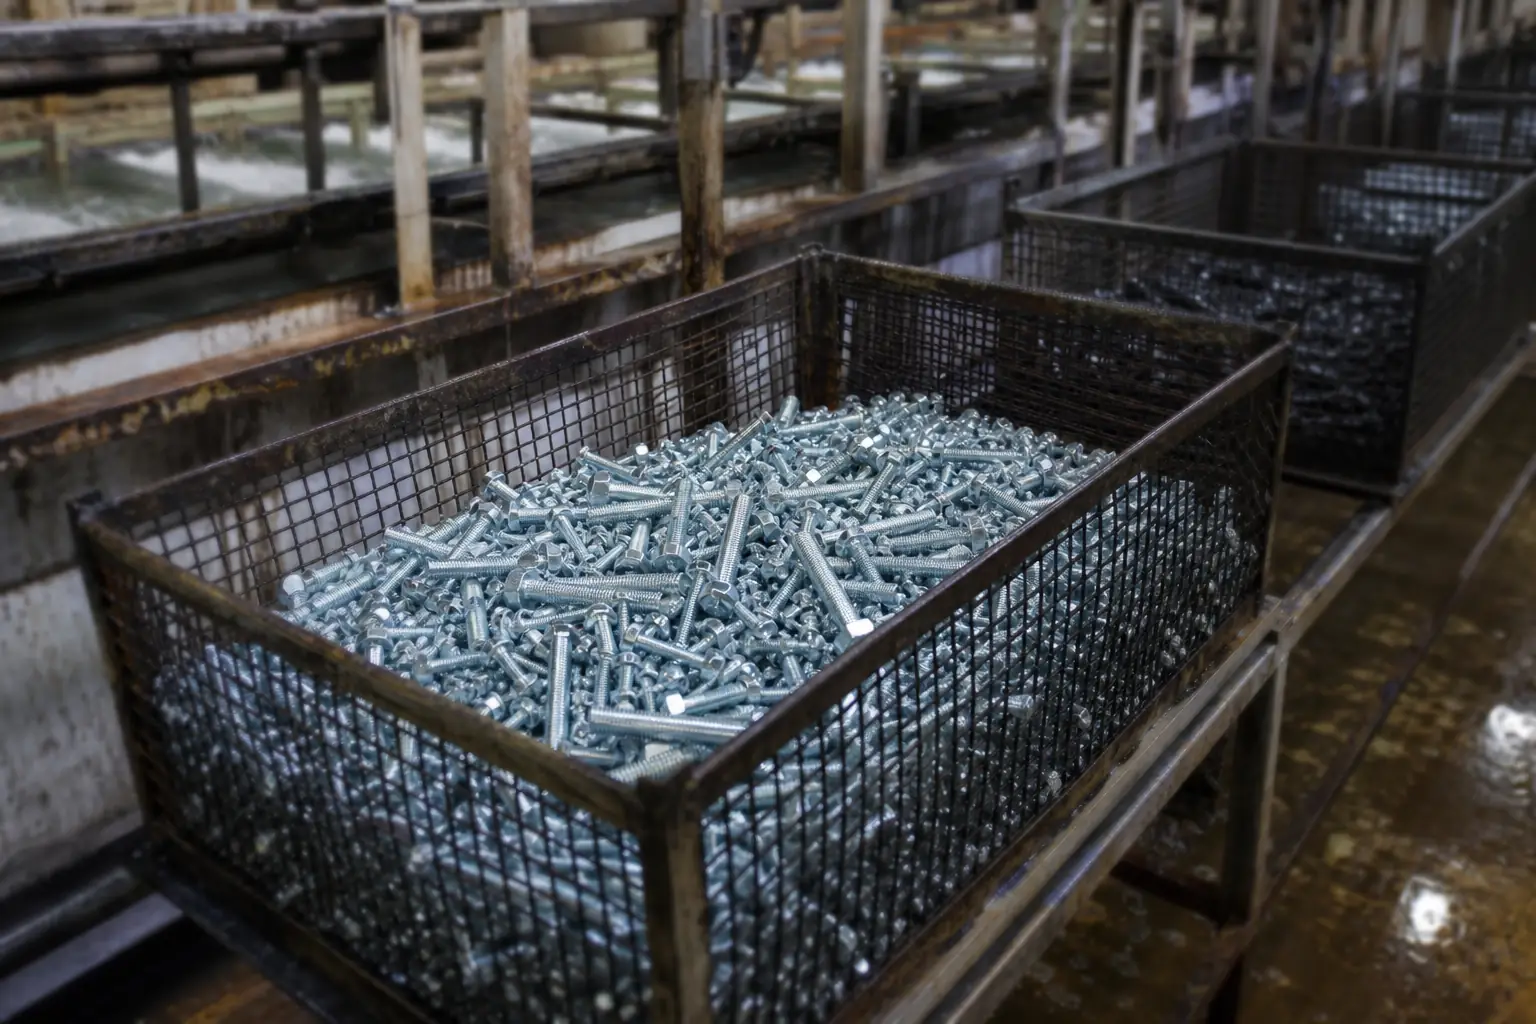
04 Surface treatment
Zinc, zinc-nickel, hot-dip galvanizing, black oxide, phosphate and Dacromet, selected against the service environment rather than against the price list.
Coating thickness and neutral salt spray hours to ISO 9227.