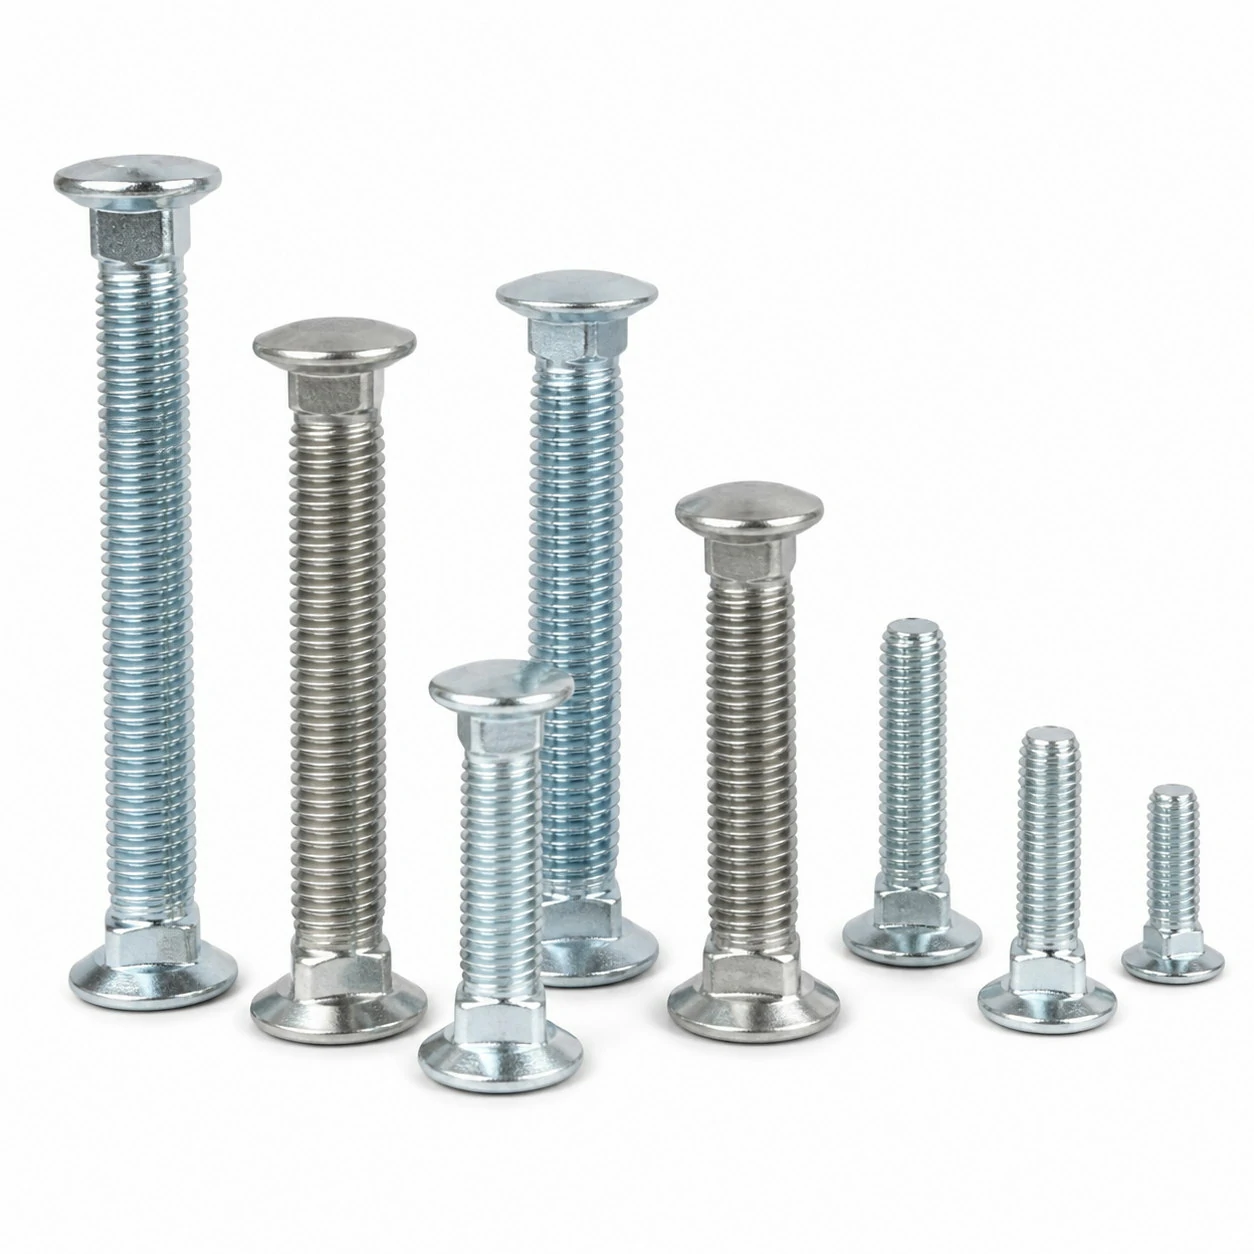
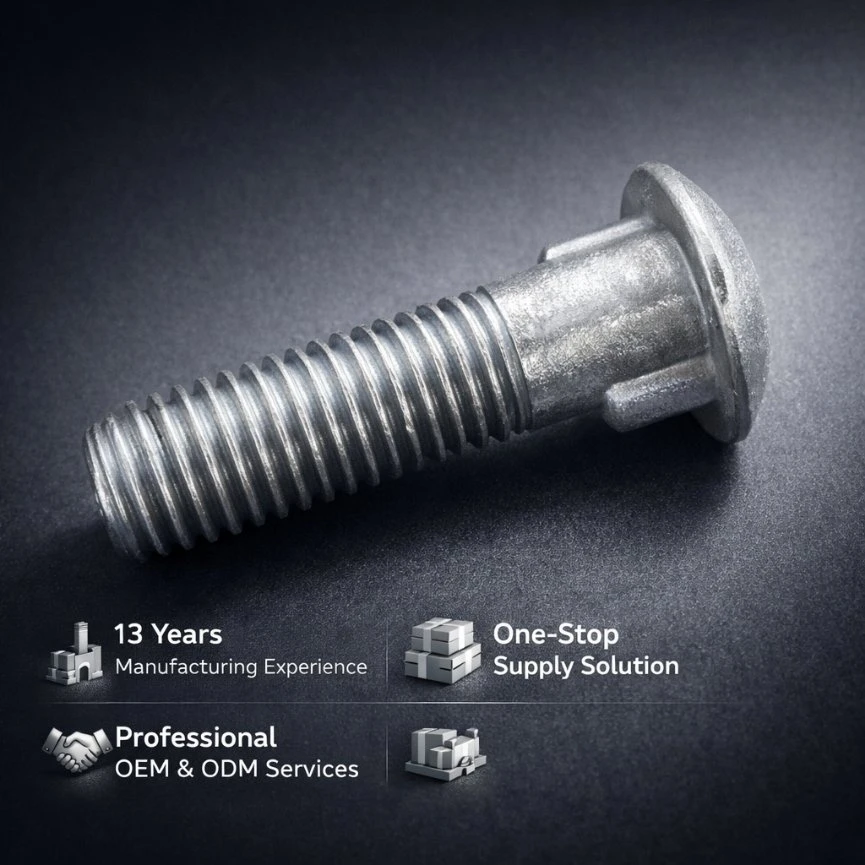
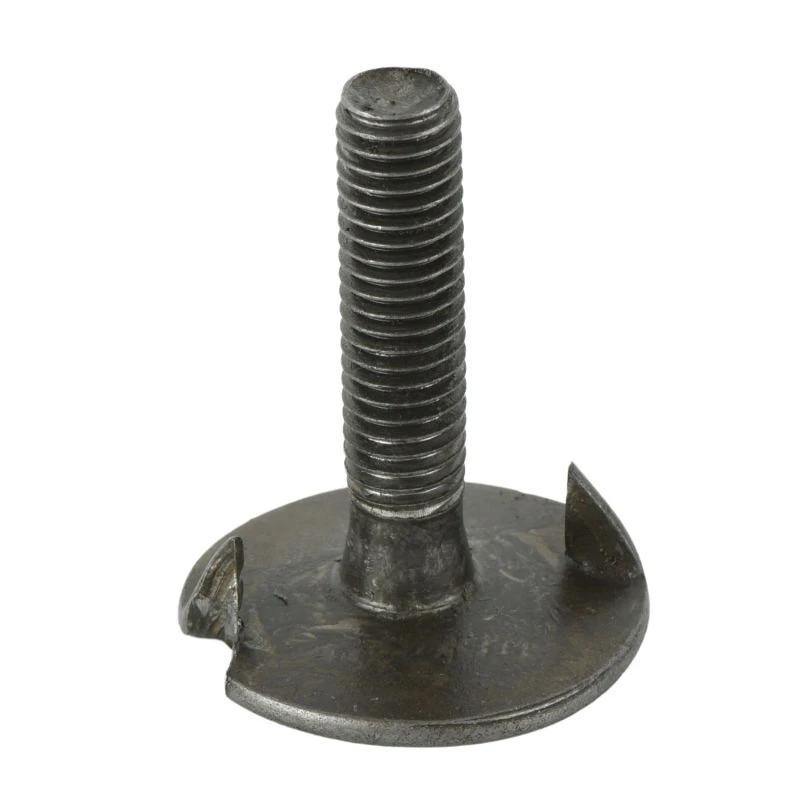
Property Class 8.8 Steel Elevator Bolts are supplied to ISO 898-1 property class 8.8. Corrosion behaviour is requires plating (zinc) for corrosion protection, the material is magnetic, and the usable service range is commonly limited to approx. +300 °C; confirm against the coating and the load. In practice this grade is the workhorse medium-carbon alloy class for structural joints.
- Grade
- ISO 898-1 property class 8.8
- Corrosion resistance
- Requires plating (zinc) for corrosion protection
- Magnetic response
- Magnetic
- Service temperature
- commonly limited to approx. +300 °C; confirm against the coating and the load
Property values are typical for the grade. Certified mechanical test data is available on request for production orders.
Property Class 8.8 Steel (ISO 898-1 property class 8.8) is the workhorse medium-carbon alloy class for structural joints. Specified on elevator bolts it determines the corrosion behaviour (requires plating (zinc) for corrosion protection) and the service temperature range (commonly limited to approx. +300 °C; confirm against the coating and the load); the dimensions are ours rather than a standard's, and are listed in full below.
Why Choose Property Class 8.8 Steel for Elevator Bolts
The workhorse medium-carbon alloy class for structural joints. For elevator bolts, this matters when requires plating (zinc) for corrosion protection is the primary requirement.
Mechanical & Physical Properties
| Grade designation | ISO 898-1 property class 8.8 |
|---|
| Magnetic response | Magnetic |
|---|
| Service temperature | commonly limited to approx. +300 °C; confirm against the coating and the load |
|---|
| Corrosion characteristic | Requires plating (zinc) for corrosion protection |
|---|
Corrosion Behavior in Service
Carbon and alloy steel elevator bolts require a coating for corrosion protection. Zinc plating (with or without passivation) is the most common; hot-dip galvanizing is used for outdoor structural service; black-oxide is mainly a tarnish-prevention finish for tool-room use.
Galvanic & Galling Considerations
For elevator bolts in steel, the dominant compatibility issue is hydrogen embrittlement at high property classes (10.9 and above) when electroplated. Plating must be followed by an appropriate baking treatment, or a non-electroplated finish (mechanical zinc, zinc flake) should be substituted.
Sizes of Elevator Bolts Available in Property Class 8.8 Steel
| Thread size | Pitch (mm) | Head diameter dk (mm) | Head height k (mm) | Square neck width (mm) | Neck depth (mm) | Common length range (mm) | Typical finish |
|---|
| M6 | 1.0 | 19.0 | 2.4 | 6.4 | 5.0 | 16~60 | Zinc plated / A2 |
| M8 | 1.25 | 25.0 | 3.0 | 8.4 | 6.0 | 20~80 | Zinc plated / A2 |
| M10 | 1.5 | 32.0 | 3.5 | 10.5 | 7.0 | 25~100 | Zinc plated / A2 |
| M12 | 1.75 | 38.0 | 4.0 | 12.5 | 8.0 | 30~120 | Zinc plated / A2 |
| M16 | 2.0 | 50.0 | 5.0 | 16.5 | 9.0 | 40~150 | Zinc plated |
Dimensions are independent of the material: every size above is available in Property Class 8.8 Steel.
Custom manufacturing · Made to drawing
Need this bolt in a grade that is not listed?
Grade 8 8 Steel is one of the grades the catalog describes. Thread size and pitch, length, property class, drive form, head geometry and head marking are all specifiable — the standard part is where it starts, not where it stops. Made by cold heading or hot forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.
Custom bolt manufacturingSend a drawing
Applications & Industries
Elevator Bolts are bought for a small number of well-defined jobs. These are the ones we ship them for. Stocked from M6 to M16.
Industries that specify Elevator Bolts
-
Agriculture & grain
Grain elevators, augers and belt-driven handling plant.
-
Recycling & quarrying
Belt fixings that must not tear the carcass.
-
Bulk handling
Buckets and flights bolted to elevator and conveyor belting.
-
Automotive & transport
Chassis, driveline and body fixings that see vibration and are assembled to a controlled preload.
-
Steel fabrication
Bolted connections in frames, enclosures, walkways and weldments, on the bench and on site.
-
Energy & infrastructure
Tower, pipework, switchgear and plant fixings specified for long service life and inspectable joints.
Typical applications
- square neck stops the bolt turning from the inside of the boot
- fixings tightened entirely from the nut side
- a wide flat head that spreads load on rubber belting
- joints where the property class is stated on the drawing
- clamping two machined faces to a calculated preload
- bolting brackets, motors and gearboxes to a frame
Service conditions to specify against
- Marine and coastal
- Available in A4 (316) stainless for chloride exposure — coastal structures, pool halls, water treatment and deck hardware, where A2 will eventually pit.
- High load
- Supplied in ISO 898-1 property classes, so the joint can be designed to a stated proof load and tightened to a calculated torque rather than by feel.
- Torque and preload
- The joint is designed around bolt tension, so lubrication, coating and the friction coefficient all change the torque figure — state them together.
Where to use something else
- Do not use a machine thread into unthreaded sheet or timber; use a tapping screw, rivet nut or insert made for that parent material.
Full application guide: where Elevator Bolts are used, how to specify them, and the cases they are wrong for