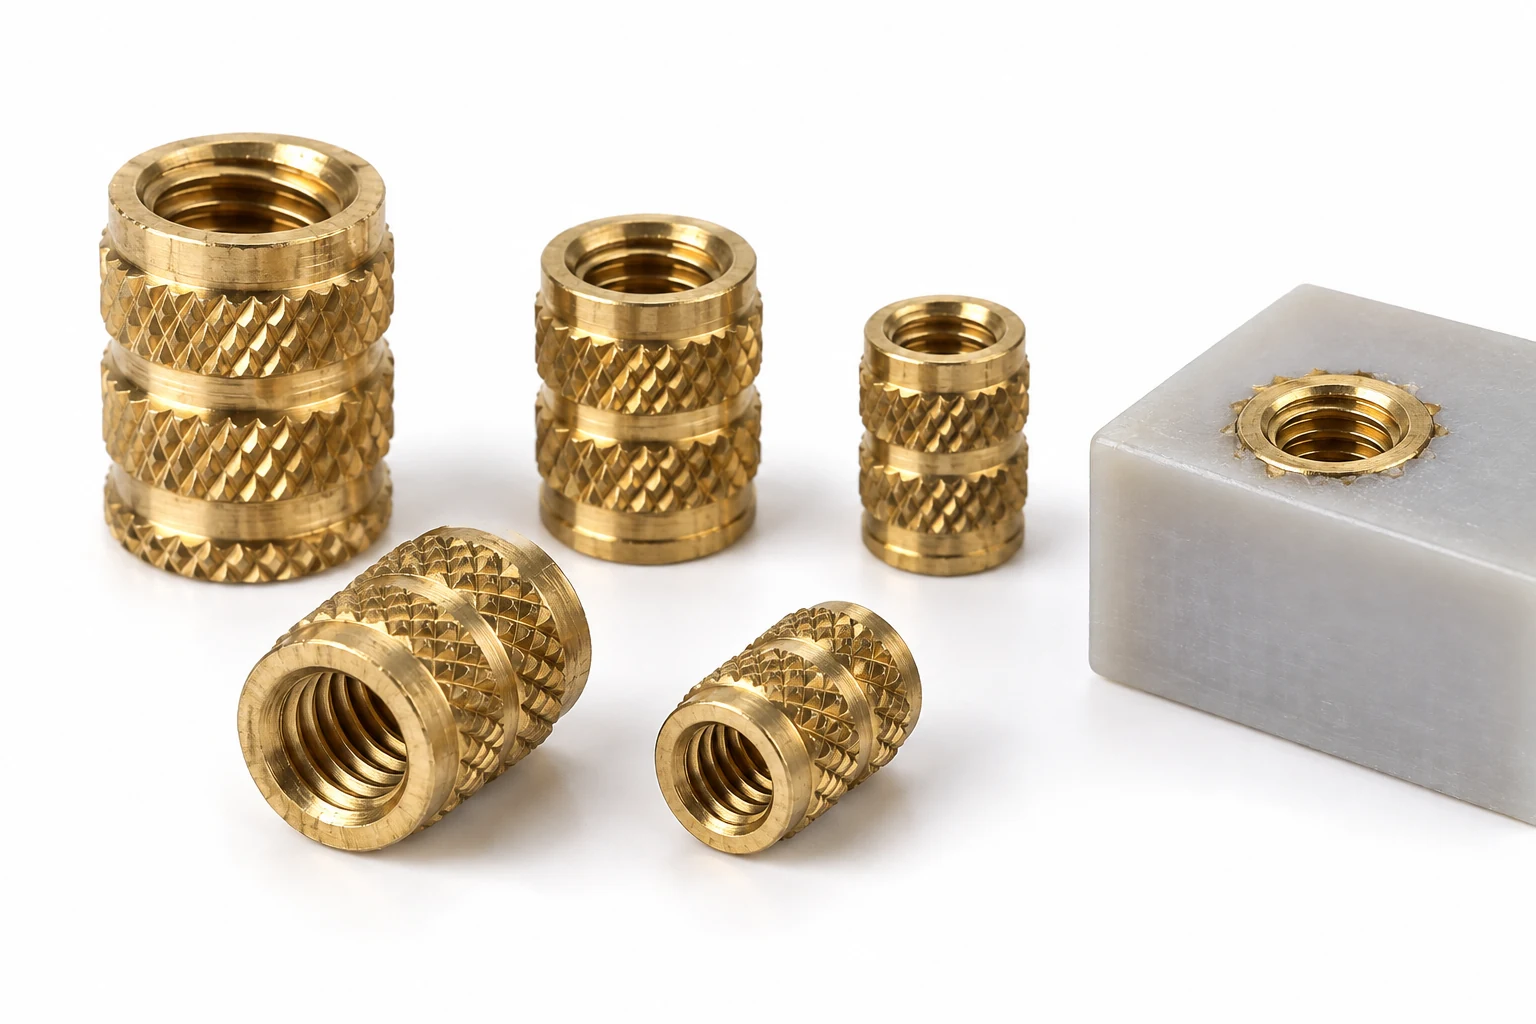
Dimensional data for M3 Heat-Set Threaded Inserts for Plastic to Trade series (heat-set insert), with the installation notes for this type.
Values are taken from the governing standard rather than from a general machine-thread table, because this type is not selected on one.
M3 Dimensional Row (Trade series (heat-set insert))
Thread size
Outer diameter (mm)
Length L (mm)
Hole in parent (mm)
Recommended boss OD (mm)
Knurl bands
Material
Installation
M3
4.6
4.0
4.4
9.2
3
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
Technical Drawing
Customize the parameters below — every spec field is editable, and the drawing redraws to match the values you choose. Changing the size will snap the other fields to that size's standard values; you can then override any individual value.
Sends the selected values to the quote form below.
Request a Quote
The form below follows the current technical drawing configuration. Change the drawing values above and the request details update automatically.
Dimensions & Specifications (Trade series (heat-set insert))
Thread size
Outer diameter (mm)
Length L (mm)
Hole in parent (mm)
Recommended boss OD (mm)
Knurl bands
Material
Installation
M2
3.2
3.0
3.0
6.4
2
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
M2.5
3.6
4.0
3.4
7.2
2
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
M3
4.6
4.0
4.4
9.2
3
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
M3
4.6
5.7
4.4
9.2
3
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
M4
5.6
5.7
5.4
11.2
3
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
M5
6.9
5.8
6.7
13.8
3
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
M6
8.2
9.5
8.0
16.4
3
Brass CuZn39Pb3
Heated tip, 200-250 u00b0C
Applications & Industries for M3 Heat-Set Threaded Inserts for Plastic
The sectors that buy Heat-Set Threaded Inserts for Plastic, and the duty each one buys them for. Stocked from M2 to M6.
Industries that specify Heat-Set Threaded Inserts for Plastic
Consumer electronicsHousings assembled and re-opened for service.
Injection mouldingPost-moulded threads in bosses.
Prototyping & product developmentReal threads in a printed prototype.
Additive manufacturingThreads in printed parts, where layer adhesion will not hold a screw.
Plastics & moulded partsDurable metal threads in housings that would strip if screwed into directly.
Aluminium & castingsReinforced threads in soft alloy, and repair of stripped holes.
Typical applications
installed with a heated tip so the plastic flows into the knurl
boss hole size is the critical dimension, not the insert length
a reusable metal thread in a plastic or printed boss
repairing a stripped hole to its original size
assemblies opened and closed many times over their life
creating a reusable metal thread in a soft or thin parent
Service conditions to specify against
Marine and coastal
Available in A4 (316) stainless for chloride exposure — coastal structures, pool halls, water treatment and deck hardware, where A2 will eventually pit.
Parent material first
The insert type is chosen by what it goes into — moulded plastic, printed polymer, alloy casting or timber — not by the screw that goes into it.
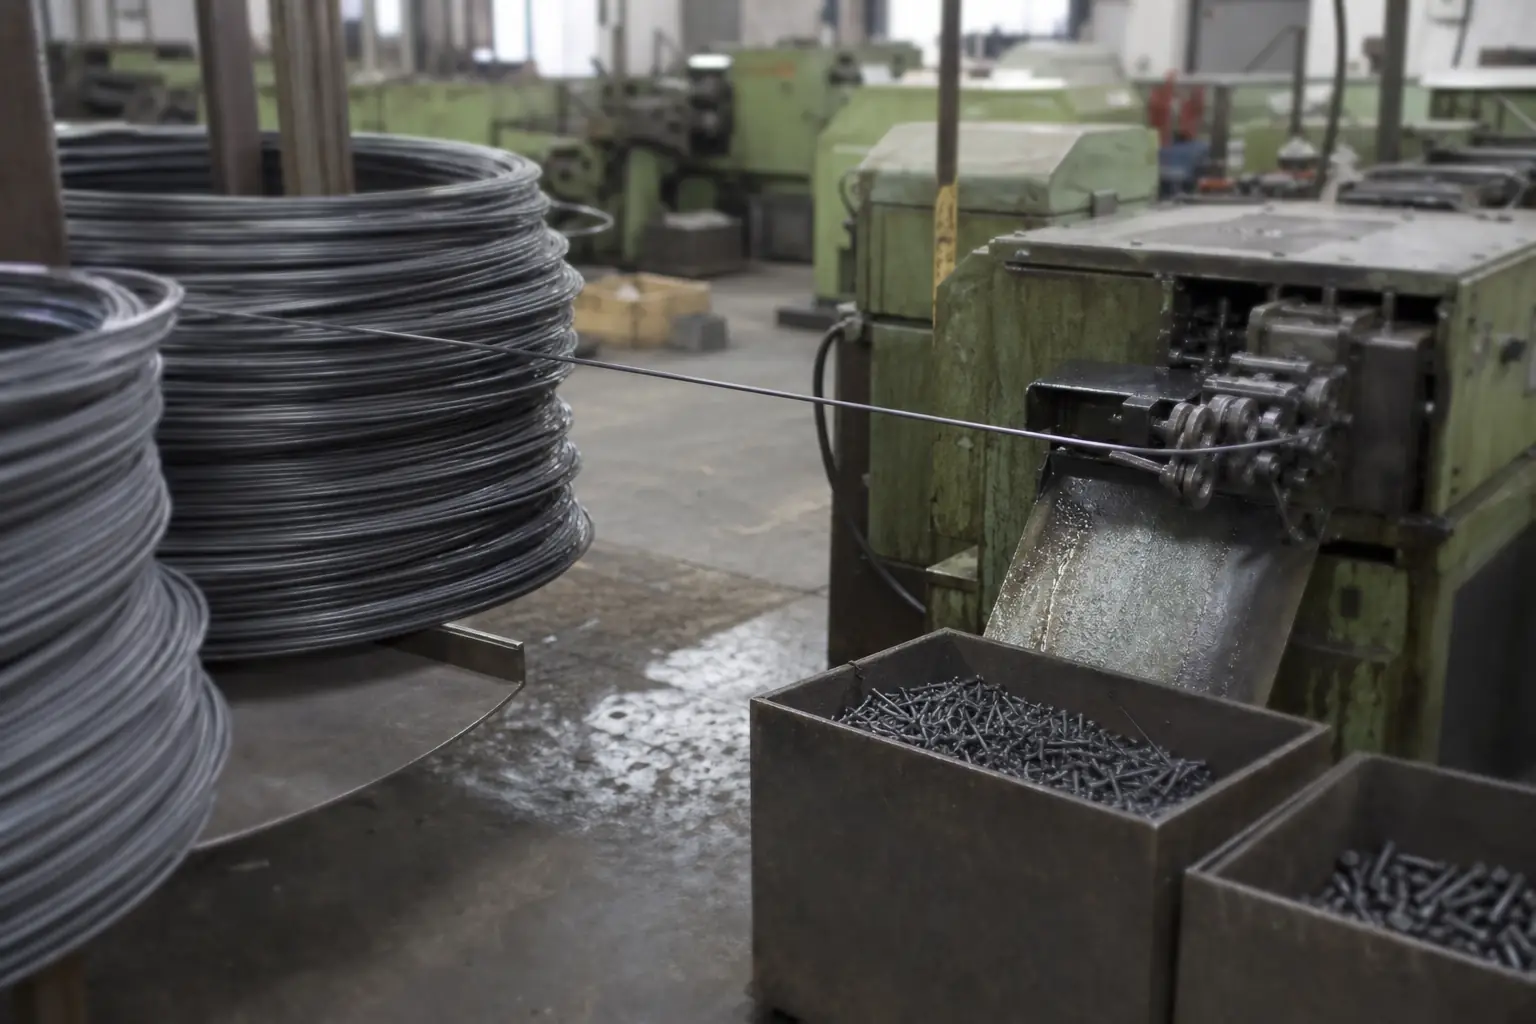
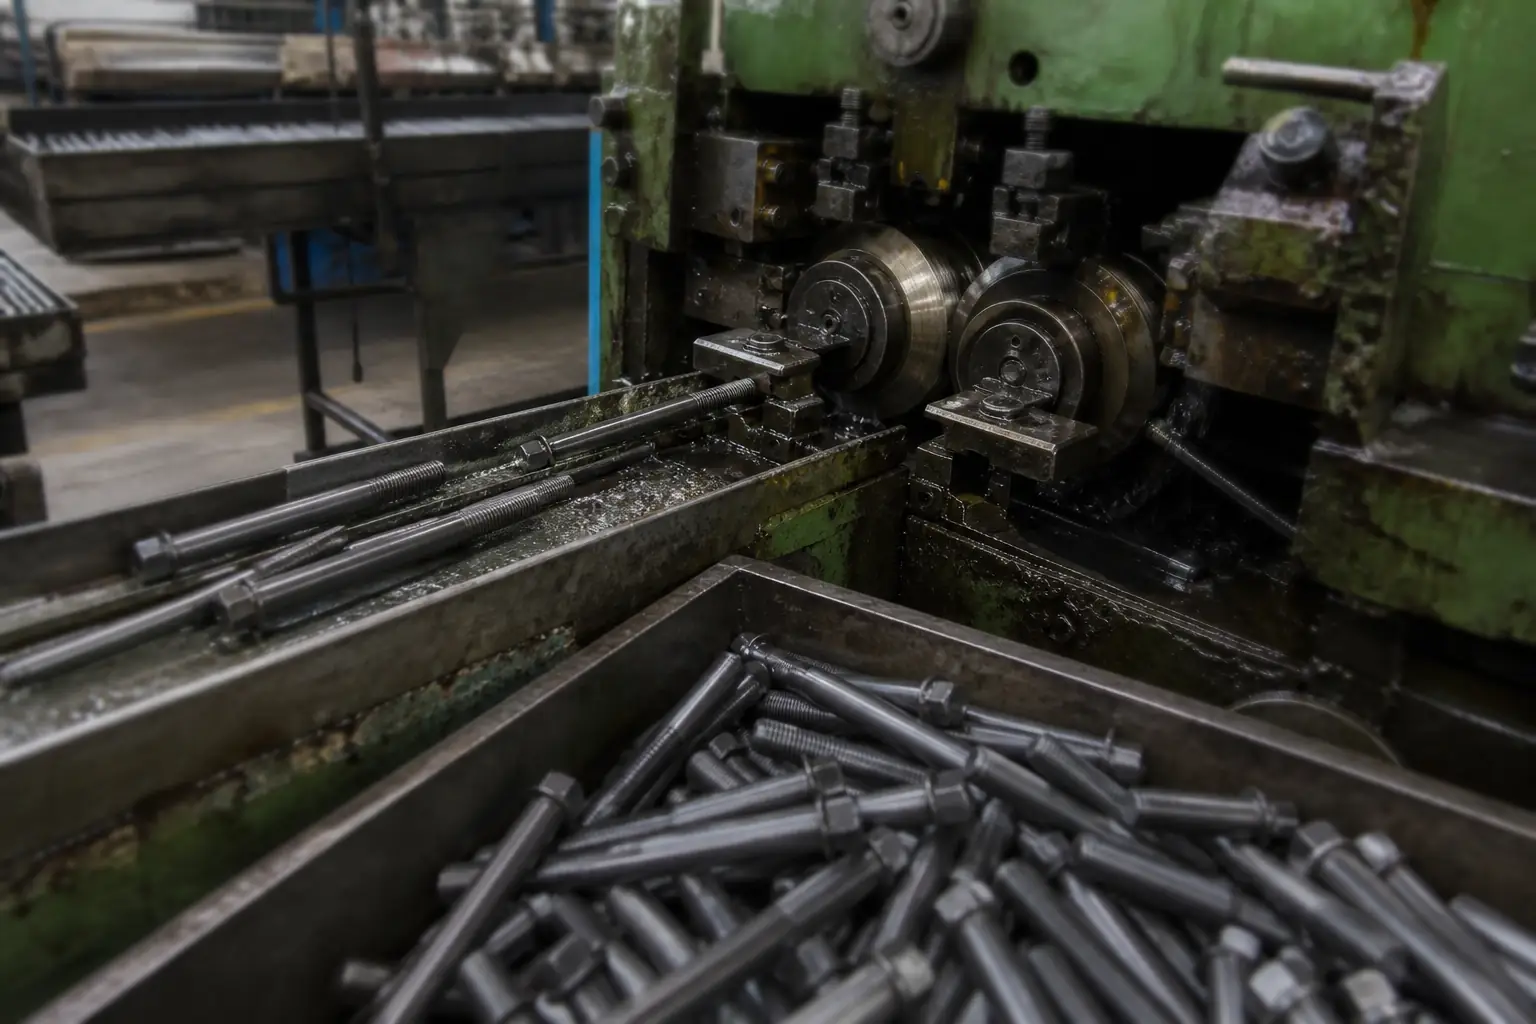
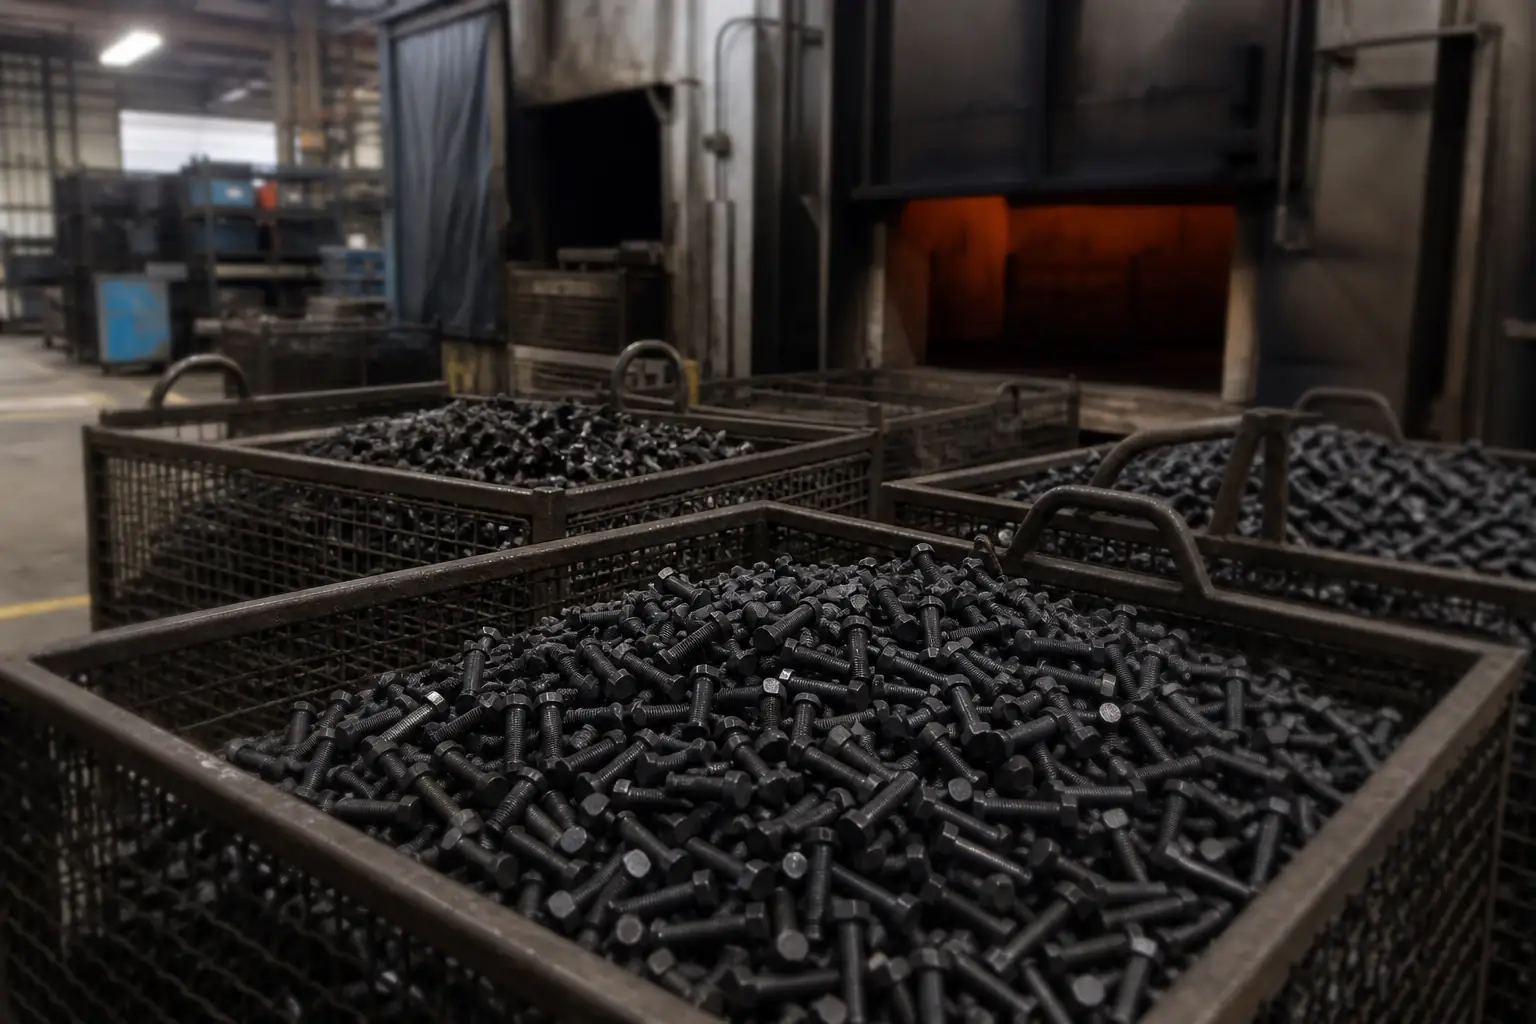
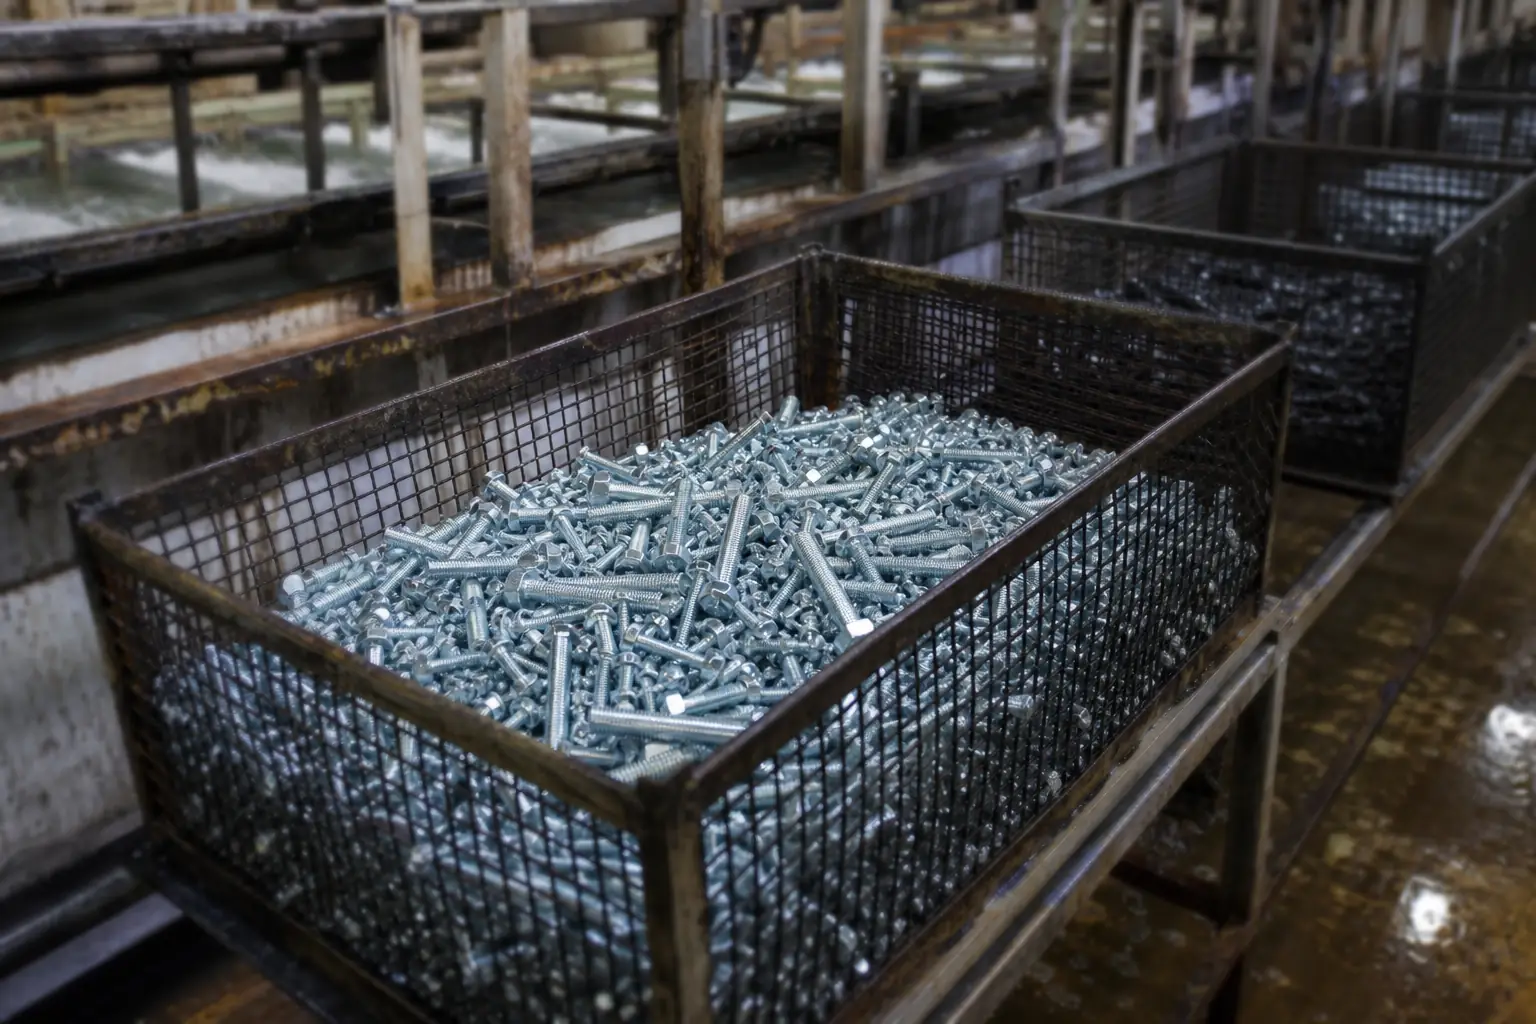
This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.
01
Cold heading
Wire rod is drawn to size and cold-formed into blanks. Forming rather than cutting keeps the grain flow continuous around the head, which is where a bolt is most likely to fail.
Head dimensions and under-head radius checked at set-up and per shift.
02
Thread rolling
Threads are rolled between hardened dies rather than cut. Rolled threads are stronger in fatigue than cut threads and hold pitch and flank angle far more consistently across a batch.
Go / no-go ring gauges to ISO 965 tolerance class 6g.
03
Heat treatment
Quench-and-temper brings carbon and alloy steel to the property class ordered — 8.8, 10.9 or 12.9 — with the furnace charge tracked so a finished lot can be traced back to it.
Core hardness and tensile tested per lot to ISO 898-1.
04
Surface treatment
Zinc, zinc-nickel, hot-dip galvanizing, black oxide, phosphate and Dacromet, selected against the service environment rather than against the price list.
Coating thickness and neutral salt spray hours to ISO 9227.
Frequently Asked Questions
What is the coarse-thread pitch of M3 for Heat-Set Threaded Inserts for Plastic?
For M3 the standard coarse pitch is 0.5 mm — this is the value used for Heat-Set Threaded Inserts for Plastic.
What clearance and tapping drill suit M3?
Use a 3.4 mm clearance hole (ISO 273 medium) for through-fixing, or a 2.5 mm tapping drill for a coarse M3 thread.
Is M3 Heat-Set Threaded Inserts for Plastic suitable for electronics and small mechanisms?
M3 Heat-Set Threaded Inserts for Plastic is in the micro range and is widely used in electronics, instrument enclosures and small precision mechanisms. Watch the over-torque margin — micro joints strip easily.
What's the typical proof load behavior of M3 class 8.8?
Micro-thread joints are sensitive to plastic deformation in the first turn under load — use a torque-limiting driver and check the bearing surface deformation on softer mating materials.
How do I request a quotation?
Use the technical drawing on this page to pick the exact configuration, then submit it with the quote form. We respond within one business day.
Need a fastener quote or a spec sheet?Message our engineers on WhatsApp — send a drawing or DIN number and get pricing back fast.Start WhatsApp Chat →
This website uses only necessary and functional cookies to operate, secure, and improve basic website performance.
We do not use advertising cookies, Google Analytics, or cross-site tracking technologies.
Privacy Policy