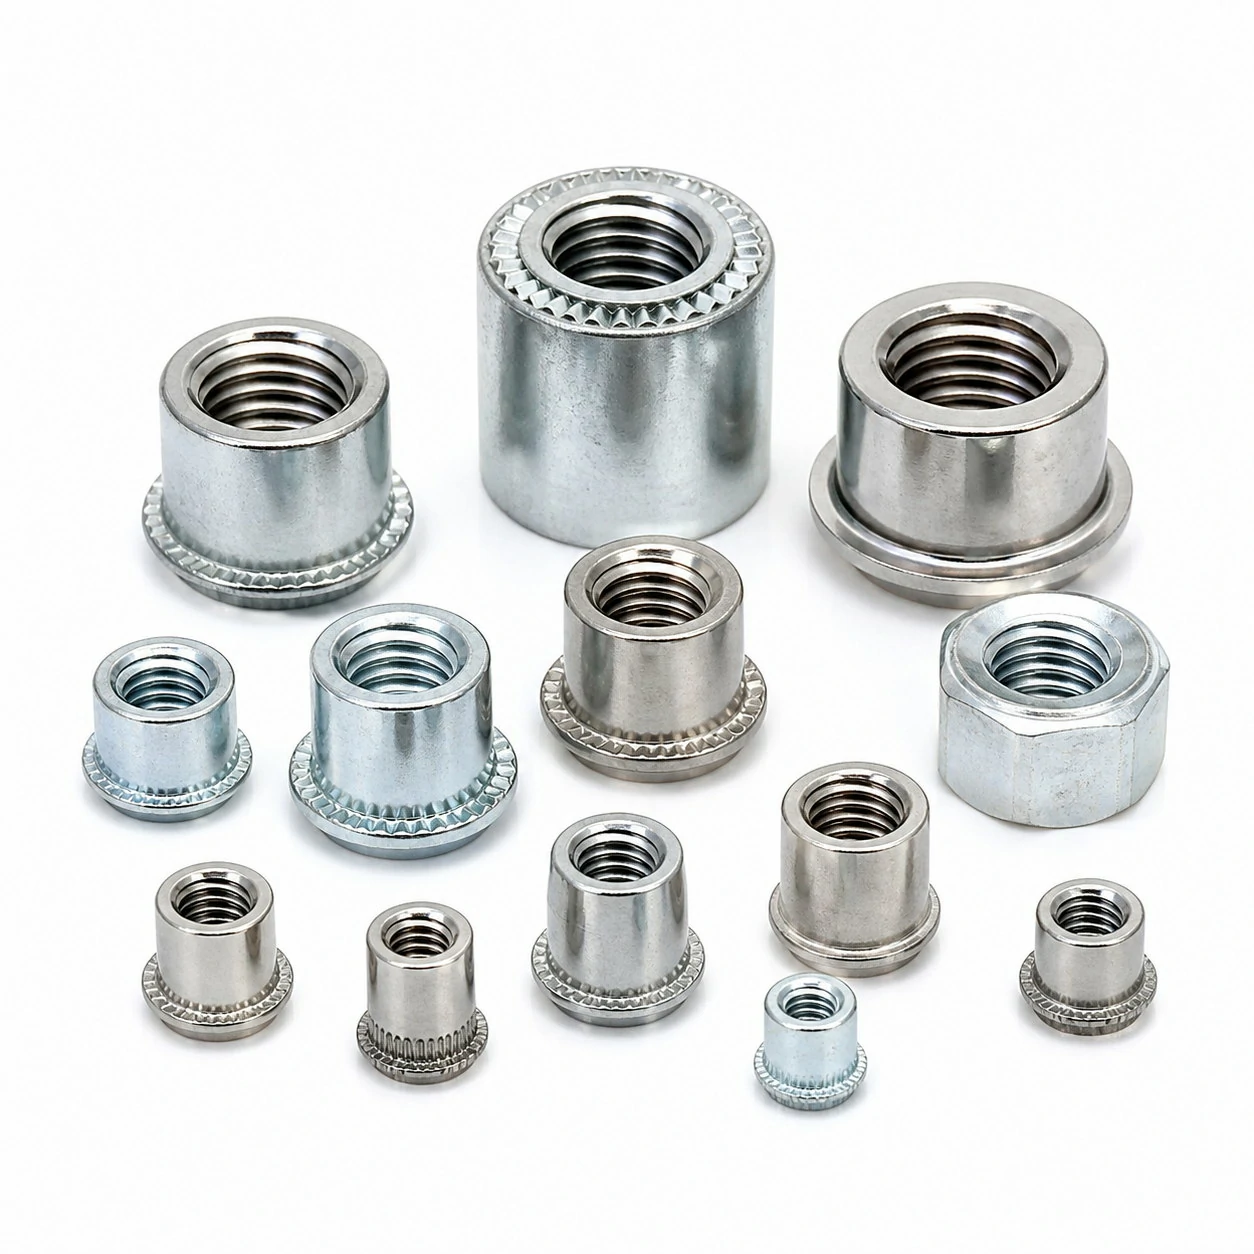
Nuts · Trade series (self-clinching, IFI-111 practice)
M4 Self-Clinching Press-Fit Nuts Dimensions
Controlling dimensions to Trade series (self-clinching, IFI-111 practice), with spanner or drive size and tightening torque.
M4 Self-Clinching Press-Fit Nuts dimensions to Trade series (self-clinching, IFI-111 practice): nut height 0.8 mm, coarse thread pitch 0.7 mm. Tighten to approximately 2.9 Nm at property class 8.8 in a dry, as-supplied condition.
Nut height
0.8 mm
Coarse thread pitch
0.7 mm
Tightening torque (class 8.8)
2.9 Nm
Figures are nominal values from the governing standard. Confirm against the tolerance class for your application before machining or ordering.
Hidden Deck Fasteners Sourcing: Manufacturing, Types & Material Compatibility
The M4 size of Self-Clinching Press-Fit Nuts is dimensioned by Trade series (self-clinching, IFI-111 practice). The table below gives the dimensional row from the standard, followed by the drive and the installation notes for this type.
Values are taken from the governing standard rather than from a general machine-thread table, because this type is not selected on one.
M4 Dimensional Row (Trade series (self-clinching, IFI-111 practice))
Thread size
Shank diameter (mm)
Length (mm)
Hole in sheet (mm)
Minimum sheet thickness (mm)
Maximum sheet hardness
Material
Installation
M4
5.40
3.80
5.42
0.8
HRB 80
Case-hardened steel
Press, squeeze
Spanner & Drive for M4 Self-Clinching Press-Fit Nuts
Drive geometry for M4 Self-Clinching Press-Fit Nuts is given by the row above; match the tool to the listed values.
Tightening Torque for M4
Class 8.8 (dry, ~µ 0.125)
≈ 2.9 Nm
Class 10.9 (dry, ~µ 0.125)
≈ 4.1 Nm
Class 12.9 (dry, ~µ 0.125)
≈ 4.9 Nm
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M4
Tensile stress area As (ISO 898-1)
8.78 mm²
Proof load, class 8.8
5.1 kN
Proof load, class 10.9
7.3 kN
Proof load, class 12.9
8.5 kN
Min. ultimate tensile, class 8.8
7 kN
Proof load = stress area × proof stress per ISO 898-1. Design joints so the working preload stays below the proof load of the selected class.
Installation Tips for M4 Self-Clinching Press-Fit Nuts
At M4 the joint is sensitive to over-torque — use a torque-limiting driver and check the head doesn't bury into a softer counterpart.
When to Step Up or Down from M4
When the joint preload approaches the proof load of M4 class 8.8, step up to M5 class 8.8 (or move to M4 class 10.9). When the joint is over-specified, M3 often saves weight and cost without losing the safety margin.
Technical Drawing
Customize the parameters below — every spec field is editable, and the drawing redraws to match the values you choose. Changing the size will snap the other fields to that size's standard values; you can then override any individual value.
Sends the selected values to the quote form below.
Request a Quote
The form below follows the current technical drawing configuration. Change the drawing values above and the request details update automatically.
Dimensions & Specifications (Trade series (self-clinching, IFI-111 practice))
Thread size
Shank diameter (mm)
Length (mm)
Hole in sheet (mm)
Minimum sheet thickness (mm)
Maximum sheet hardness
Material
Installation
M3
4.20
3.30
4.22
0.8
HRB 80
Case-hardened steel
Press, squeeze
M4
5.40
3.80
5.42
0.8
HRB 80
Case-hardened steel
Press, squeeze
M5
6.35
4.20
6.38
1.0
HRB 80
Case-hardened steel
Press, squeeze
M6
7.95
4.80
7.98
1.0
HRB 80
Case-hardened steel
Press, squeeze
M8
9.55
5.70
9.58
1.5
HRB 80
Case-hardened steel
Press, squeeze
Materials & Grades
Select a material class to see the grades we supply it in. Each designation is listed with its ISO/EN, AISI/SAE, JIS and GB equivalents.
Sheet metal fabricationThreads in enclosure and chassis panels on the press line.
Electronics enclosuresCaptive threads for lids, brackets and PCB mounts.
Automotive & transportVibration-prone joints where the locking type is specified on the drawing.
Maintenance & MROReplacements matched to the existing bolt class, thread and finish.
Building servicesThreaded rod, channel and suspension assemblies.
Typical applications
limited by sheet HARDNESS, not sheet thickness
a permanent torque-resistant thread in sheet too thin to tap
installed by press, never by hammer
joints re-torqued at a service interval
completing a bolted joint on a stud, rod or bolt
locking an adjustment so it cannot drift
Service conditions to specify against
Marine and coastal
Available in A4 (316) stainless for chloride exposure — coastal structures, pool halls, water treatment and deck hardware, where A2 will eventually pit.
High load
Supplied in ISO 898-1 property classes, so the joint can be designed to a stated proof load and tightened to a calculated torque rather than by feel.
Match the class
A nut below the bolt property class strips before the bolt reaches its own limit — pair class 8 nuts with 8.8 bolts, class 10 with 10.9.
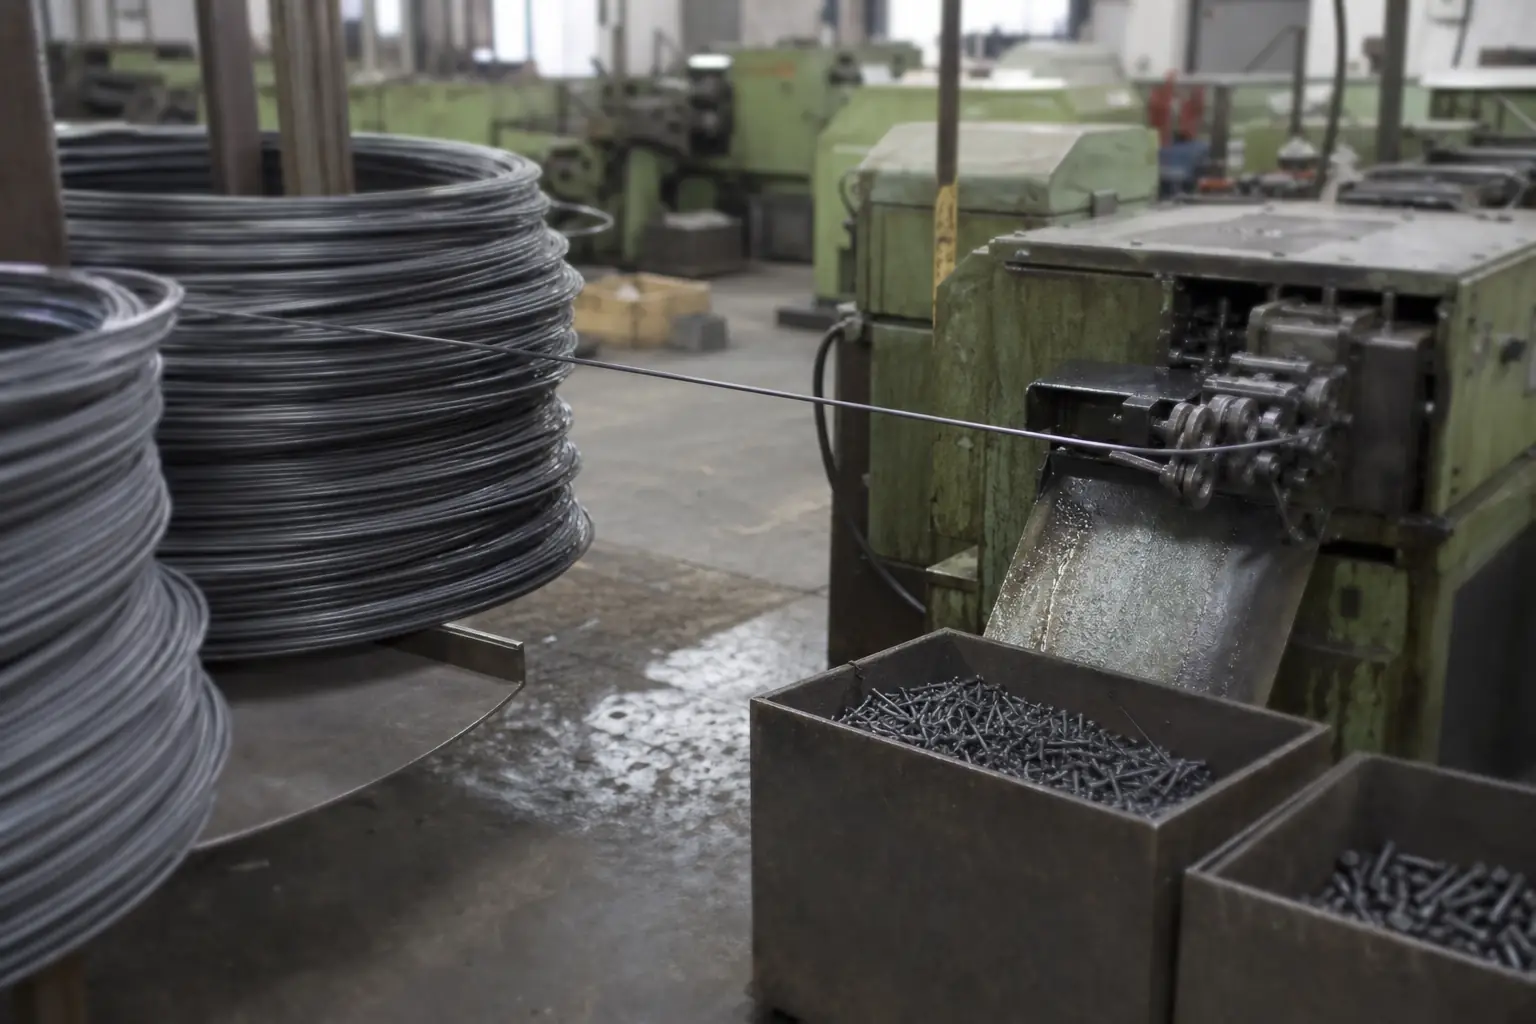
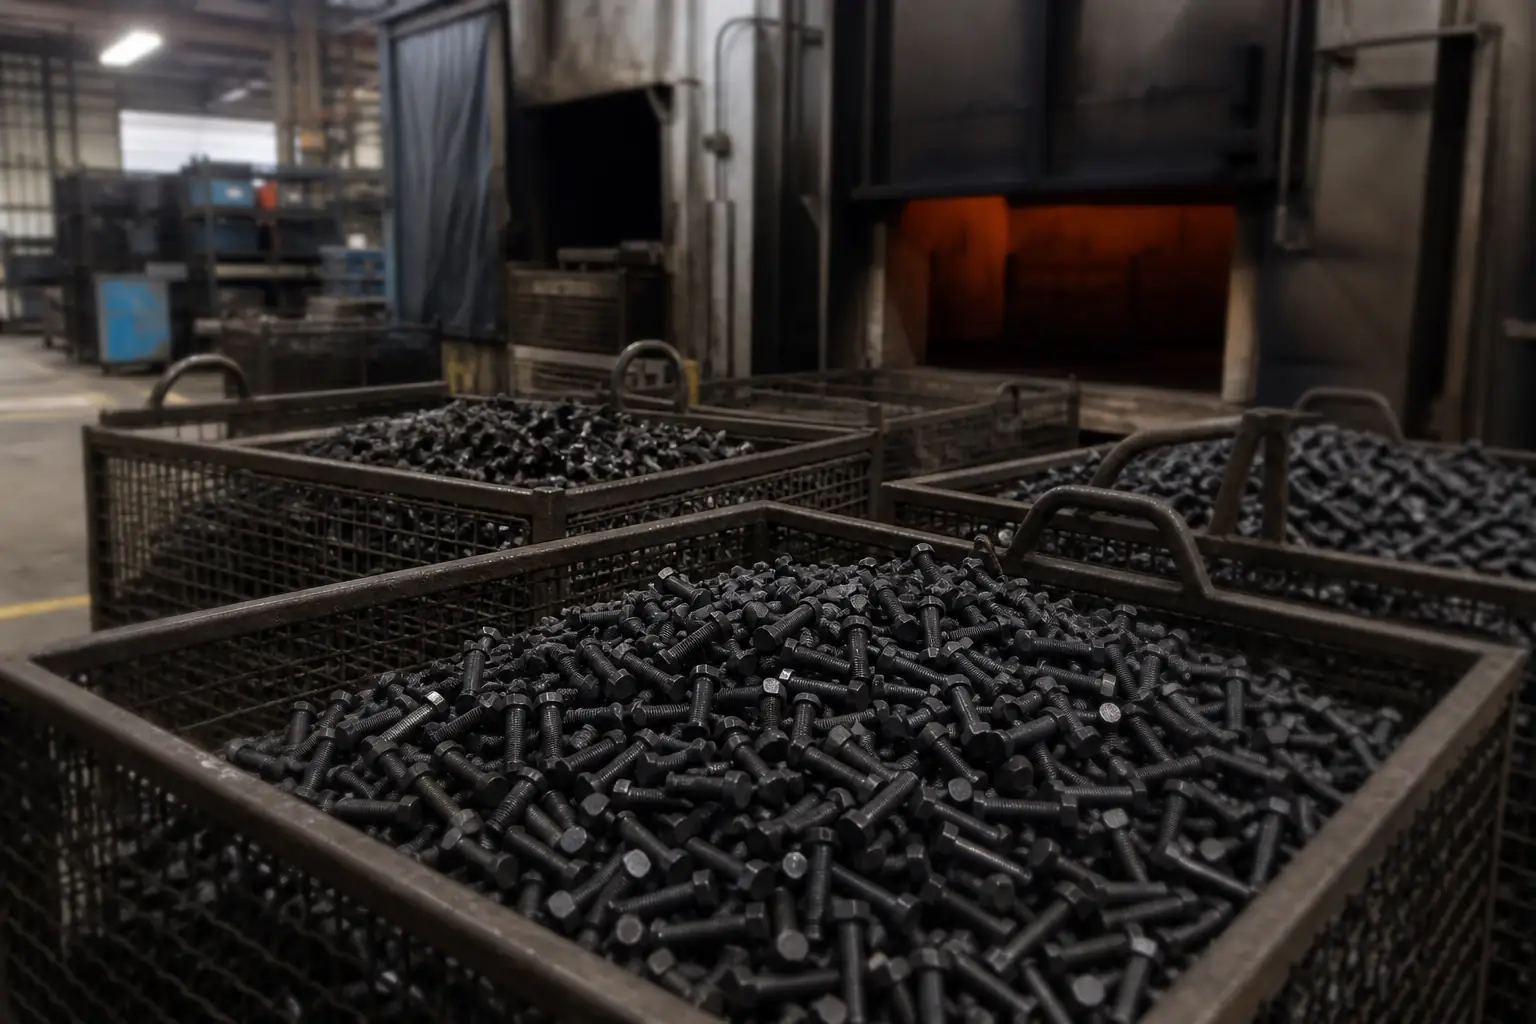
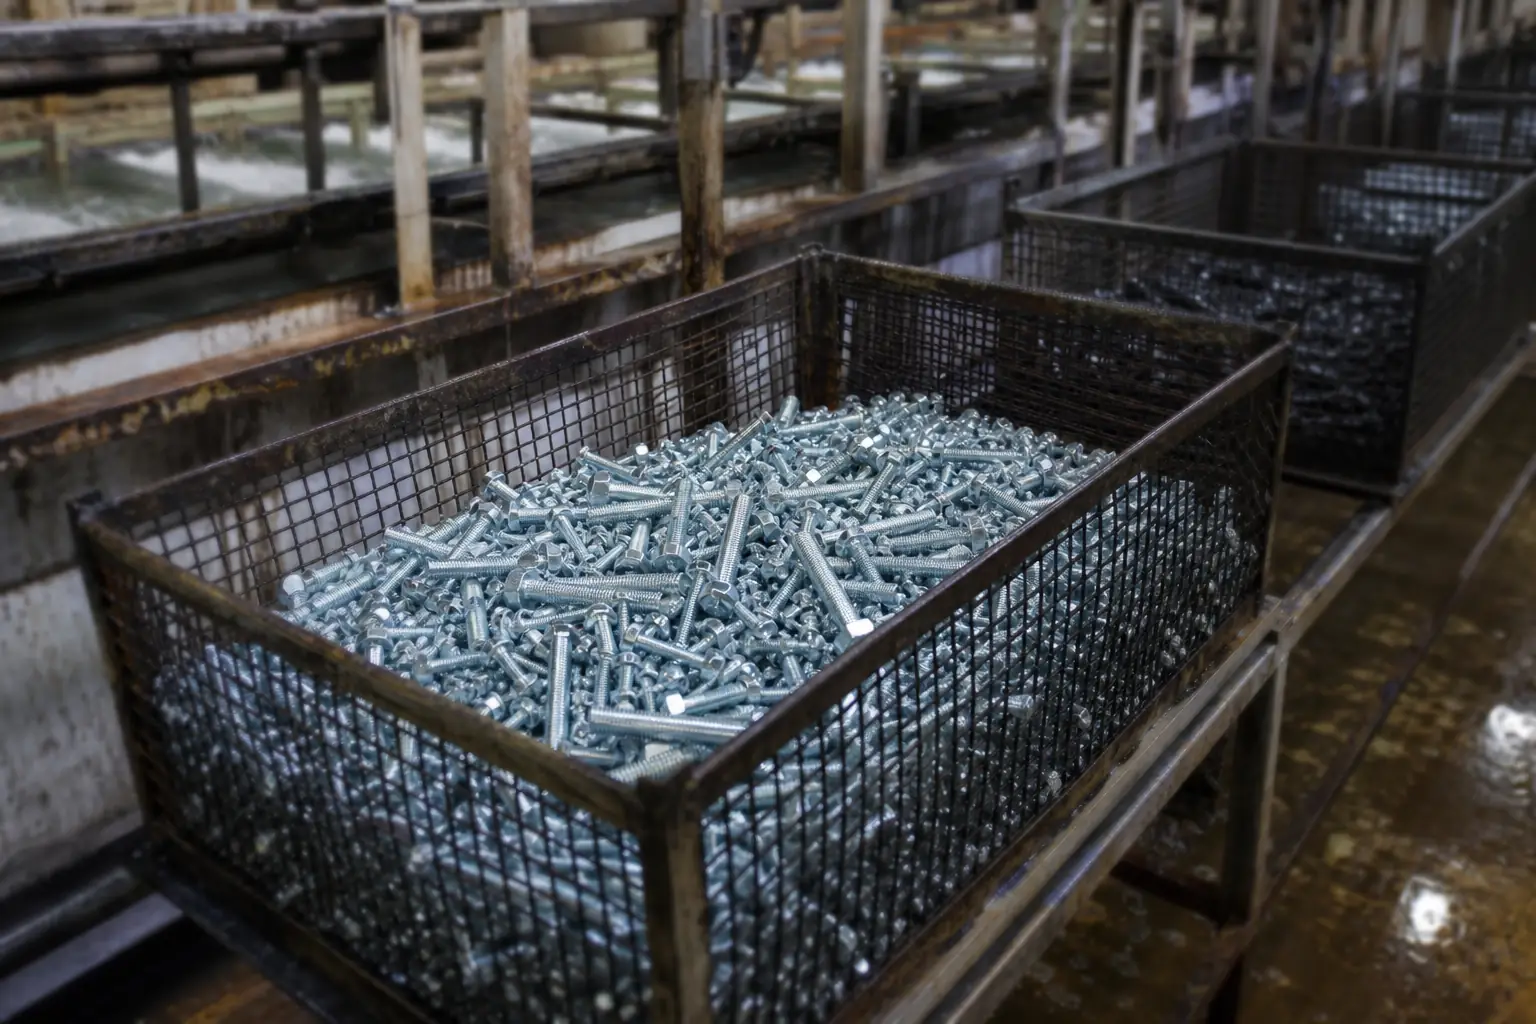
This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.
01
Cold heading
Wire rod is drawn to size and cold-formed into blanks. Forming rather than cutting keeps the grain flow continuous around the head, which is where a bolt is most likely to fail.
Head dimensions and under-head radius checked at set-up and per shift.
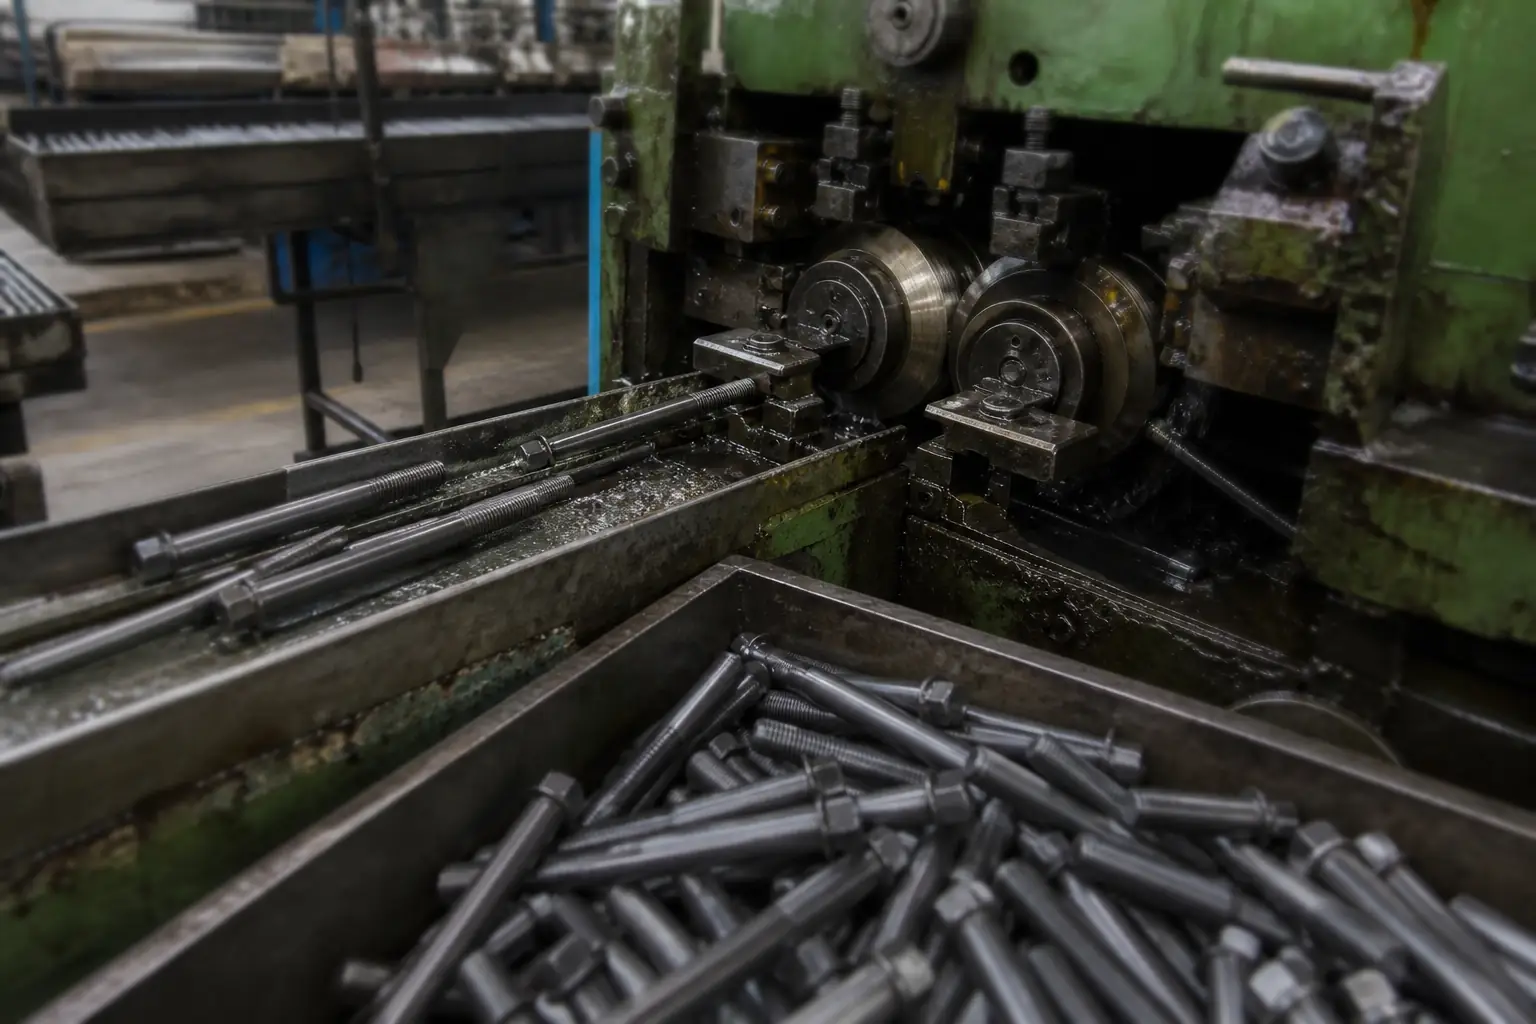
02
Thread rolling
Threads are rolled between hardened dies rather than cut. Rolled threads are stronger in fatigue than cut threads and hold pitch and flank angle far more consistently across a batch.
Go / no-go ring gauges to ISO 965 tolerance class 6g.
03
Heat treatment
Quench-and-temper brings carbon and alloy steel to the property class ordered — 8.8, 10.9 or 12.9 — with the furnace charge tracked so a finished lot can be traced back to it.
Core hardness and tensile tested per lot to ISO 898-1.
04
Surface treatment
Zinc, zinc-nickel, hot-dip galvanizing, black oxide, phosphate and Dacromet, selected against the service environment rather than against the price list.
Coating thickness and neutral salt spray hours to ISO 9227.
Frequently Asked Questions
What clearance and tapping drill suit M4?
Use a 4.5 mm clearance hole (ISO 273 medium) for through-fixing, or a 3.3 mm tapping drill for a coarse M4 thread.
Is M4 Self-Clinching Press-Fit Nuts suitable for electronics and small mechanisms?
M4 Self-Clinching Press-Fit Nuts is in the micro range and is widely used in electronics, instrument enclosures and small precision mechanisms. Watch the over-torque margin — micro joints strip easily.
What's the typical proof load behavior of M4 class 8.8?
Micro-thread joints are sensitive to plastic deformation in the first turn under load — use a torque-limiting driver and check the bearing surface deformation on softer mating materials.
What is the height of an M4 nut?
The nominal height of a style-1 ISO 4032 M4 nut is in the spec table on this page. Style-2 (thick) is approximately 1.1× this height; thin (ISO 4035 / DIN 439) is approximately 0.5×.
How do I request a quotation?
Use the technical drawing on this page to pick the exact configuration, then submit it with the quote form. We respond within one business day.
This website uses only necessary and functional cookies to operate, secure, and improve basic website performance.
We do not use advertising cookies, Google Analytics, or cross-site tracking technologies.
Privacy Policy