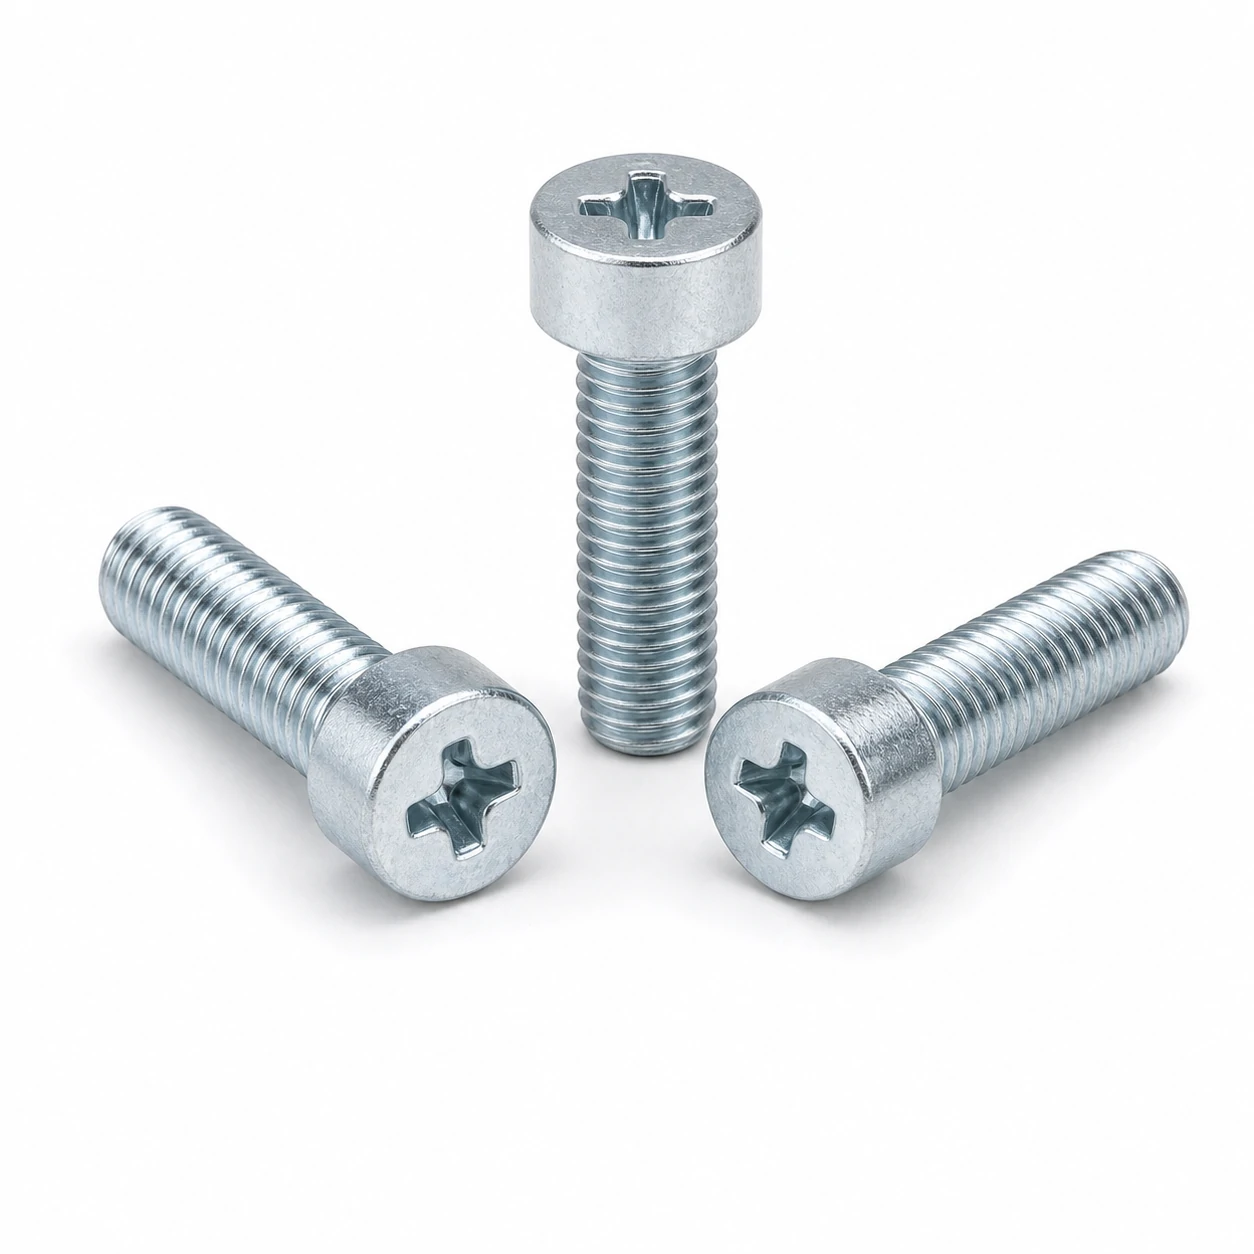
M6 Cheese Head Screws dimensions to ISO 7048 / DIN 7985: head diameter 10 mm, head height 6 mm, coarse thread pitch 1 mm, clearance hole (ISO 273 medium) 6.6 mm. Tighten to approximately 10 Nm at property class 8.8 in a dry, as-supplied condition.
- Head diameter
- 10 mm
- Head height
- 6 mm
- Coarse thread pitch
- 1 mm
- Clearance hole (ISO 273 medium)
- 6.6 mm
- Tightening torque (class 8.8)
- 10 Nm
Figures are nominal values from the governing standard. Confirm against the tolerance class for your application before machining or ordering.
M6 Cheese Head Screws (ISO 7048 / DIN 7985) are specified by thread size, length and head dimensions. The M6 row from the standard is reproduced below, followed by the drill sizes, spanner size and torque values used when installing this size.
M6 Dimensional Row (ISO 7048 / DIN 7985)
| Size | Pitch (mm) | Head diameter dk (mm) | Head height k (mm) | Cross recess | Reference standard |
|---|
| M6 | 1.0 | 10.0 | 6.0 | PH3 | ISO 7048 / DIN 7985 (cross) / ISO 1207 (slotted) |
Spanner & Drive for M6 Cheese Head Screws
M6 Cheese Head Screws use a PH3 cross recess. Match the driver bit to the recess (Phillips PH / Pozi PZ are NOT interchangeable).
Hole Sizes for M6
| Coarse-thread pitch (ISO 724) | 1 mm |
|---|
| Through-hole / clearance (ISO 273 medium) | 6.6 mm |
|---|
| Tapping drill, coarse thread | 5 mm |
|---|
Tightening Torque for M6
| Class 8.8 (dry, ~µ 0.125) | ≈ 10 Nm |
|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 15 Nm |
|---|
| Class 12.9 (dry, ~µ 0.125) | ≈ 17 Nm |
|---|
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M6
| Tensile stress area As (ISO 724) | 20.1 mm² |
|---|
| Proof load, class 8.8 | 12 kN |
|---|
| Proof load, class 10.9 | 17 kN |
|---|
| Proof load, class 12.9 | 20 kN |
|---|
| Min. ultimate tensile load, class 8.8 | 16 kN |
|---|
Proof load = tensile stress area × the proof stress Sp of the class, per ISO 898-1 — Sp is a lower figure than the yield stress Rp0.2 and the two are not interchangeable. The stress area is computed from this size's own diameter and pitch, so a fine-pitch designation gives the fine-pitch figure. Design the joint so the working preload stays below the proof load of the class selected.
Mating Parts for M6
For M6, pair with a M6 hex nut (ISO 4032 / DIN 934) and, where used, a M6 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
When to Step Up or Down from M6
When the joint preload approaches the proof load of M6 class 8.8, step up to M8 class 8.8 (or move to M6 class 10.9). When the joint is over-specified, M5 often saves weight and cost without losing the safety margin.
Custom manufacturing · Made to drawing
Need cheese head screws in a size this table does not list?
This page covers M6 cheese head screws. Lengths and thread lengths outside the standard table are the commonest request, followed by a drive the standard does not offer and a head marked with your own part number. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.
Custom screw manufacturingSend a drawing
Applications & Industries for M6 Cheese Head Screws
What Cheese Head Screws are specified for, industry by industry. Stocked from M1.6 to M10.
Industries that specify Cheese Head Screws
-
Steel fabrication
Bolted connections in frames, enclosures, walkways and weldments, on the bench and on site.
-
Energy & infrastructure
Tower, pipework, switchgear and plant fixings specified for long service life and inspectable joints.
-
Maintenance & MRO
Stocked replacements matched to an existing property class, thread and finish.
-
Food, pharma & cleanroom
Stainless assemblies that are washed down, where the finish matters as much as the strength.
-
Machine building & OEM
The default fastener on production equipment: covers, brackets, motor mounts and sub-assemblies tightened to a specified torque.
-
Automotive & transport
Chassis, driveline and body fixings that see vibration and are assembled to a controlled preload.
Typical applications
- assemblies that are dismantled for service and re-torqued
- joints where the property class is stated on the drawing
- clamping two machined faces to a calculated preload
- bolting brackets, motors and gearboxes to a frame
Service conditions to specify against
- Marine and coastal
- Available in A4 (316) stainless for chloride exposure — coastal structures, pool halls, water treatment and deck hardware, where A2 will eventually pit.
- High load
- Supplied in ISO 898-1 property classes, so the joint can be designed to a stated proof load and tightened to a calculated torque rather than by feel.
- Torque and preload
- The joint is designed around bolt tension, so lubrication, coating and the friction coefficient all change the torque figure — state them together.
Where to use something else
- Do not use a machine thread into unthreaded sheet or timber; use a tapping screw, rivet nut or insert made for that parent material.
Full application guide: where Cheese Head Screws are used, how to specify them, and the cases they are wrong for