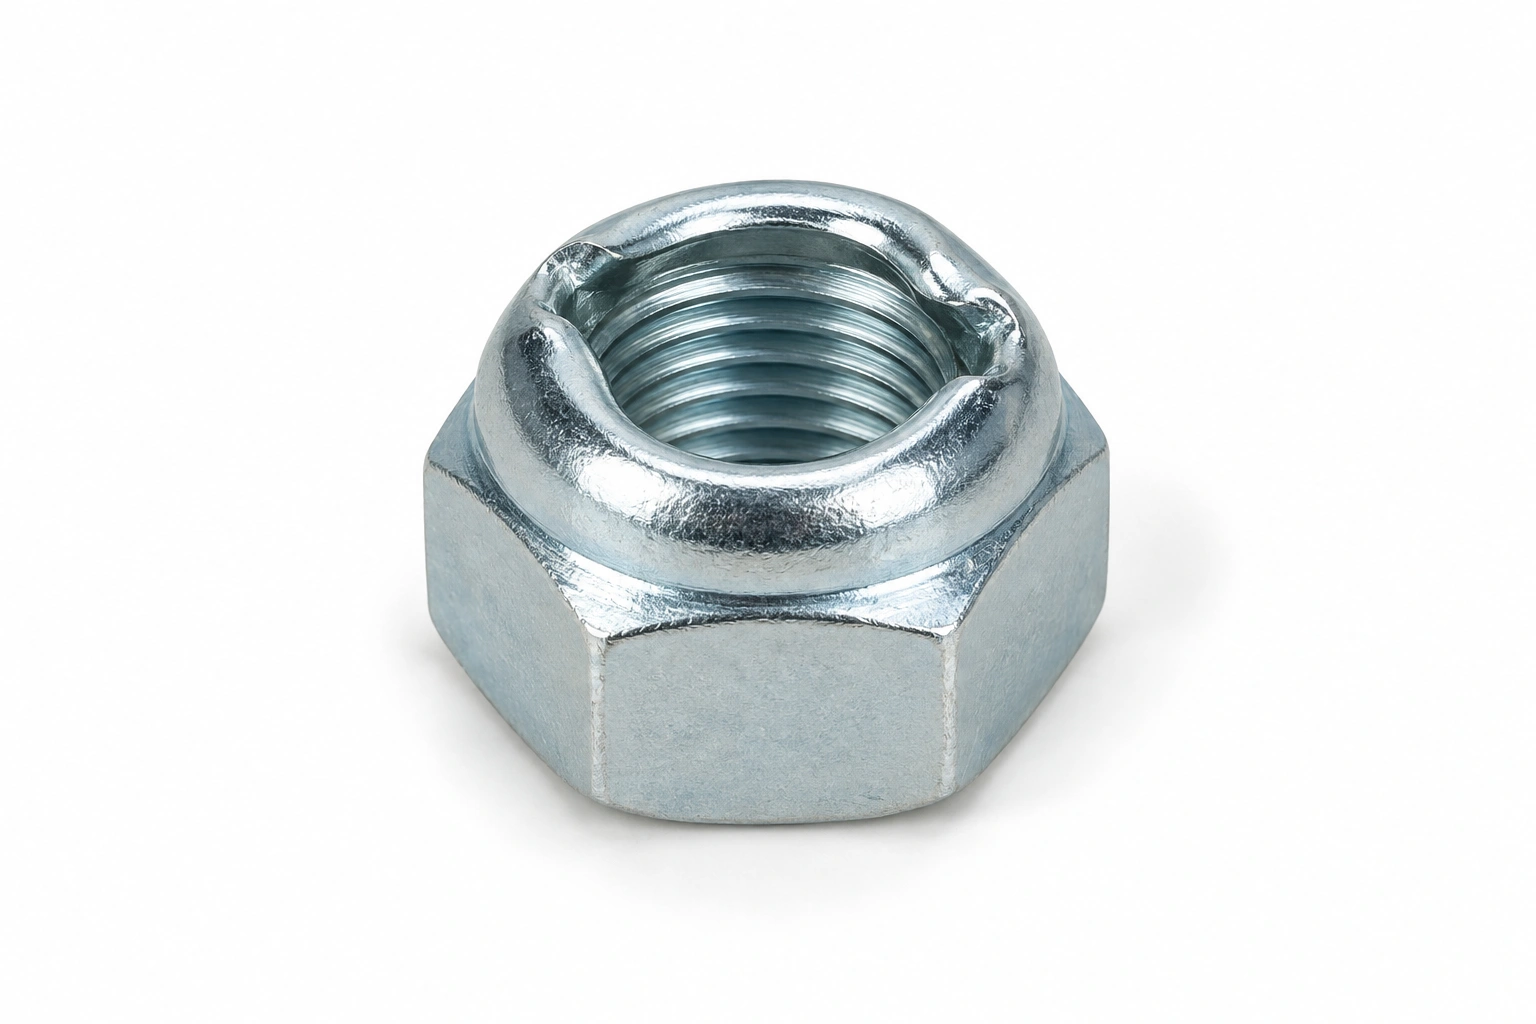
Dimensional data for M8X1 Fine-Thread All-Metal Hex Lock Nuts to ISO 10513, with the drive and the installation notes for this type.
Values are taken from the governing standard rather than from a general machine-thread table, because this type is not selected on one.
M8X1 Dimensional Row (ISO 10513)
| Size | Pitch P (mm) | d_a_max (mm) | d_a_min (mm) | d_w_min (mm) | Width across corners e (mm) | h_max (mm) | h_min (mm) | m_w_min (mm) | Width across flats s (mm) | s_min (mm) | Reference standard |
|---|---|---|---|---|---|---|---|---|---|---|---|
| M8x1 | 1 | 8.75 | 8 | 11.63 | 14.38 | 8 | 7.14 | 5.15 | 13 | 12.73 | ISO 10513 |
Spanner & Drive for M8X1 Fine-Thread All-Metal Hex Lock Nuts
Drive geometry for M8X1 Fine-Thread All-Metal Hex Lock Nuts is given by the row above; match the tool to the listed values.
Tightening Torque for M8X1
| Class 8.8 (dry, ~µ 0.125) | ≈ 26 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 38 Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 45 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M8X1
Nuts are graded to ISO 898-2 by the proof load the nut itself will hold (classes 04, 05, 5, 6, 8, 10 and 12), not by the 8.8 / 10.9 / 12.9 scale used for bolts. A class-8 nut is the correct mate for a class-8.8 bolt, and the joint is designed on the bolt, so no bolt-tension figure is quoted here.
Installation Tips for M8X1 Fine-Thread All-Metal Hex Lock Nuts
- At M8X1 the stretch in the bolt becomes the controlling factor — for critical joints, use angle-controlled or stretch-controlled tightening instead of pure torque.
Mating Parts for M8X1
Pair M8X1 with the matching M8X1 bolt or screw, plus a M8X1 flat washer where required to distribute load on softer materials.
Custom manufacturing · Made to drawing
Need fine-thread all-metal hex lock nuts in a size this table does not list?
This page covers M8X1 fine-thread all-metal hex lock nuts. Height and across-flats are the two most often changed — a thinner nut for clearance, a larger hex for a tool that is already on the line. Made by cold heading or tapping.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.