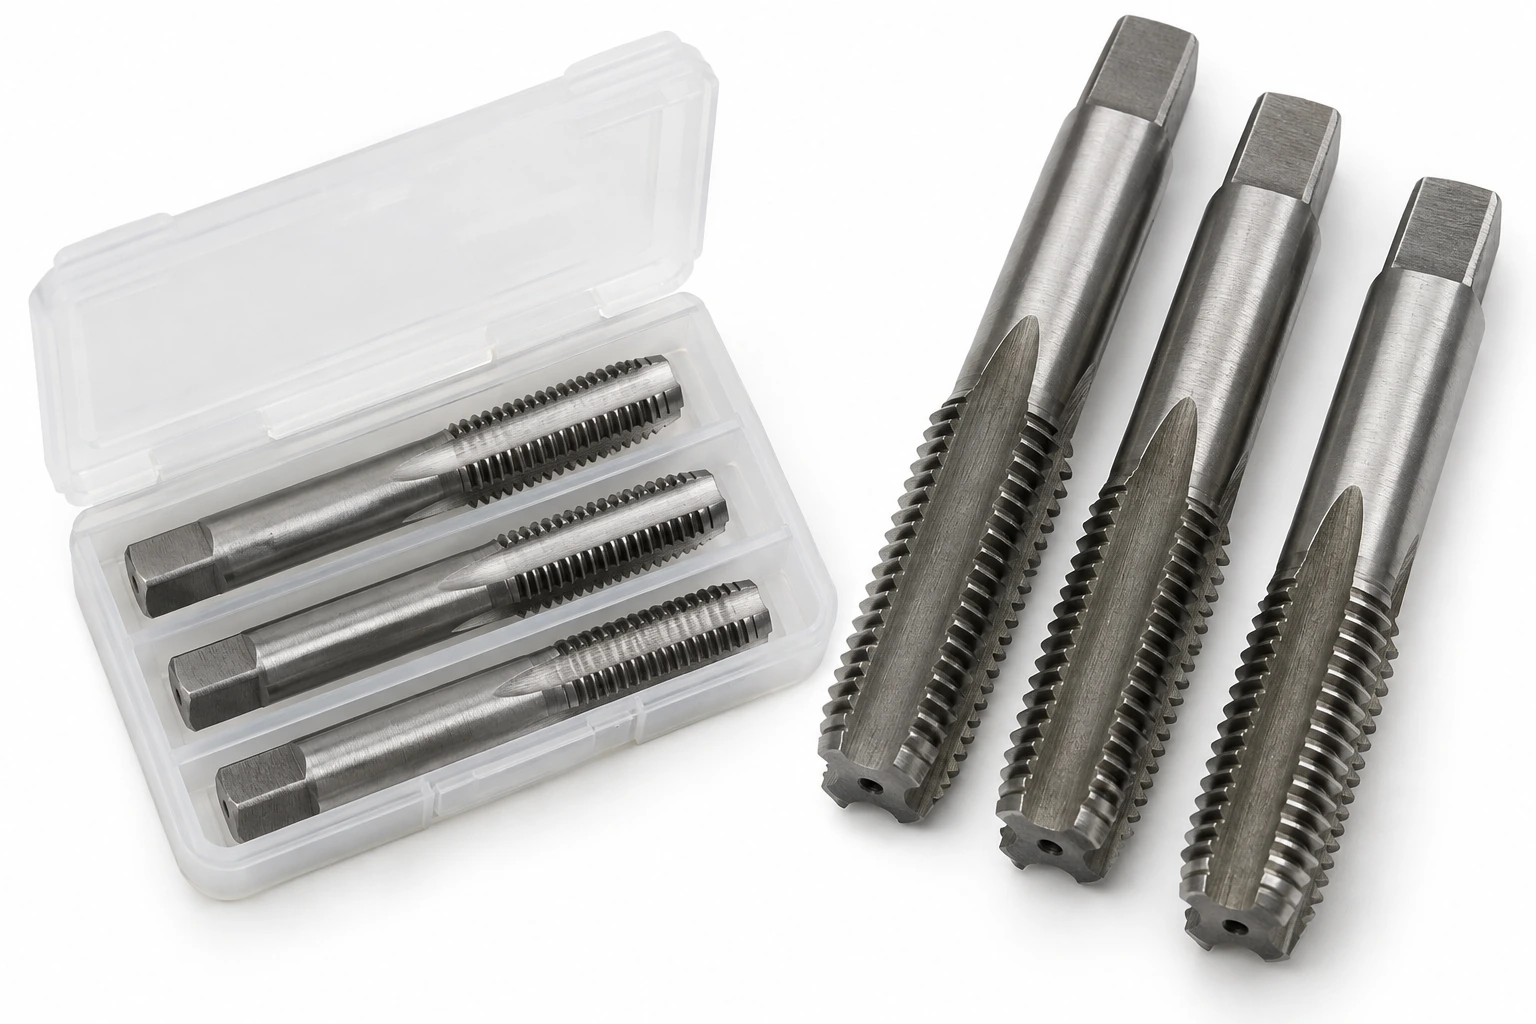
Specification summary of DIN 352 as applied to hand tap sets (taper, second and plug): the dimensions the standard fixes, the full size range supplied, and the related designations commonly cross-referenced.
DIN 352 — Scope
DIN 352 specifies the dimensional requirements for hand tap sets (taper, second and plug).
Material, surface condition and any performance rating are set by separate documents specific to this part family — ISO 898-1 and ISO 898-2, which govern bolt and nut property classes, do not apply here.
Tolerance & Product Grades
Tolerances for hand tap sets (taper, second and plug) are given as limits on the individual dimensions in the table rather than as a fastener product grade.
Where a general-tolerance class is cited on the drawing instead, it applies to the dimensions not otherwise toleranced.
Dimensions Specified by DIN 352
| Tap | Lead (chamfered threads) | Job in the sequence | Blind hole |
|---|---|---|---|
| taper (first) | about 8 u2013 10 threads | starts the thread square to the face | cannot reach the bottom |
| second (intermediate) | about 3 u2013 5 threads | cuts the working length of thread | cannot reach the bottom |
| plug (bottoming) | about 1 u2013 2 threads | finishes the thread to the hole bottom | this is the one that reaches |
Equivalent Standards
Where direct equivalents exist (ISO ↔ DIN, ISO ↔ ASME), they are listed on the parent Hand Tap Sets (Taper, Second and Plug) page.
Always confirm against the dimensions on this page, since some "equivalent" standards differ in tolerances and head geometry.
Companion Standards
DIN 352 controls only the geometry of hand tap sets (taper, second and plug). Surface finish is governed by separate finish standards (for example ISO 4042 for electroplating), and corrosion testing by ISO 9227 (neutral salt spray). Mechanical performance is set by the standards specific to this part family, not by ISO 898-1 or ISO 898-2, which apply to bolts, screws and nuts.