Skip to content
Pipe & Pneumatic Fittings · DIN 71412 / ISO 6392 (lubricating nipples) · Application guide

What Are Grease Nipples (DIN 71412) Used For?

Typical applications, the industries that specify grease nipples (din 71412), and how to choose the right size, material and finish for the joint.

Grease Nipples (DIN 71412) are used for joining and sealing fluid or pneumatic lines. They are manufactured to DIN 71412 / ISO 6392 (lubricating nipples), and selection is driven by the screw size, the fit and tolerance the assembly requires, and the service environment.

Primary duty
Joining and sealing fluid or pneumatic lines
Governing standard
DIN 71412 / ISO 6392 (lubricating nipples)
Screw size range
1/4-28 UNF to M10 x 1.0
Category
Pipe & Pneumatic Fittings

Application notes are general engineering guidance. Verify the property class and any approval requirement against your own design calculation.

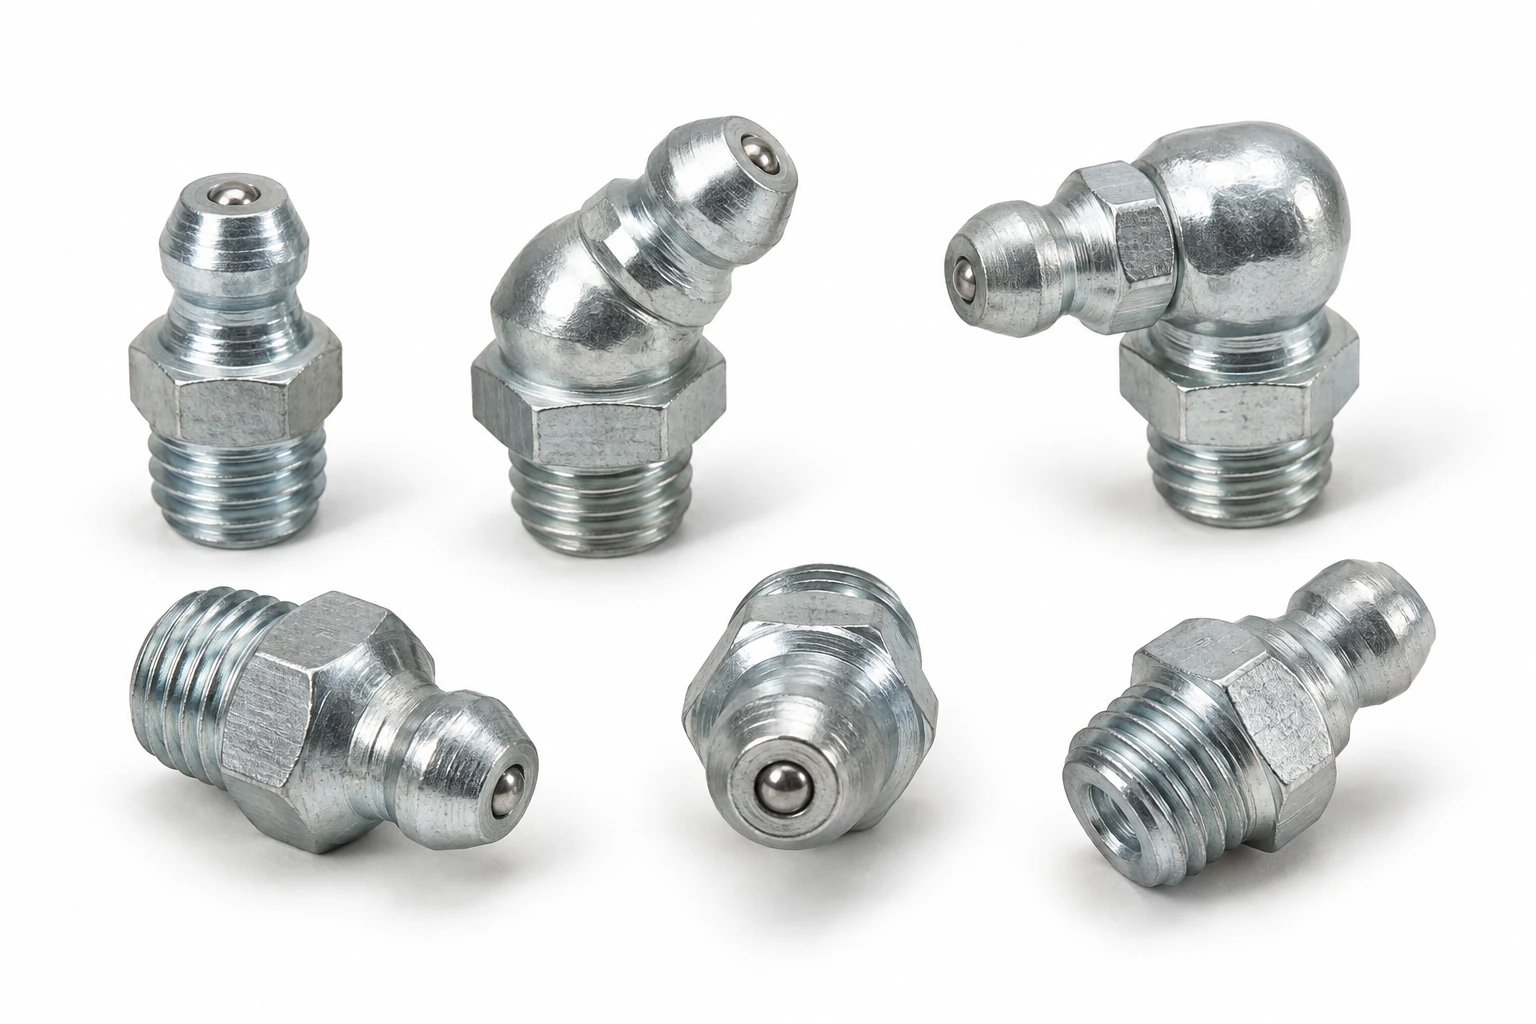
What Are Grease Nipples (DIN 71412) Used For? application image

Grease Nipples (DIN 71412) are selected when an assembly calls for joining and sealing fluid or pneumatic lines. This application guide to the DIN 71412 / ISO 6392 (lubricating nipples) type covers concrete end-uses, the specification checklist, correct installation, and where an alternative fastener performs better. Stocked across roughly 1 to 10, they cover general to heavy-duty work.

Typical Applications for Grease Nipples (DIN 71412)

The most common settings where these are specified:

  • General machine building: fastening covers, brackets, motors and sub-assemblies on production equipment.
  • Maintenance & repair (MRO): a stocked size for servicing existing plant where the original fastener spec must be matched.
  • Fabrication & metalwork: bench and on-site assembly of steel frames, enclosures and weldments.
  • Pneumatic systems: connecting air lines, cylinders and valves on automation rigs.
  • Hydraulic & fluid power: sealed, pressure-rated joints in fluid lines.

How to Specify Grease Nipples (DIN 71412) for Your Application

  • Size: Match the nominal size to the mating thread or hole. This product spans 1–10; check the full table below for the exact dimensions of each size.
  • Thread & pressure: Match the thread form (BSP/NPT/metric) and pressure rating to the line, and seal appropriately (tape, sealant or O-ring).
  • Environment: For damp, coastal or chemical exposure prefer A4/316 stainless or a suitable coating; indoors, plated steel or A2 is usually sufficient.
  • Standard: This product is supplied to DIN 71412 / ISO 6392 (lubricating nipples). Quoting the standard on your order guarantees interchangeable dimensions between suppliers.

Installation & Assembly Practice

  • Seal tapered threads with PTFE tape or anaerobic sealant applied clear of the first thread; parallel threads seal on a washer or O-ring, not on the thread.
  • Tighten to the fitting manufacturer's torque — over-tightening tapered threads splits female ports.

Common Selection Mistakes with Grease Nipples (DIN 71412)

  • Mating BSP and NPT threads directly — the 55°/60° forms do not seal against each other.
  • Exceeding the pressure rating of the lowest-rated component in the line.

Where Grease Nipples (DIN 71412) Are Not the Right Choice

Do not mix thread forms (BSP into NPT) without an adapter, and do not exceed the pressure rating of the lowest-rated component.
Technical Drawing

Customize the parameters below — every spec field is editable, and the drawing redraws to match the values you choose. Changing the size will snap the other fields to that size's standard values; you can then override any individual value.

Sends the selected values to the quote form below.

Request a Quote

The form below follows the current technical drawing configuration. Change the drawing values above and the request details update automatically.

Request a Quotation

Specification
Business Information

Dimensions & Specifications (DIN 71412 / ISO 6392 (lubricating nipples))

ThreadHead angleFormNotes
M6 x 1.0straight (form A)DIN 71412 Acommonest small nipple
M8 x 1.0straight (form A)DIN 71412 Ageneral machinery
M8 x 1.25straight (form A)DIN 71412 Ageneral machinery
M10 x 1.0straight (form A)DIN 71412 Ageneral machinery
M10 x 1.045 degrees (form B)DIN 71412 Bwhere a straight gun will not reach
M10 x 1.090 degrees (form C)DIN 71412 Ctight or shrouded positions
R 1/8 instraight (form A)DIN 71412 Atapered pipe thread
R 1/4 instraight (form A)DIN 71412 Atapered pipe thread
1/4-28 UNFstraightinch seriesimported and automotive equipment
Inside the plant

Manufactured in our own plant

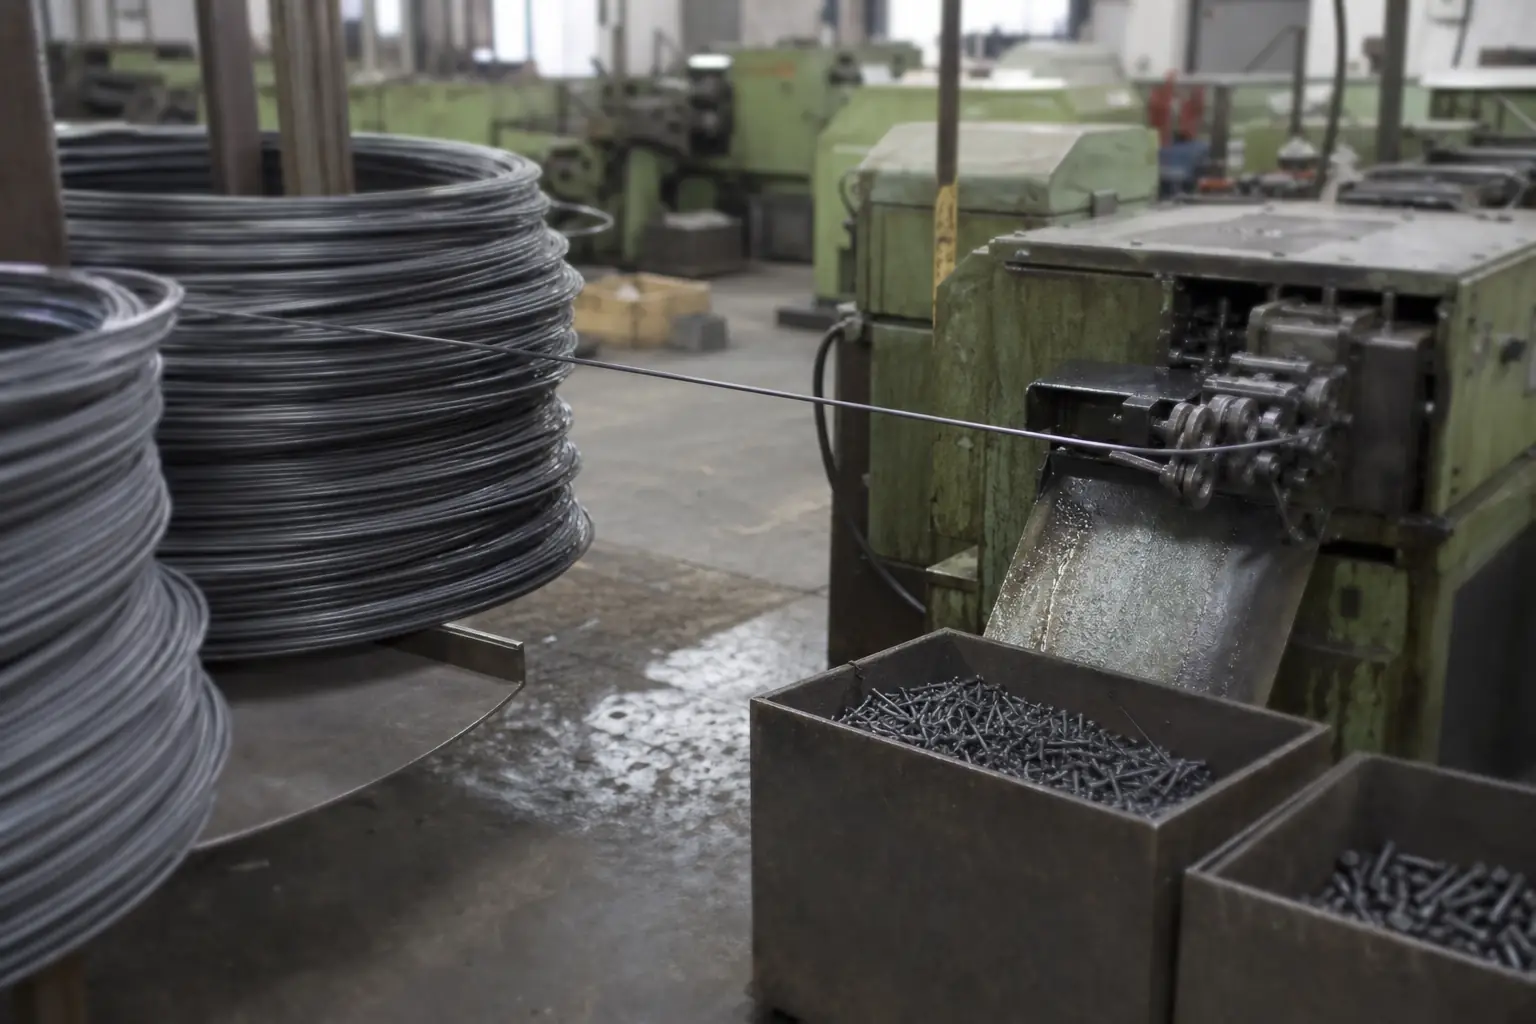
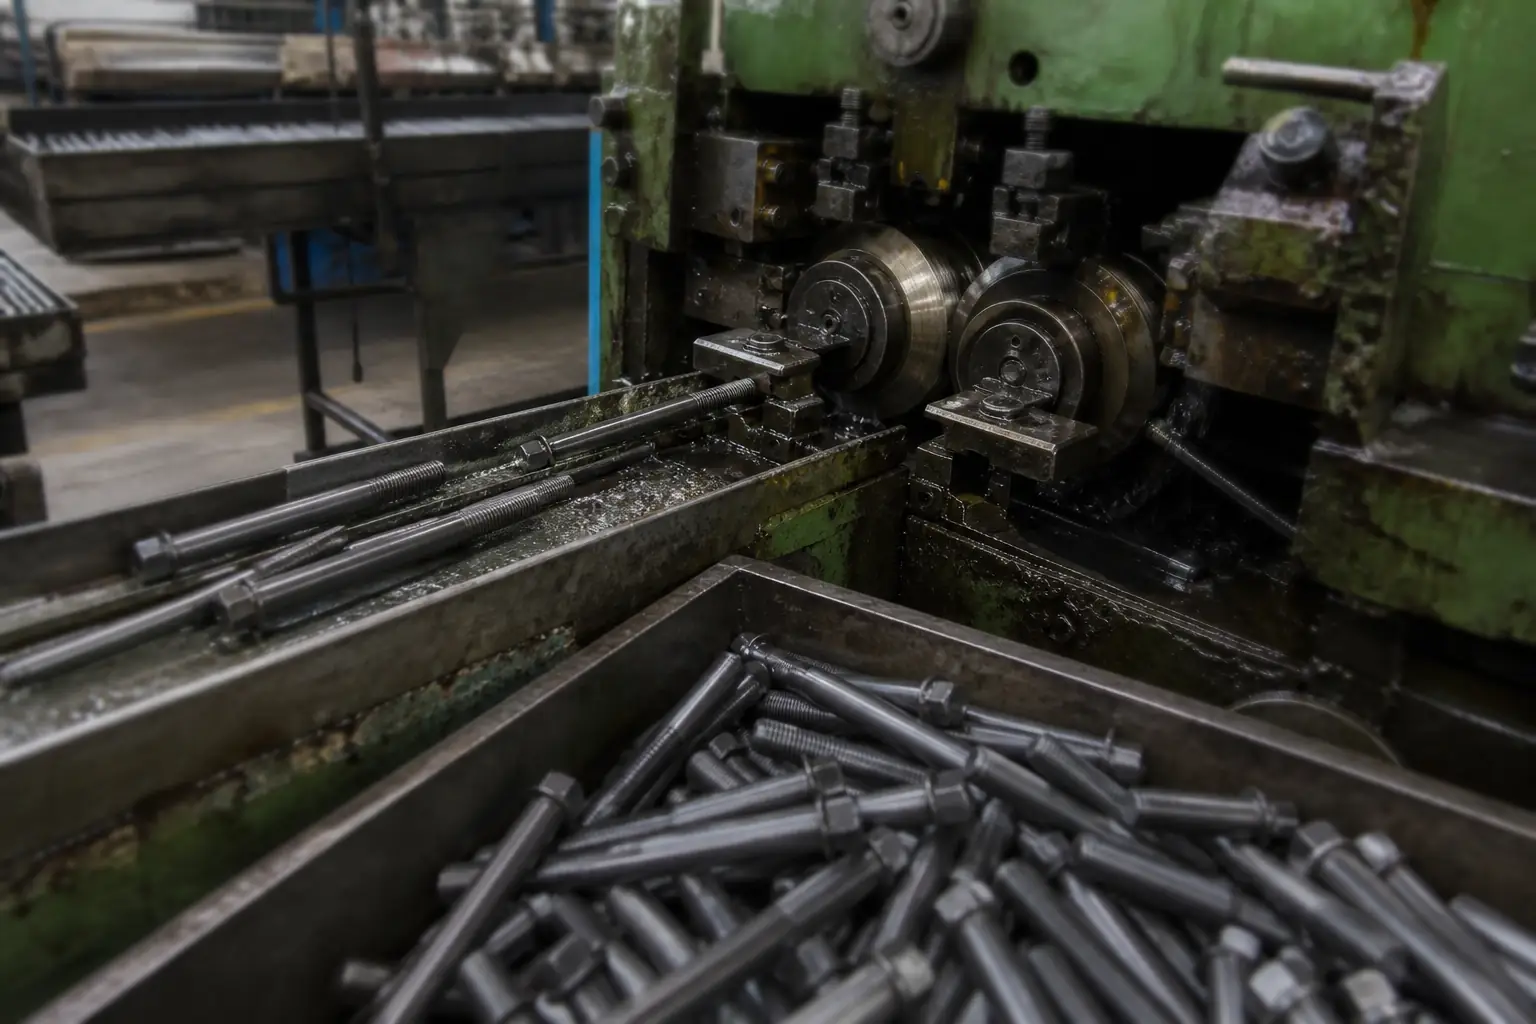
This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.

  1. Wire rod feeding into a cold heading machine
    01

    Cold heading

    Wire rod is drawn to size and cold-formed into blanks. Forming rather than cutting keeps the grain flow continuous around the head, which is where a bolt is most likely to fail.

    Head dimensions and under-head radius checked at set-up and per shift.

  2. Thread rolling machine producing bolt threads
    02

    Thread rolling

    Threads are rolled between hardened dies rather than cut. Rolled threads are stronger in fatigue than cut threads and hold pitch and flank angle far more consistently across a batch.

    Go / no-go ring gauges to ISO 965 tolerance class 6g.

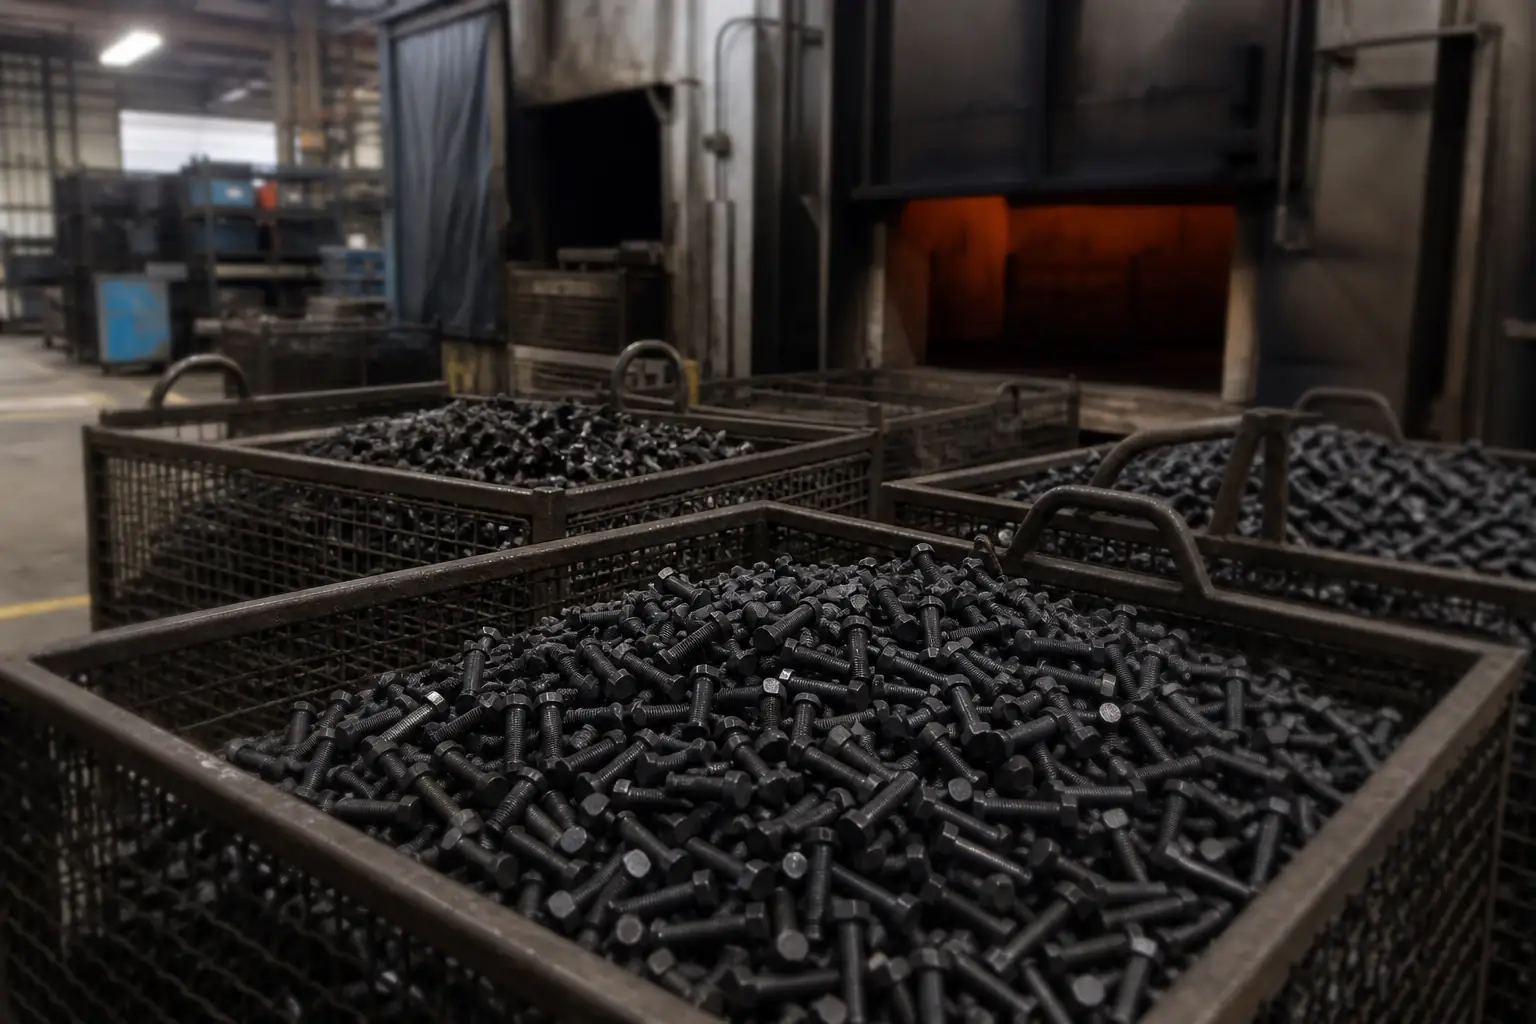
  3. Baskets of bolts staged for heat treatment
    03

    Heat treatment

    Quench-and-temper brings carbon and alloy steel to the property class ordered — 8.8, 10.9 or 12.9 — with the furnace charge tracked so a finished lot can be traced back to it.

    Core hardness and tensile tested per lot to ISO 898-1.

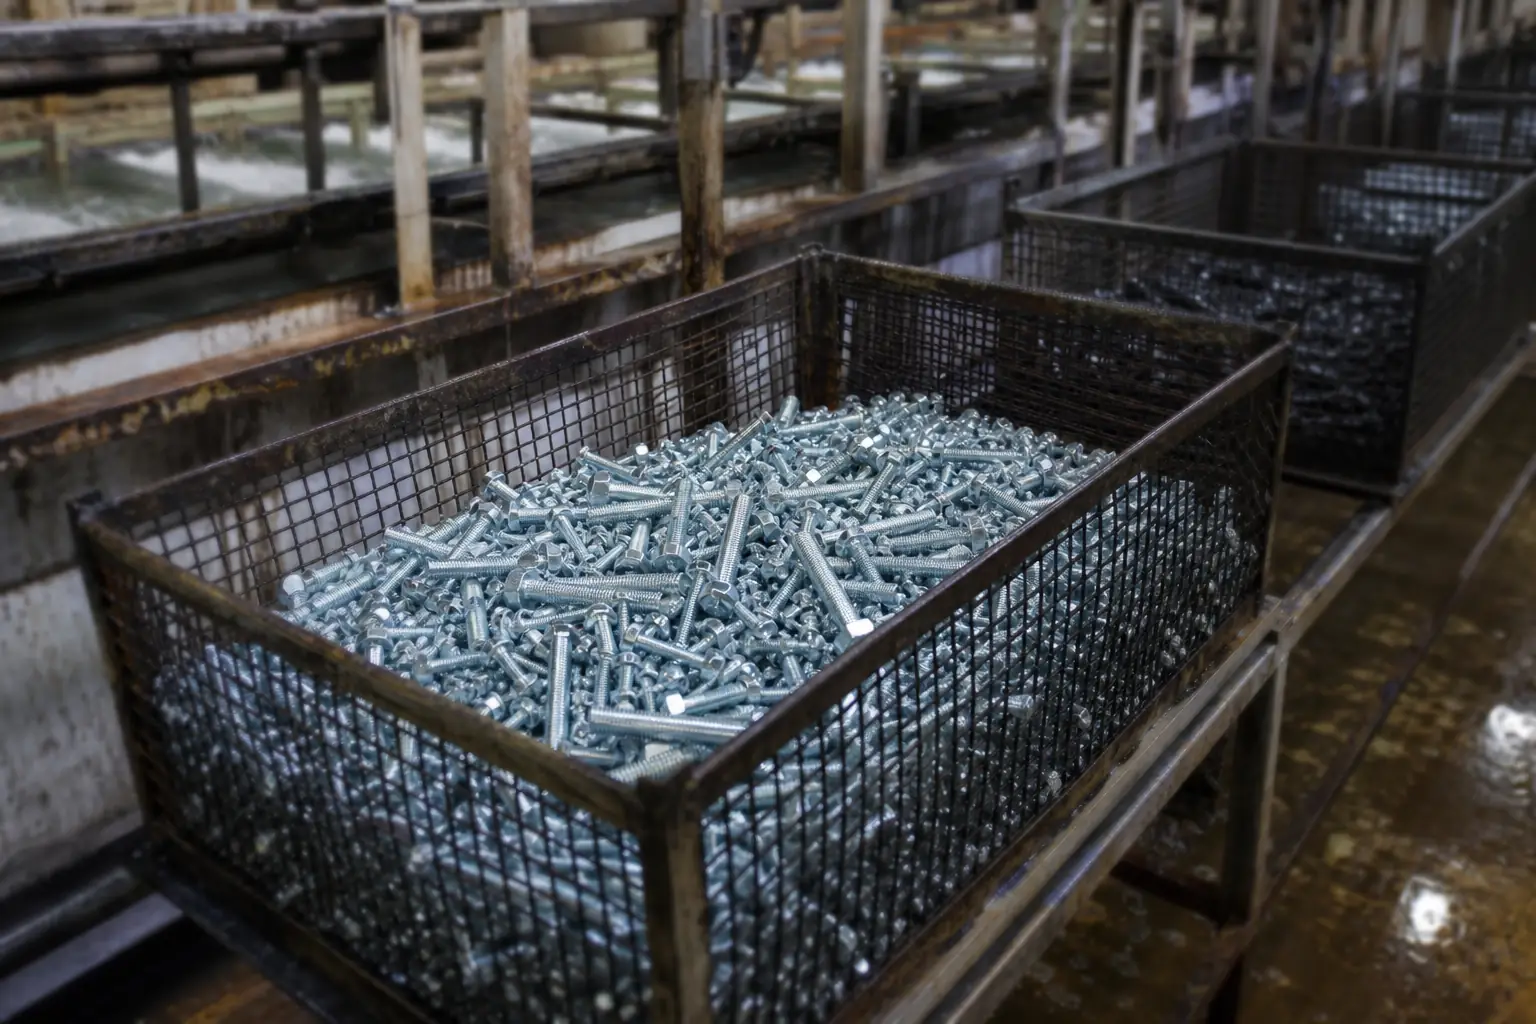
  4. Zinc plated bolts in a treatment basket
    04

    Surface treatment

    Zinc, zinc-nickel, hot-dip galvanizing, black oxide, phosphate and Dacromet, selected against the service environment rather than against the price list.

    Coating thickness and neutral salt spray hours to ISO 9227.

Frequently Asked Questions

What are Grease Nipples (DIN 71412) used for?

Joining and sealing fluid or pneumatic lines. They are supplied to DIN 71412 / ISO 6392 (lubricating nipples).

Which industries use Grease Nipples (DIN 71412)?

They are commonly specified in hydraulic & fluid power, process & plant piping and general machine building, among other sectors.

How do I choose the right size of Grease Nipples (DIN 71412)?

Match the nominal size to the mating thread or hole. This product is available from 1 to 10; the full dimension table on this page lists each size.

Can I mix BSP and NPT Grease Nipples (DIN 71412)?

Not directly — the thread forms differ in angle and taper. Use a dedicated BSP-to-NPT adapter, and seal with the method suited to the thread (tape, sealant or O-ring).

Can I get a quote for Grease Nipples (DIN 71412) in the size and material I need?

Yes. Use the technical drawing and quote form on this page to set the size and options, then send the exact configuration to our team for pricing and lead time.