Skip to content
Screws · ASME B18.6.3 · Application guide

What Are Machine Screws, Inch (UNC & UNF) Used For?

Typical applications, the industries that specify machine screws, inch (unc & unf), and how to choose the right size, material and finish for the joint.

Machine Screws, Inch (UNC & UNF) are used for assemblies dimensioned in the inch gauge series, where a metric screw of similar diameter simply will not thread. They are manufactured to ASME B18.6.3, and the choice of size, property class and finish is driven by the load in the joint and the environment it sits in.

Primary duty
Assemblies dimensioned in the inch gauge series, where a metric screw of similar diameter simply will not thread
Governing standard
ASME B18.6.3
Screw size range
1/4" to #10
Category
Screws

Application notes are general engineering guidance. Verify the property class and any approval requirement against your own design calculation.

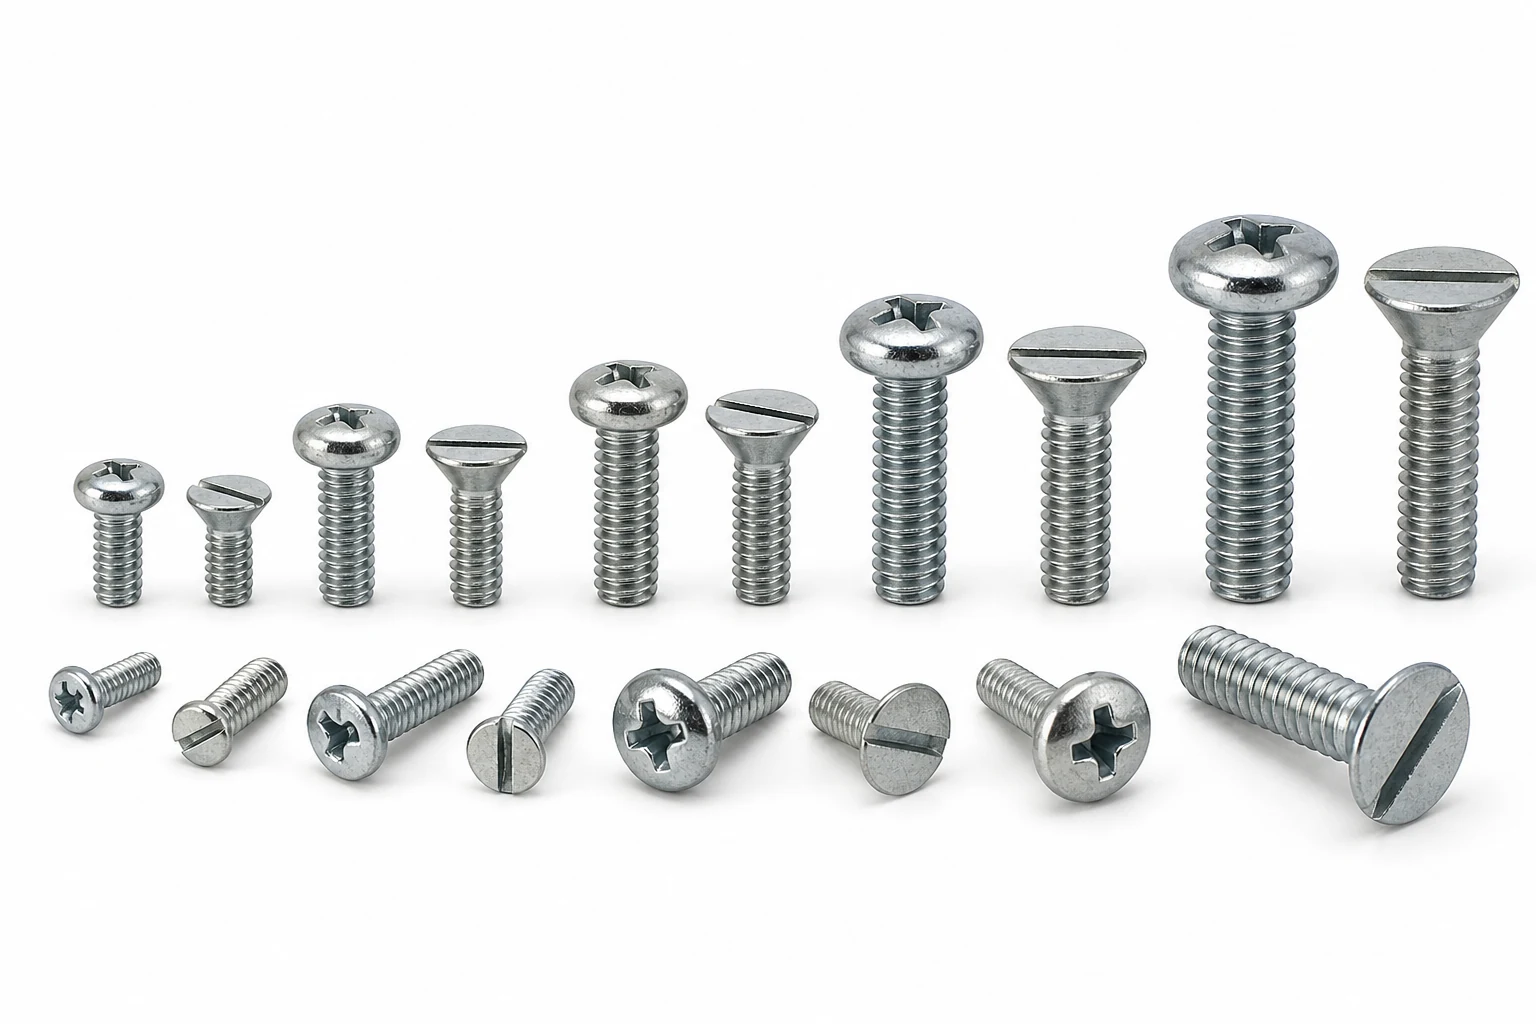
What Are Machine Screws, Inch (UNC & UNF) Used For? application image

Machine Screws, Inch (UNC & UNF) (ASME B18.6.3) are specified where the joint requires assemblies dimensioned in the inch gauge series, where a metric screw of similar diameter simply will not thread. The sections below cover the typical end-uses by industry, the size and material decisions for each, assembly practice, and the applications this fastener type is not suited to. Stocked across roughly 1 to 10, they cover general to heavy-duty work.

Typical Applications for Machine Screws, Inch (UNC & UNF)

The most common settings where these are specified:

  • Appliances & consumer goods: high-volume assembly with power tools and consistent seating.
  • Machine guarding & panels: removable access covers that are opened for service.
  • General machine building: fastening covers, brackets, motors and sub-assemblies on production equipment.
  • Maintenance & repair (MRO): a stocked size for servicing existing plant where the original fastener spec must be matched.
  • Fabrication & metalwork: bench and on-site assembly of steel frames, enclosures and weldments.

How to Specify Machine Screws, Inch (UNC & UNF) for Your Application

  • Size: Match the nominal size to the mating thread or hole. This product spans 1–10; check the full table below for the exact dimensions of each size.
  • Drive & head: Pick the drive (socket, cross, slot) and head style for the tool access and seating surface; a recessed drive resists cam-out under power tools.
  • Environment: For damp, coastal or chemical exposure prefer A4/316 stainless or a suitable coating; indoors, plated steel or A2 is usually sufficient.
  • Standard: This product is supplied to ASME B18.6.3. Quoting the standard on your order guarantees interchangeable dimensions between suppliers.

Installation & Assembly Practice

  • Match the driver exactly to the recess (PH ≠ PZ; hex key sizes per ISO 2936) and keep the tool axial — side load is the main cause of stripped drives.
  • In tapped holes, engage a thread length of at least 1× the nominal diameter in steel, 2× in aluminum.
  • Set power tools to a torque that seats the head without embedding it into the mating surface.

Common Selection Mistakes with Machine Screws, Inch (UNC & UNF)

  • Under-sizing the drive for the installation torque — a small recess at high torque strips before the screw is seated.
  • Using a countersunk head in thin sheet where the countersink removes most of the load-bearing material.
  • Specifying stainless in high-strength duty: A2-70 is roughly class 7 steel, not a 10.9 substitute.

Where Machine Screws, Inch (UNC & UNF) Are Not the Right Choice

Not for high-preload structural joints (use a property-class bolt and nut), and not in thin sheet where a self-drilling or self-tapping type suits better.

Custom manufacturing · Made to drawing

Need a machine screws, inch (unc & unf) outside the standard range?

Lengths and thread lengths outside the standard table are the commonest request, followed by a drive the standard does not offer and a head marked with your own part number. Made by cold heading or warm forging.

Minimum order from 2,000 pieces; samples within 7 days of drawing approval.
Custom screw manufacturingSend a drawing

Technical Drawing

Customize the parameters below — every spec field is editable, and the drawing redraws to match the values you choose. Changing the size will snap the other fields to that size's standard values; you can then override any individual value.

Dimensioned line drawing of #2 Machine Screws, Inch (UNC & UNF) to ASME B18.6.3. Side view and top view, drawn to the dimensions in the table below and redrawn for any size selected.
UNC threads per inch
56
UNF threads per inch
64
Major diameter (in)
0.086
Pan head diameter (in)
0.167
Pan head height (in)
0.053
Drive
PH1
Sends the selected values to the quote form below.

Request a Quote

The form below follows the current technical drawing configuration. Change the drawing values above and the request details update automatically.

Request a Quotation

Specification
Business Information

Dimensions & Specifications (ASME B18.6.3)

SizeUNC threads per inchUNF threads per inchMajor diameter (in)Pan head diameter (in)Pan head height (in)DriveReference standard
#256640.0860.1670.053PH1ASME B18.6.3
#440480.1120.2190.068PH1ASME B18.6.3
#632400.1380.2700.082PH2ASME B18.6.3
#832360.1640.3220.096PH2ASME B18.6.3
#1024320.1900.3730.110PH2ASME B18.6.3
1/4"20280.2500.4920.144PH2 / PH3ASME B18.6.3
Inside the plant

Manufactured in our own plant

This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.

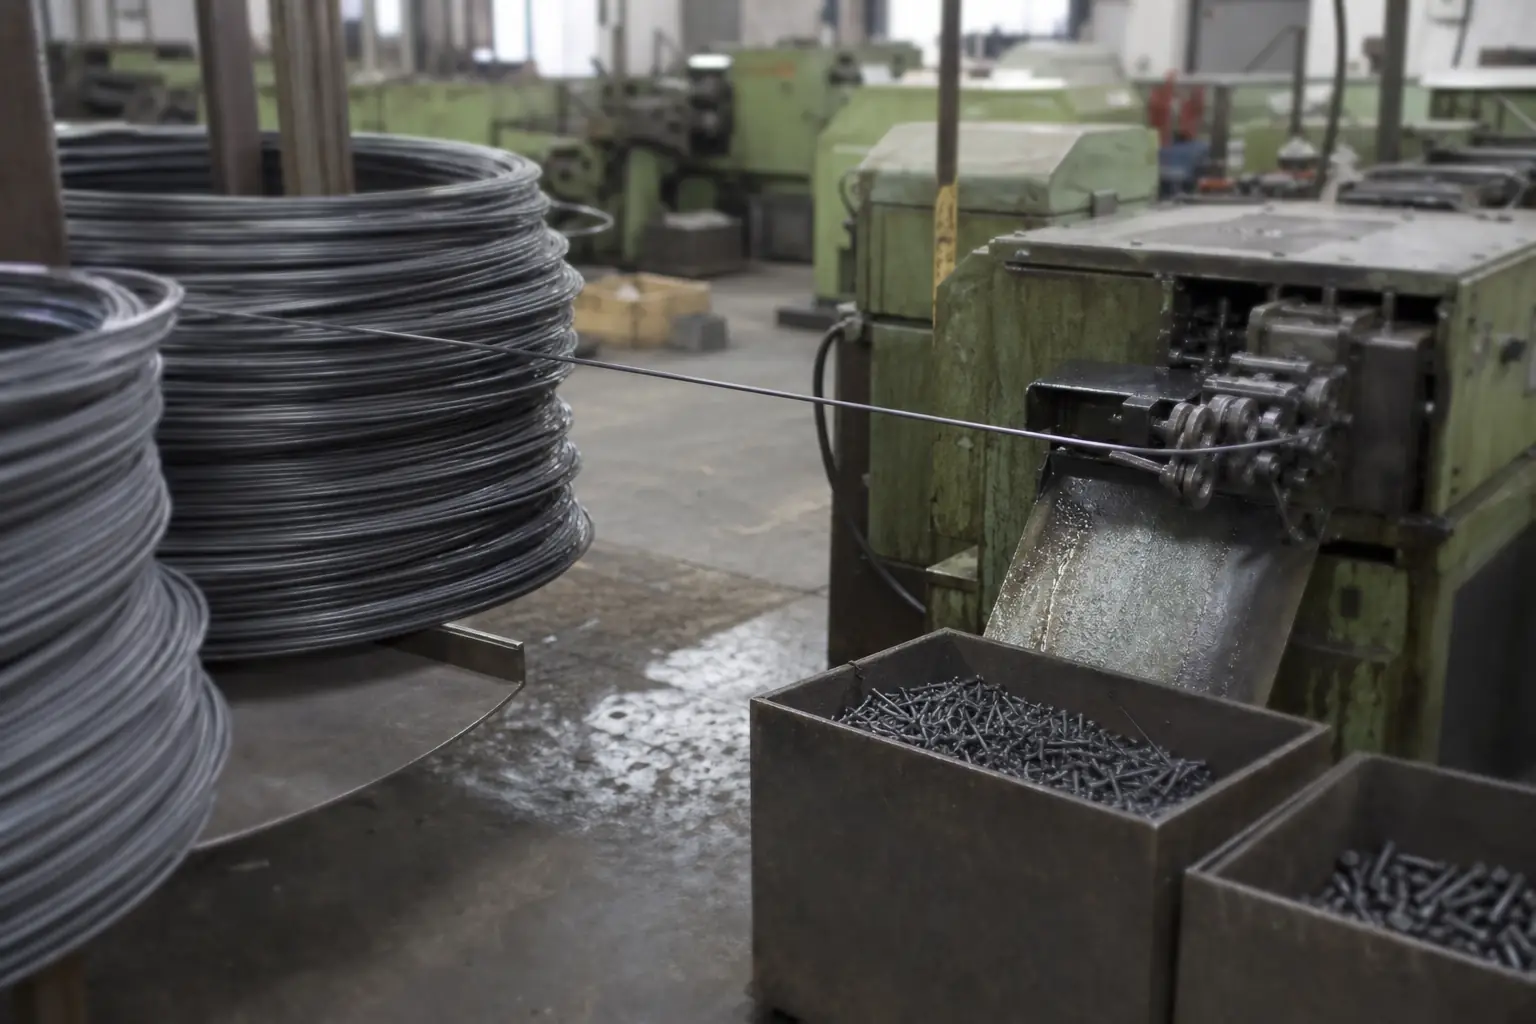
  1. Wire rod feeding into a cold heading machine
    01

    Cold heading

    Wire rod is drawn to size and cold-formed into blanks. Forming rather than cutting keeps the grain flow continuous around the head, which is where a bolt is most likely to fail.

    Head dimensions and under-head radius checked at set-up and per shift.

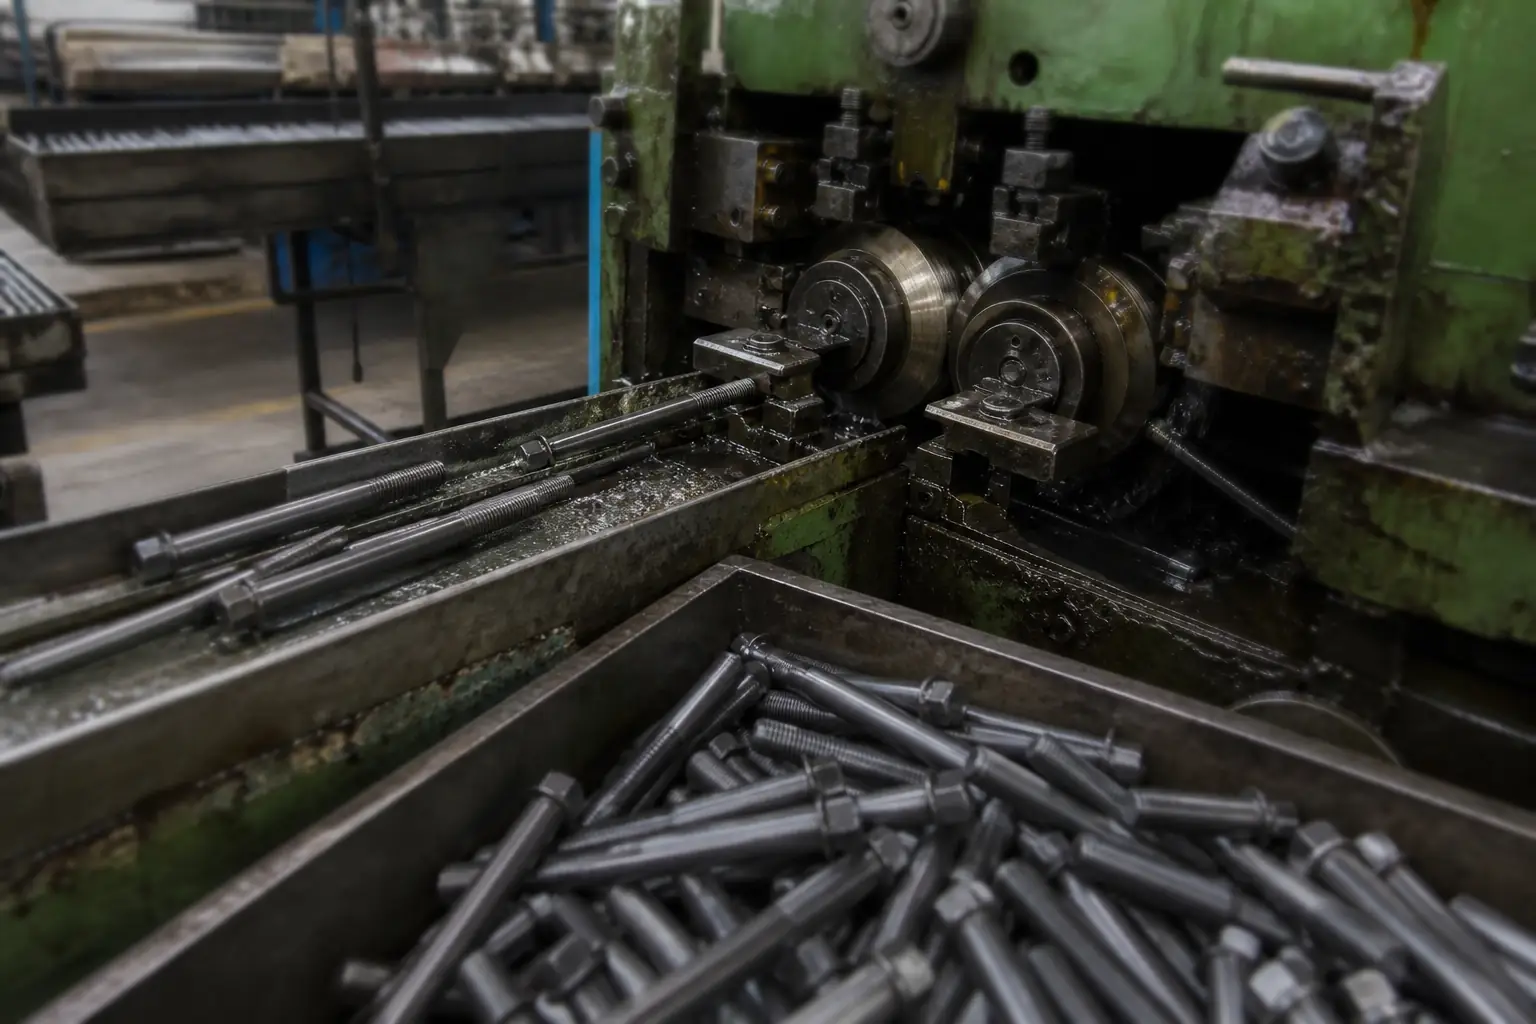
  2. Thread rolling machine producing bolt threads
    02

    Thread rolling

    Threads are rolled between hardened dies rather than cut. Rolled threads are stronger in fatigue than cut threads and hold pitch and flank angle far more consistently across a batch.

    Go / no-go ring gauges to ISO 965 tolerance class 6g.

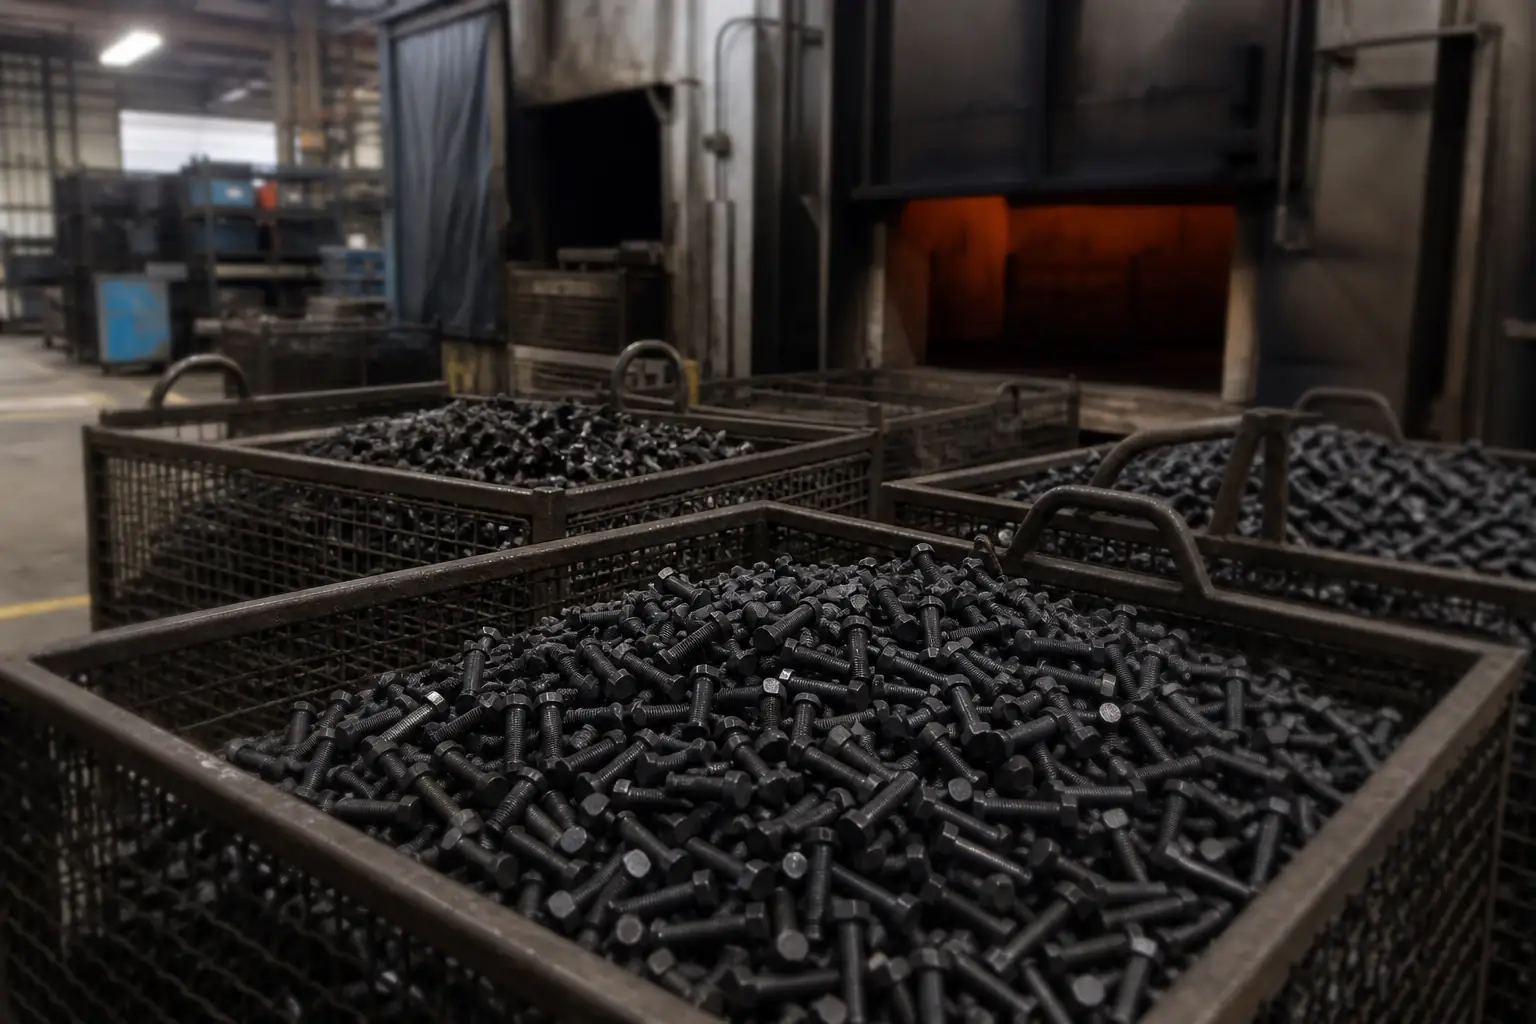
  3. Baskets of bolts staged for heat treatment
    03

    Heat treatment

    Quench-and-temper brings carbon and alloy steel to the property class ordered — 8.8, 10.9 or 12.9 — with the furnace charge tracked so a finished lot can be traced back to it.

    Core hardness and tensile tested per lot to ISO 898-1.

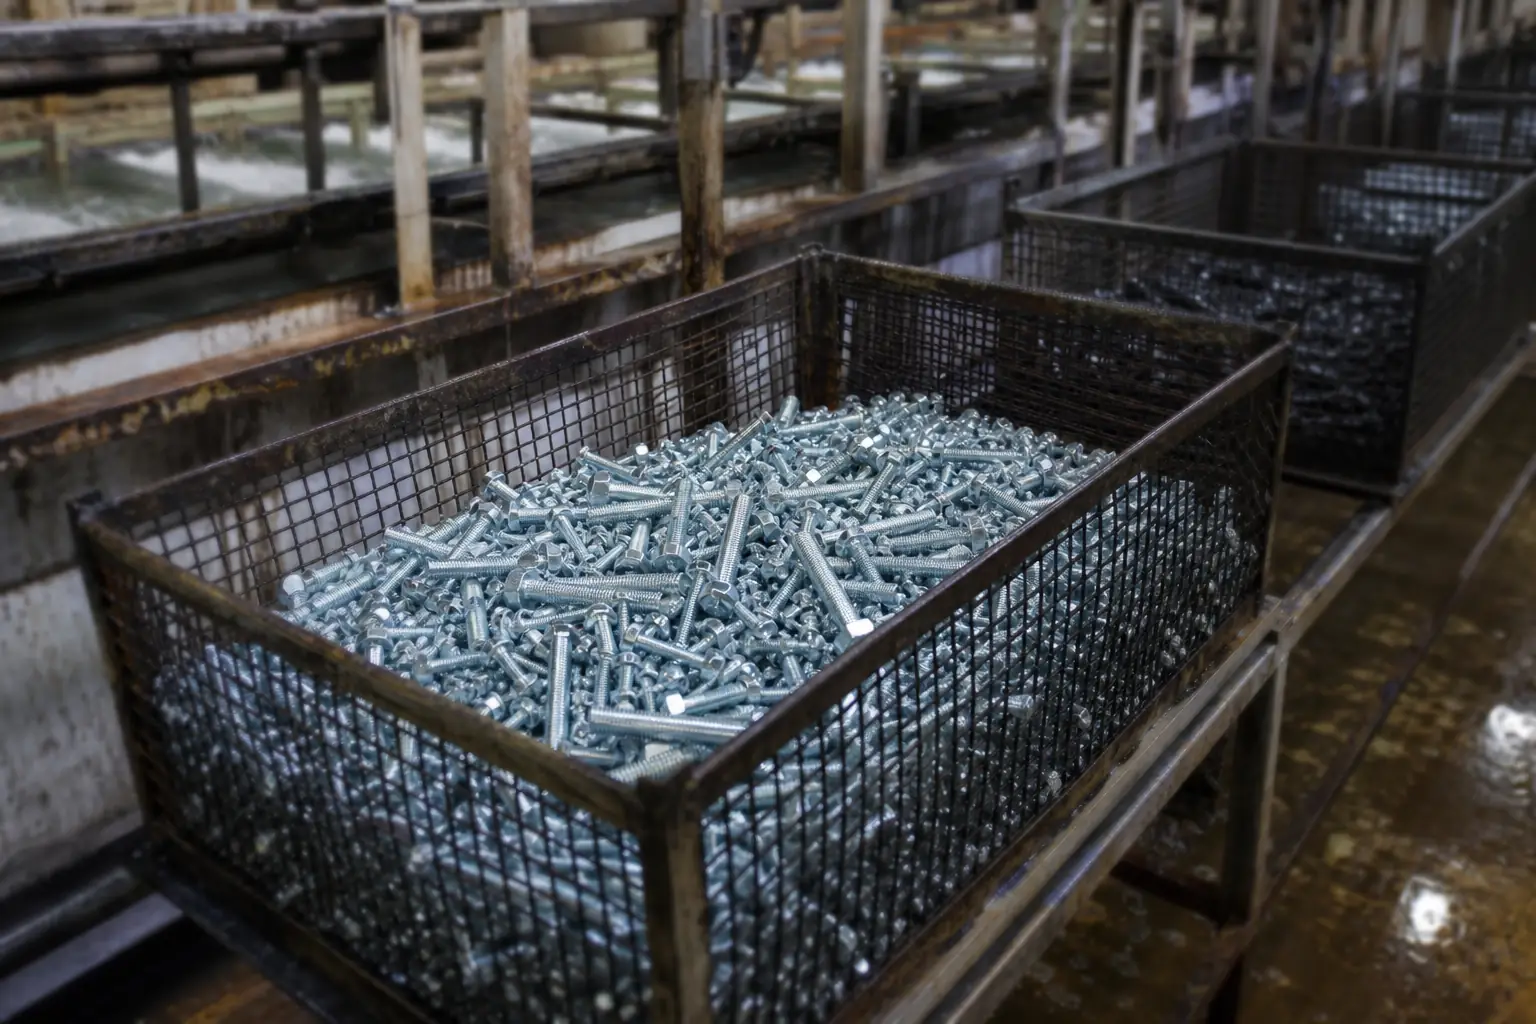
  4. Zinc plated bolts in a treatment basket
    04

    Surface treatment

    Zinc, zinc-nickel, hot-dip galvanizing, black oxide, phosphate and Dacromet, selected against the service environment rather than against the price list.

    Coating thickness and neutral salt spray hours to ISO 9227.

Frequently Asked Questions

What material should Machine Screws, Inch (UNC & UNF) be for outdoor use?

For damp, coastal or chemical environments specify A4 (316) stainless or a suitably coated steel. For indoor or dry use, A2 (304) stainless or zinc-plated steel is normally adequate.

Are Machine Screws, Inch (UNC & UNF) made to a recognized standard?

Yes — they are manufactured to ASME B18.6.3, so dimensions are interchangeable between suppliers when you quote the standard on your order.

What are Machine Screws, Inch (UNC & UNF) used for?

Assemblies dimensioned in the inch gauge series, where a metric screw of similar diameter simply will not thread. They are supplied to ASME B18.6.3.

Which industries use Machine Screws, Inch (UNC & UNF)?

They are commonly specified in fabrication & metalwork, electronics & enclosures and appliances & consumer goods, among other sectors.

Can I get a quote for Machine Screws, Inch (UNC & UNF) in the size and material I need?

Yes. Use the technical drawing and quote form on this page to set the size and options, then send the exact configuration to our team for pricing and lead time.