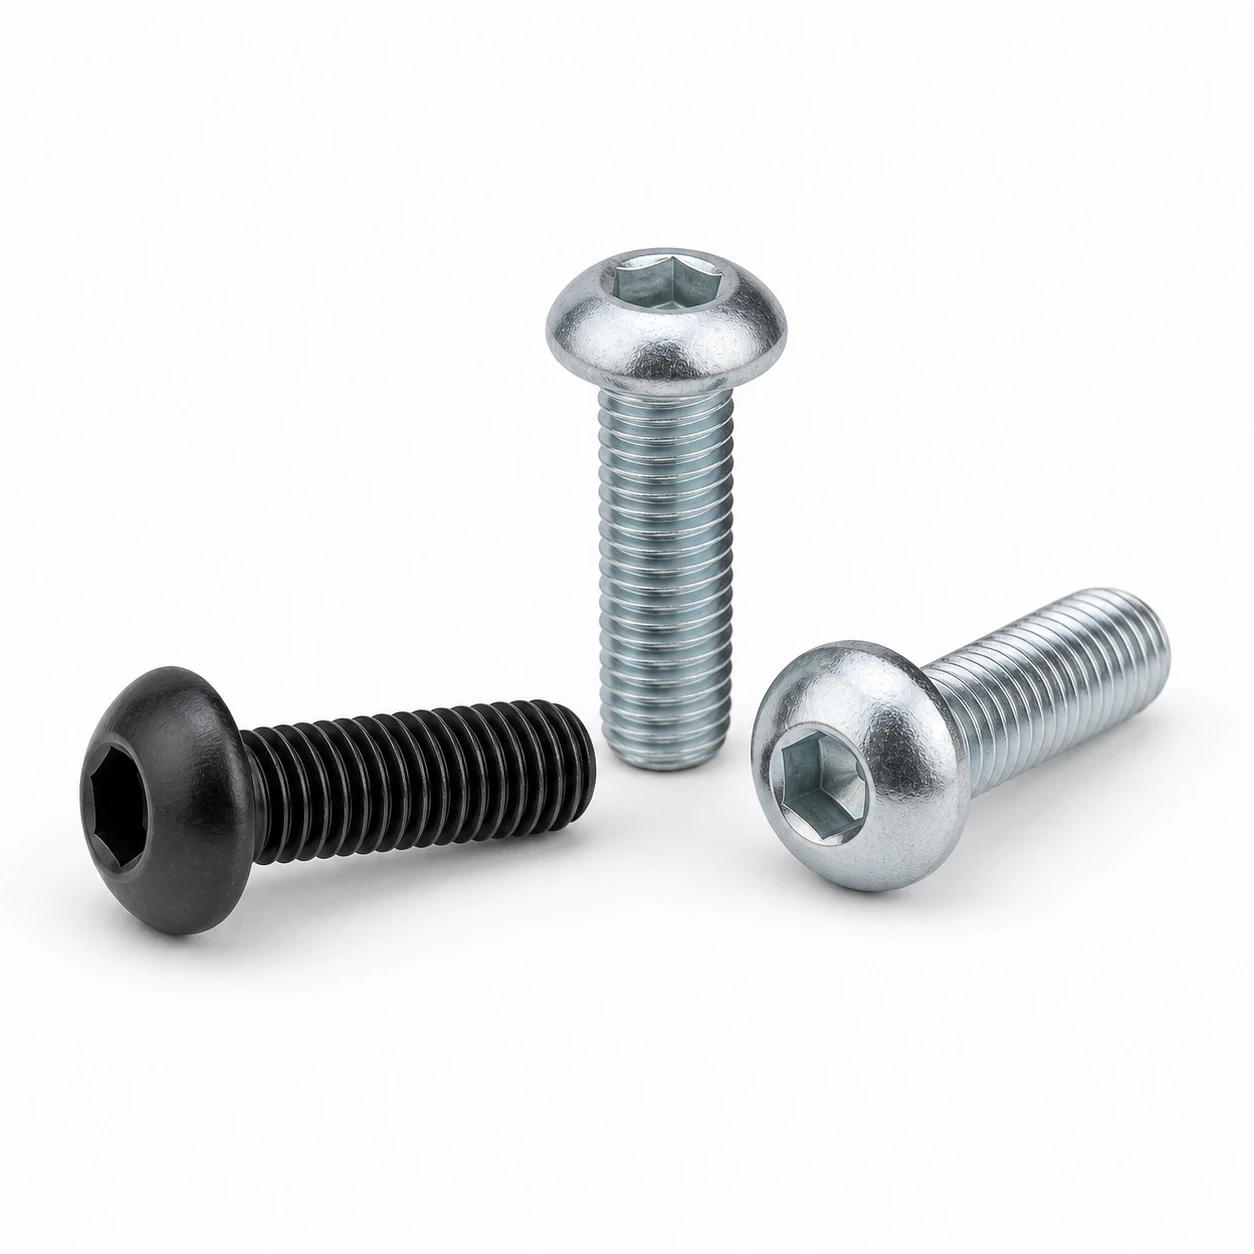
Button Head Socket Screws are selected when an assembly calls for threaded assemblies where the head drive and seating style matter. This application guide to the ISO 7380 type covers concrete end-uses, the specification checklist, correct installation, and where an alternative fastener performs better. Stocked across roughly M3 to M20, they cover general to heavy-duty work.
Typical Applications for Button Head Socket Screws
The most common settings where these are specified:
- Appliances & consumer goods: high-volume assembly with power tools and consistent seating.
- Machine guarding & panels: removable access covers that are opened for service.
- General machine building: fastening covers, brackets, motors and sub-assemblies on production equipment.
- Maintenance & repair (MRO): a stocked size for servicing existing plant where the original fastener spec must be matched.
- Fabrication & metalwork: bench and on-site assembly of steel frames, enclosures and weldments.
How to Specify Button Head Socket Screws for Your Application
- Size: Match the nominal size to the mating thread or hole. This product spans M3–M20; check the full table below for the exact dimensions of each size.
- Drive & head: Pick the drive (socket, cross, slot) and head style for the tool access and seating surface; a recessed drive resists cam-out under power tools.
- Environment: For damp, coastal or chemical exposure prefer A4/316 stainless or a suitable coating; indoors, plated steel or A2 is usually sufficient.
- Standard: This product is supplied to ISO 7380. Quoting the standard on your order guarantees interchangeable dimensions between suppliers.
Installation & Assembly Practice
- This is a reduced-height head. The head, not the thread, limits what the screw will carry — ISO 7380-1 caps a button head at roughly 80% of the thread's capacity — so the thread's proof load overstates the assembly. Size the joint on the head, or use a cap screw where the full class strength is needed.
- Match the driver exactly to the recess (PH ≠ PZ; hex key sizes per ISO 2936) and keep the tool axial — side load is the main cause of stripped drives.
- In tapped holes, engage a thread length of at least 1× the nominal diameter in steel, 2× in aluminum.
- Set power tools to a torque that seats the head without embedding it into the mating surface.
Common Selection Mistakes with Button Head Socket Screws
- Under-sizing the drive for the installation torque — a small recess at high torque strips before the screw is seated.
- Using a countersunk head in thin sheet where the countersink removes most of the load-bearing material.
- Specifying stainless in high-strength duty: A2-70 is roughly class 7 steel, not a 10.9 substitute.
Where Button Head Socket Screws Are Not the Right Choice
Not for high-preload structural joints (use a property-class bolt and nut), and not in thin sheet where a self-drilling or self-tapping type suits better.
Custom manufacturing · Made to drawing
Need a button head socket screws outside the standard range?
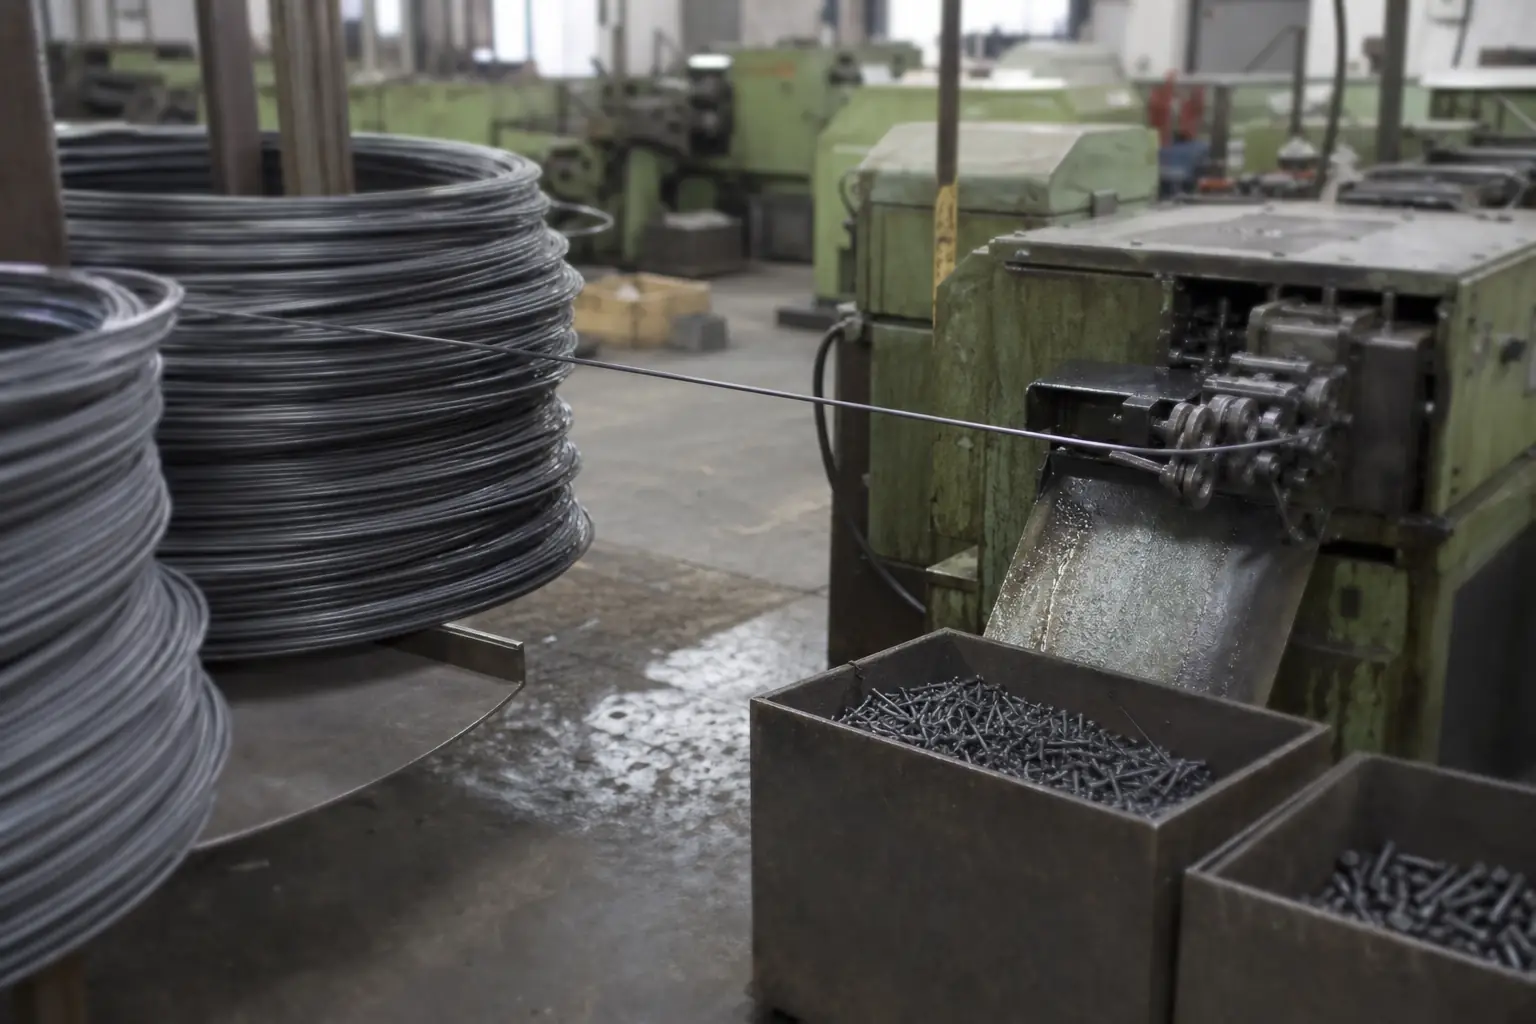
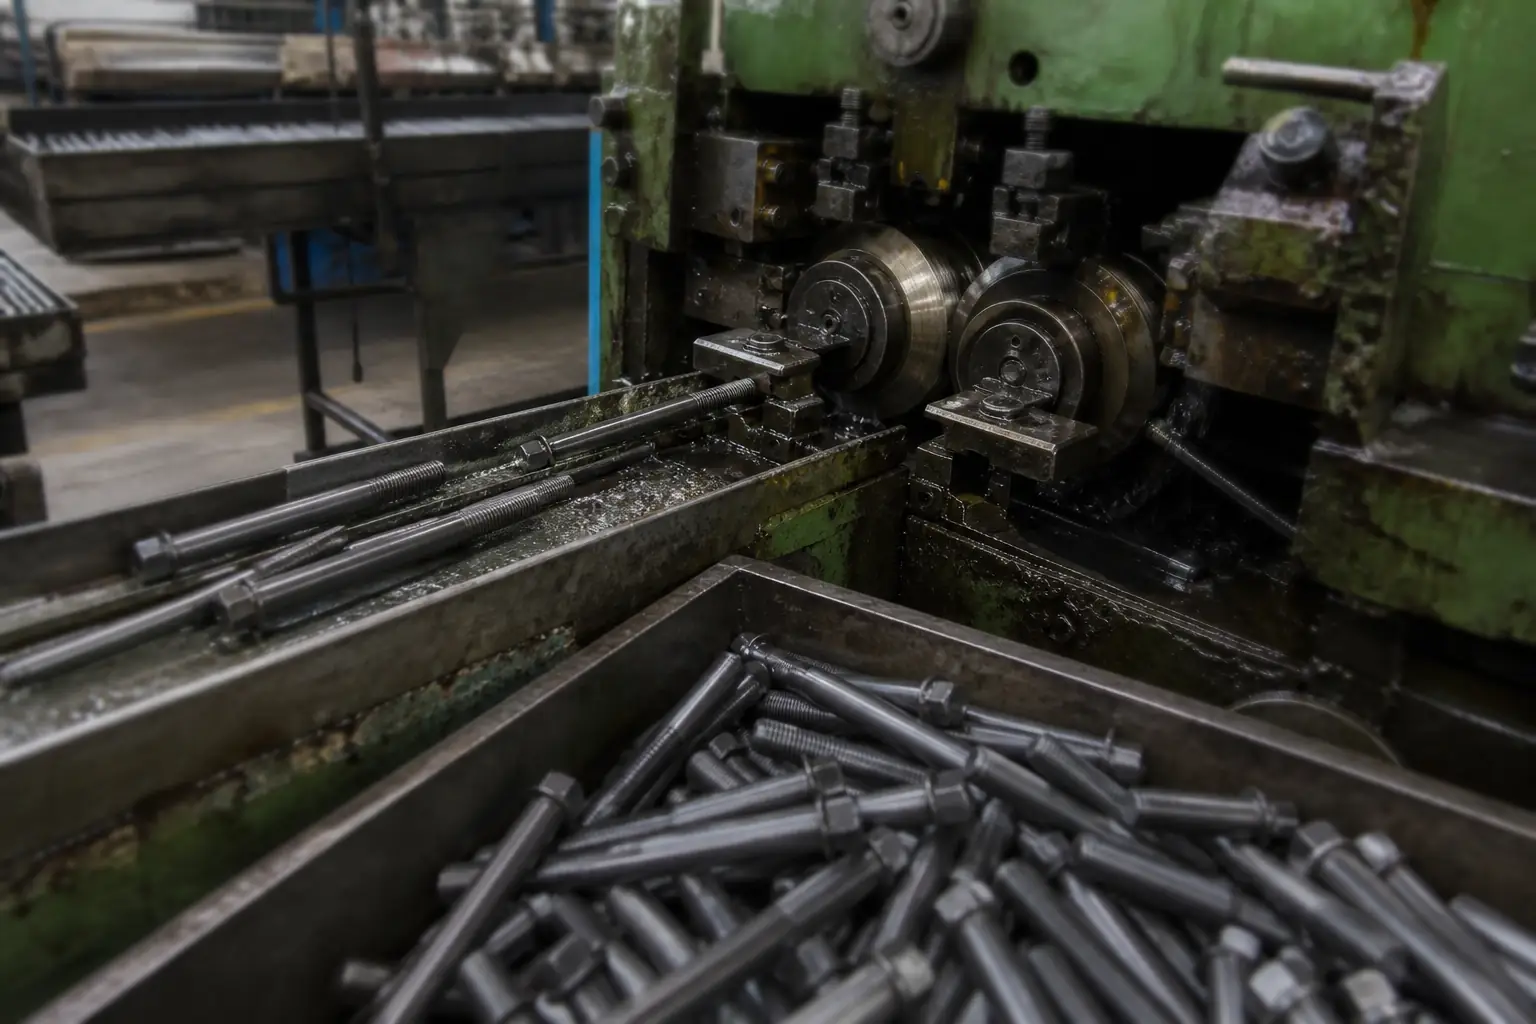
Head form and drive can be specified to the assembly rather than to a standard: a larger bearing face, a security drive, or a socket sized for the tool already on the bench. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.