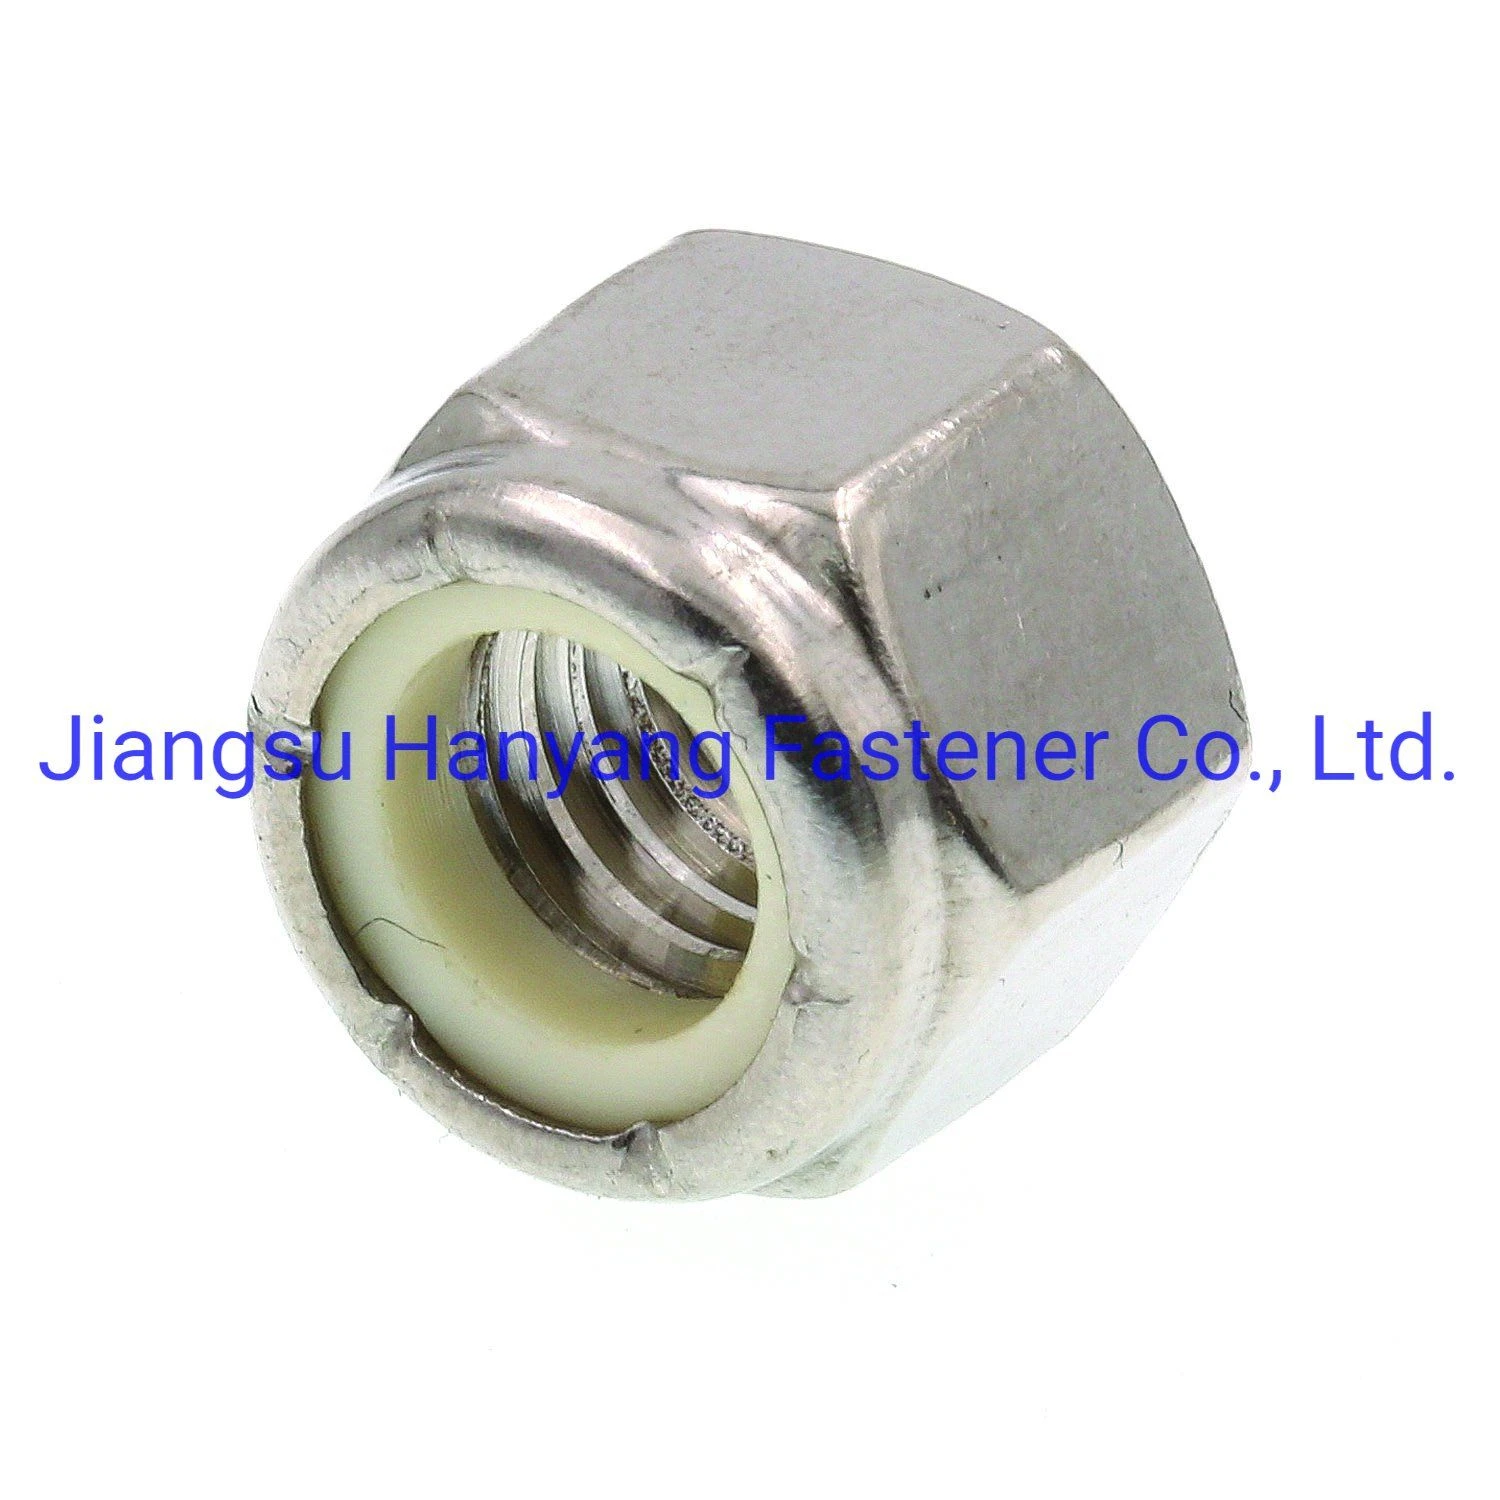

M10 Thin Nylon Insert Lock Nuts (DIN 985) are manufactured to DIN 985. This page lists the controlling dimensions for the M10 size together with the drive and the installation notes for this type.
Values are taken from the governing standard rather than from a general machine-thread table, because this type is not selected on one.
M10 Dimensional Row (DIN 985)
| Thread size | Pitch (mm) | Width across flats s (mm) | Total height m (mm) | Max service temperature (u00b0C) | Re-use | Property class | Reference standard |
|---|---|---|---|---|---|---|---|
| M10 | 1.5 | 17.0 | 10.0 | 120 | 5 cycles typical | 8 | DIN 985 |
Spanner & Drive for M10 Thin Nylon Insert Lock Nuts (DIN 985)
Drive geometry for M10 Thin Nylon Insert Lock Nuts (DIN 985) is given by the row above; match the tool to the listed values.
Tightening Torque for M10
| Class 8.8 (dry, ~µ 0.125) | ≈ 48 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 71 Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 83 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M10
Nuts are graded to ISO 898-2 by the proof load the nut itself will hold (classes 04, 05, 5, 6, 8, 10 and 12), not by the 8.8 / 10.9 / 12.9 scale used for bolts. A class-8 nut is the correct mate for a class-8.8 bolt, and the joint is designed on the bolt, so no bolt-tension figure is quoted here.
Mating Parts for M10
Pair M10 with the matching M10 bolt or screw, plus a M10 flat washer where required to distribute load on softer materials.
When to Step Up or Down from M10
When the joint preload approaches the proof load of M10 class 8.8, step up to M12 class 8.8 (or move to M10 class 10.9). When the joint is over-specified, M8 often saves weight and cost without losing the safety margin.
Custom manufacturing · Made to drawing
Need thin nylon insert lock nuts (din 985) in a size this table does not list?
This page covers M10 thin nylon insert lock nuts (din 985). Locking method is specifiable independently of the rest: nylon insert, all-metal deformed thread, serrated flange, or none. Made by cold heading or tapping.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.