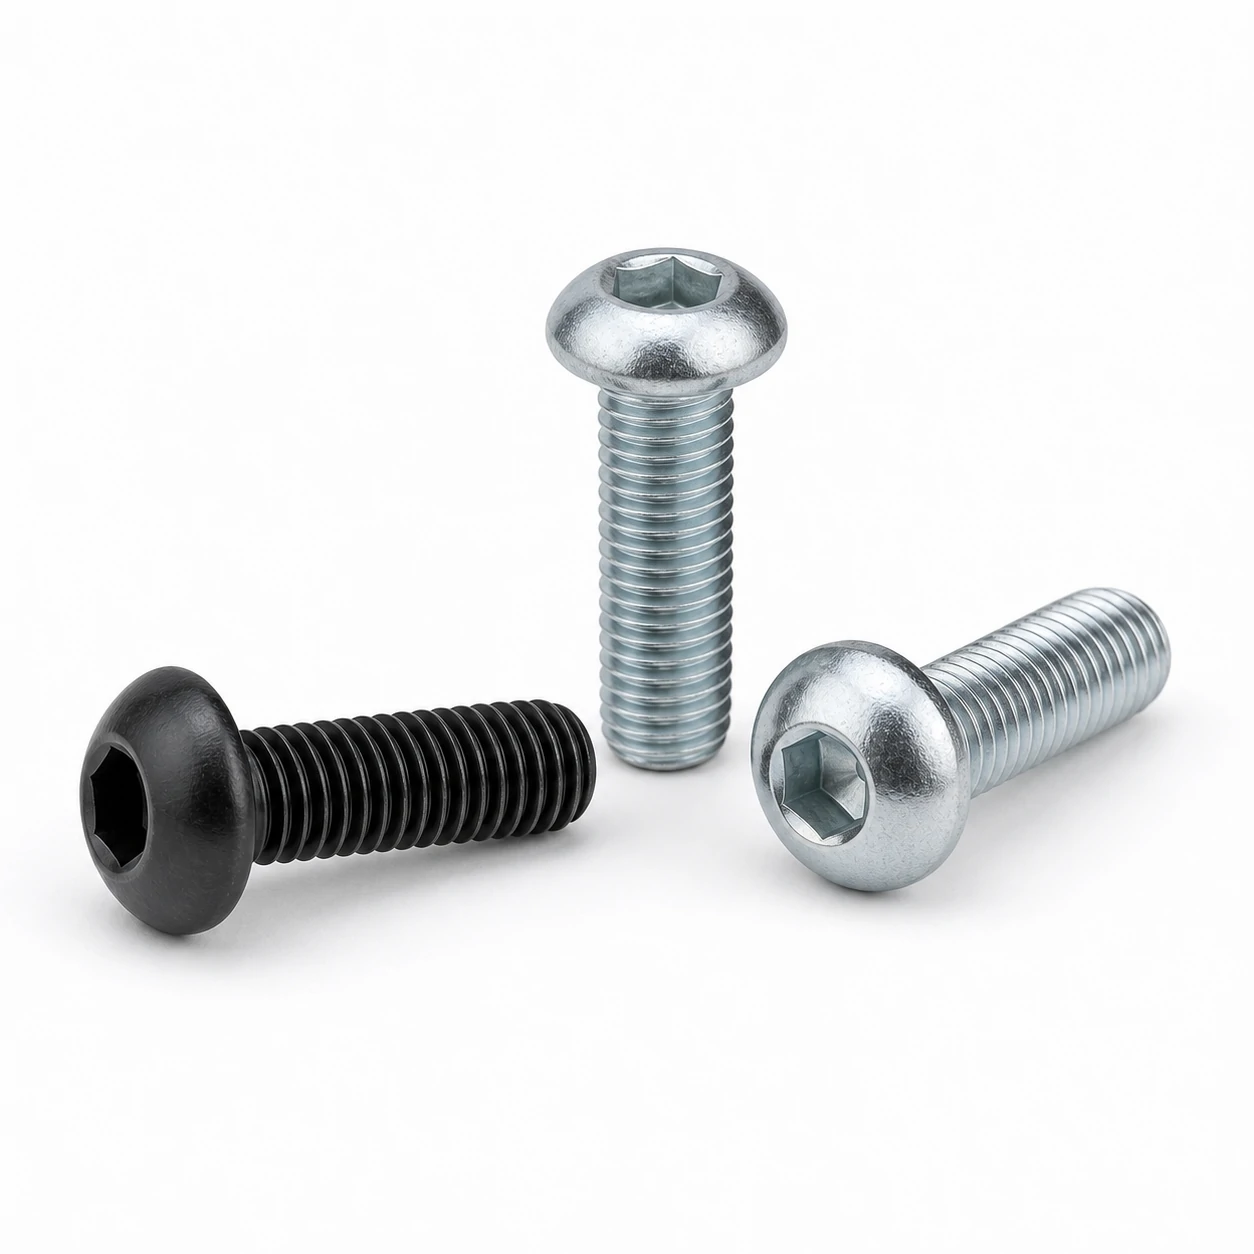
M14 Button Head Socket Screws dimensions to ISO 7380: head diameter 24.5 mm, head height 7.7 mm, coarse thread pitch 2 mm, clearance hole (ISO 273 medium) 15.5 mm. Tighten to approximately 134 Nm at property class 8.8 in a dry, as-supplied condition.
- Head diameter
- 24.5 mm
- Head height
- 7.7 mm
- Coarse thread pitch
- 2 mm
- Clearance hole (ISO 273 medium)
- 15.5 mm
- Tightening torque (class 8.8)
- 134 Nm
Figures are nominal values from the governing standard. Confirm against the tolerance class for your application before machining or ordering.
This page covers M14 Button Head Socket Screws to ISO 7380: the full dimensional row, hole and tool sizes, proof-load data and typical applications. All values are taken from the governing standards (ISO 7380 together with ISO 273, ISO 724 and ISO 898-1 where applicable).
M14 Dimensional Row (ISO 7380)
| Size | Pitch (mm) | Head diameter dk (mm) | Head height k (mm) | Hex socket s (mm) | Reference standard |
|---|
| M14 | 2.0 | 24.5 | 7.7 | 10.0 | ISO 7380-1 / DIN 7380 |
Spanner & Drive for M14 Button Head Socket Screws
The hex socket for M14 Button Head Socket Screws is shown in the spec table — use the matching Allen / hex key (an ISO 2936 hex key set covers the full range). For a one-off, a T-handle key and a calibrated arm will do. For a batch, the only way to get the same preload twice is a torque-controlled driver.
Hole Sizes for M14
| Coarse-thread pitch (ISO 724) | 2 mm |
|---|
| Through-hole / clearance (ISO 273 medium) | 15.5 mm |
|---|
| Tapping drill, coarse thread | 12 mm |
|---|
Tightening Torque for M14
| Class 8.8 (dry, ~µ 0.125) | ≈ 134 Nm |
|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 197 Nm |
|---|
| Class 12.9 (dry, ~µ 0.125) | ≈ 231 Nm |
|---|
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M14
This is a reduced-height head. The head, not the thread, limits what the screw will carry — ISO 7380-1 caps a button head at roughly 80% of the thread's capacity — so the thread's proof load overstates the assembly. Size the joint on the head, or use a cap screw where the full class strength is needed.
Installation Tips for M14 Button Head Socket Screws
- Use a quality Allen key fully seated in the socket — partial engagement is the most common cause of stripped sockets at this size.
- For countersunk and button-head variants, chamfer the through-hole to seat the head flush without preloading the head/shank fillet.
Mating Parts for M14
For M14, pair with a M14 hex nut (ISO 4032 / DIN 934) and, where used, a M14 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
Custom manufacturing · Made to drawing
Need button head socket screws in a size this table does not list?
This page covers M14 button head socket screws. Lengths and thread lengths outside the standard table are the commonest request, followed by a drive the standard does not offer and a head marked with your own part number. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.
Custom screw manufacturingSend a drawing
Applications & Industries for M14 Button Head Socket Screws
The sectors that buy Button Head Socket Screws to ISO 7380, and the duty each one buys them for. Stocked from M3 to M20.
Industries that specify Button Head Socket Screws
-
Automotive & transport
Chassis, driveline and body fixings that see vibration and are assembled to a controlled preload.
-
Steel fabrication
Bolted connections in frames, enclosures, walkways and weldments, on the bench and on site.
-
Energy & infrastructure
Tower, pipework, switchgear and plant fixings specified for long service life and inspectable joints.
-
Maintenance & MRO
Stocked replacements matched to an existing property class, thread and finish.
-
Food, pharma & cleanroom
Stainless assemblies that are washed down, where the finish matters as much as the strength.
-
Machine building & OEM
The default fastener on production equipment: covers, brackets, motor mounts and sub-assemblies tightened to a specified torque.
Typical applications
- bolting brackets, motors and gearboxes to a frame
- assemblies that are dismantled for service and re-torqued
- joints where the property class is stated on the drawing
- clamping two machined faces to a calculated preload
Service conditions to specify against
- Marine and coastal
- Available in A4 (316) stainless for chloride exposure — coastal structures, pool halls, water treatment and deck hardware, where A2 will eventually pit.
- High load
- Supplied in ISO 898-1 property classes, so the joint can be designed to a stated proof load and tightened to a calculated torque rather than by feel.
- Torque and preload
- The joint is designed around bolt tension, so lubrication, coating and the friction coefficient all change the torque figure — state them together.
Where to use something else
- Do not use a machine thread into unthreaded sheet or timber; use a tapping screw, rivet nut or insert made for that parent material.
Full application guide: where Button Head Socket Screws are used, how to specify them, and the cases they are wrong for