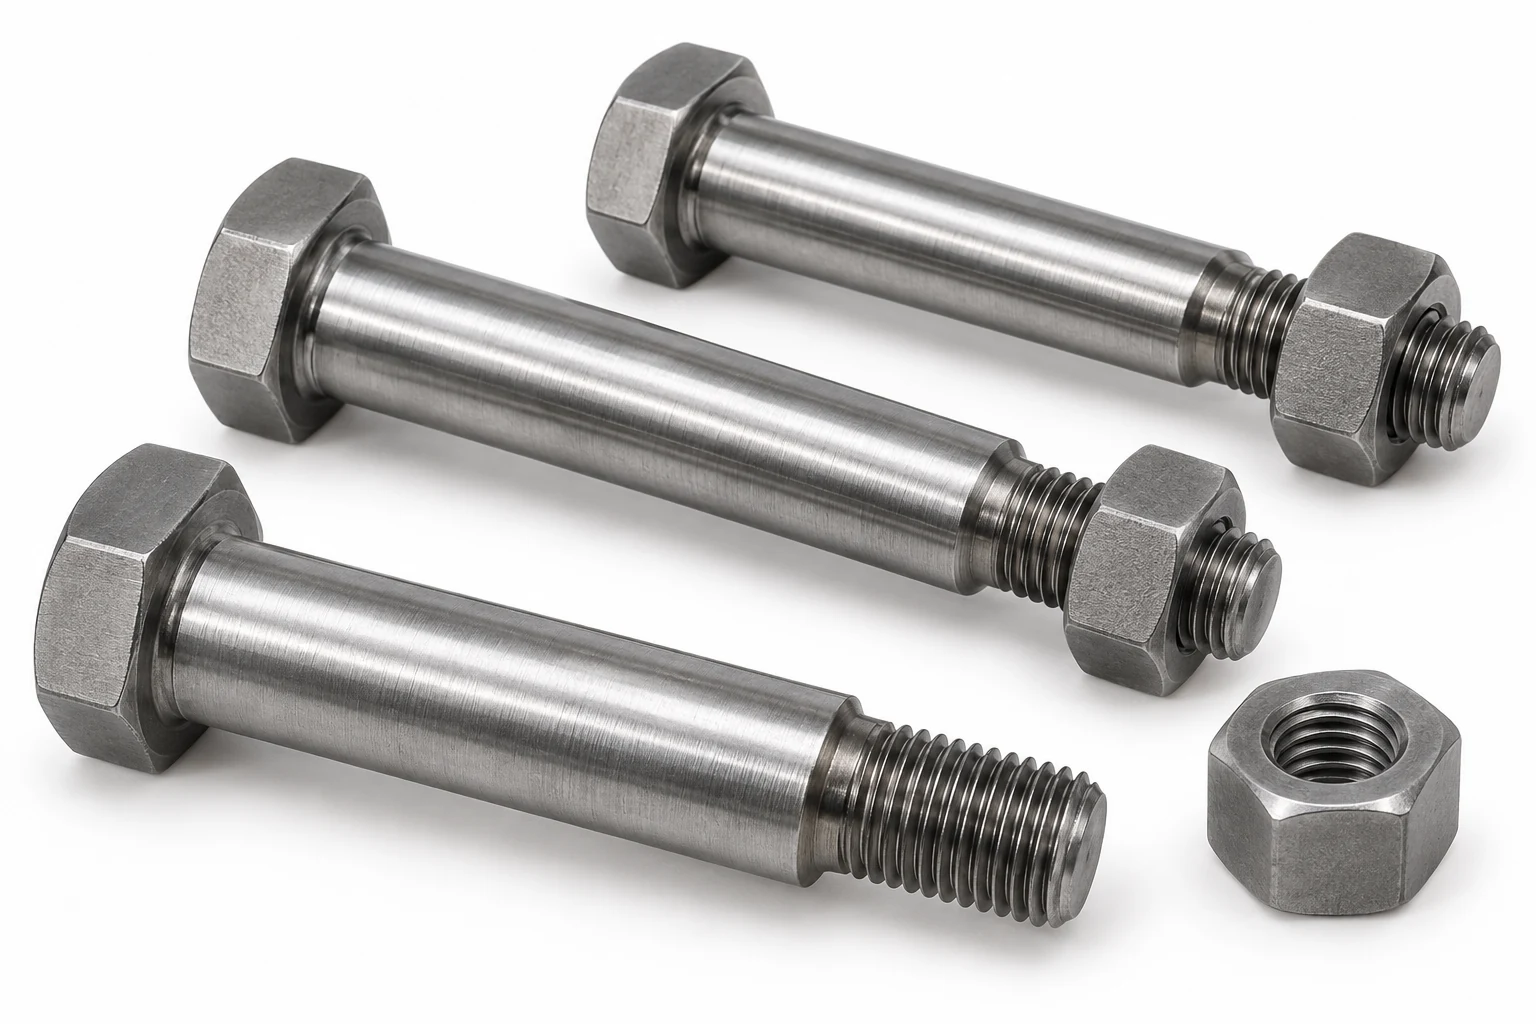
This page covers M16 Fitted (Reamer) Bolts, DIN 609 to DIN 609: the full dimensional row, hole and tool sizes, proof-load data and typical applications. All values are taken from the governing standards (DIN 609 together with ISO 273, ISO 724 and ISO 898-1 where applicable).
M16 Dimensional Row (DIN 609)
| Thread size | Shank diameter ds k6 (mm) | Reamed hole H7 (mm) | Width across flats s (mm) | Head height k (mm) | Common length range (mm) | Property class | Reference standard |
|---|---|---|---|---|---|---|---|
| M16 | 17 | 17 | 24 | 10.0 | 50~150 | 8.8 | DIN 609 |
Spanner & Drive for M16 Fitted (Reamer) Bolts, DIN 609
Drive geometry for M16 Fitted (Reamer) Bolts, DIN 609 is given by the row above; match the tool to the listed values.
Hole Sizes for M16
| Coarse-thread pitch (ISO 724) | 2 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 17.5 mm |
| Tapping drill, coarse thread | 14 mm |
Tightening Torque for M16
| Class 8.8 (dry, ~µ 0.125) | ≈ 210 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 295 Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 355 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M16
| Tensile stress area As (ISO 898-1) | 157 mm² |
|---|---|
| Proof load, class 8.8 | 91 kN |
| Proof load, class 10.9 | 130 kN |
| Proof load, class 12.9 | 152 kN |
| Min. ultimate tensile, class 8.8 | 126 kN |
Proof load = stress area × proof stress per ISO 898-1. Design joints so the working preload stays below the proof load of the selected class.
M16 Fitted (Reamer) Bolts, DIN 609 Weight
A steel M16 fitted (reamer) bolts, din 609 at the listed 50,150 mm length weighs approximately 89,396 g each — about 89,396 kg per 1,000 pieces. Stainless A2/A4 weighs roughly the same (density 7.9–8.0 g/cm³).
Actual weight varies slightly with head form, thread and finish; use this figure for freight estimation only.
Mating Parts for M16
For M16, pair with a M16 hex nut (ISO 4032 / DIN 934) and, where used, a M16 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
When to Step Up or Down from M16
When the joint preload approaches the proof load of M16 class 8.8, step up to M20 class 8.8 (or move to M16 class 10.9). When the joint is over-specified, M12 often saves weight and cost without losing the safety margin.