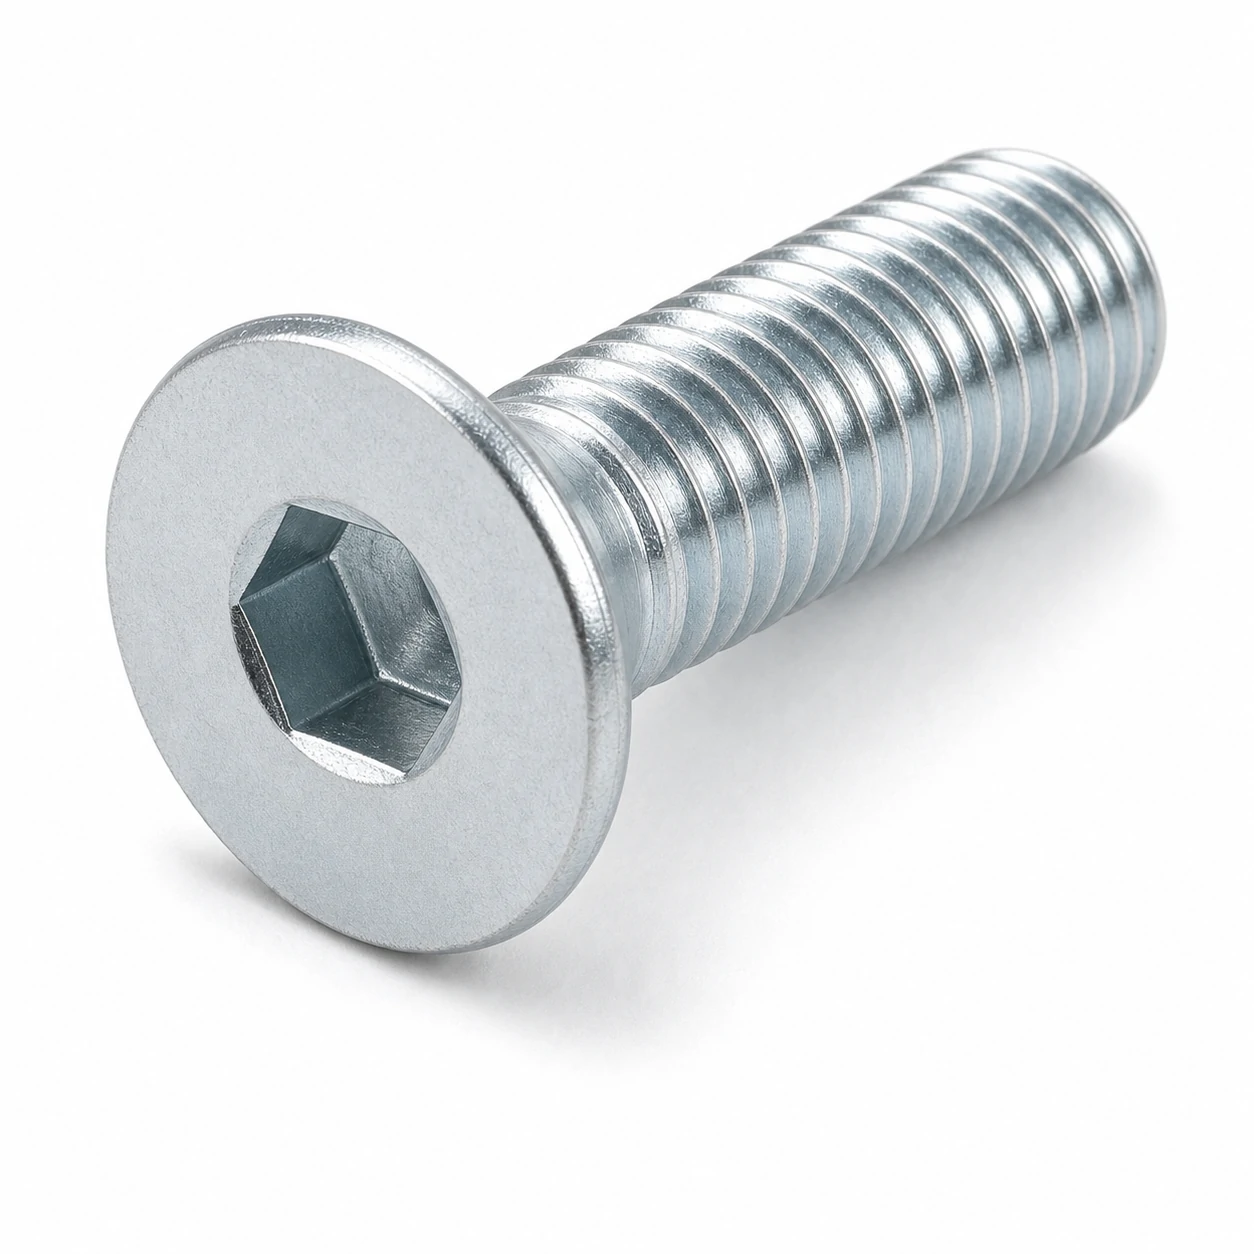
M20 Countersunk Socket Screws are manufactured to ISO 10642 / DIN 7991 with a coarse thread pitch of 2.5 mm. This page lists the controlling dimensions for the M20 size — head geometry, width across flats, matching spanner size — together with the clearance hole, tapping drill and tightening torque used at assembly.
M20 Dimensional Row (ISO 10642 / DIN 7991)
| Size | Pitch (mm) | Head diameter dk (mm) | Head height k (mm) | Hex key s (mm) | Countersink angle (deg) | Reference standard |
|---|---|---|---|---|---|---|
| M20 | 2.5 | 40.32 | 11.2 | 12.0 | 90 | ISO 10642 / DIN 7991 |
Spanner & Drive for M20 Countersunk Socket Screws
The hex socket for M20 Countersunk Socket Screws is shown in the spec table — use the matching Allen / hex key (an ISO 2936 hex key set covers the full range). For a one-off, a T-handle key and a calibrated arm will do. For a batch, the only way to get the same preload twice is a torque-controlled driver.
Hole Sizes for M20
| Coarse-thread pitch (ISO 724) | 2.5 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 22 mm |
| Tapping drill, coarse thread | 17.5 mm |
Tightening Torque for M20
| Class 8.8 (dry, ~µ 0.125) | ≈ 420 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 598 Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 700 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M20
| Tensile stress area As (ISO 724) | 245 mm² |
|---|---|
| Proof load, class 8.8 | 147 kN |
| Proof load, class 10.9 | 203 kN |
| Proof load, class 12.9 | 237 kN |
| Min. ultimate tensile load, class 8.8 | 203 kN |
Proof load = tensile stress area × the proof stress Sp of the class, per ISO 898-1 — Sp is a lower figure than the yield stress Rp0.2 and the two are not interchangeable. The stress area is computed from this size's own diameter and pitch, so a fine-pitch designation gives the fine-pitch figure. Design the joint so the working preload stays below the proof load of the class selected.
Mating Parts for M20
For M20, pair with a M20 hex nut (ISO 4032 / DIN 934) and, where used, a M20 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
When to Step Up or Down from M20
When the joint preload approaches the proof load of M20 class 8.8, step up to M24 class 8.8 (or move to M20 class 10.9). When the joint is over-specified, M16 often saves weight and cost without losing the safety margin.
Custom manufacturing · Made to drawing
Need countersunk socket screws in a size this table does not list?
This page covers M20 countersunk socket screws. Head form and drive can be specified to the assembly rather than to a standard: a larger bearing face, a security drive, or a socket sized for the tool already on the bench. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.