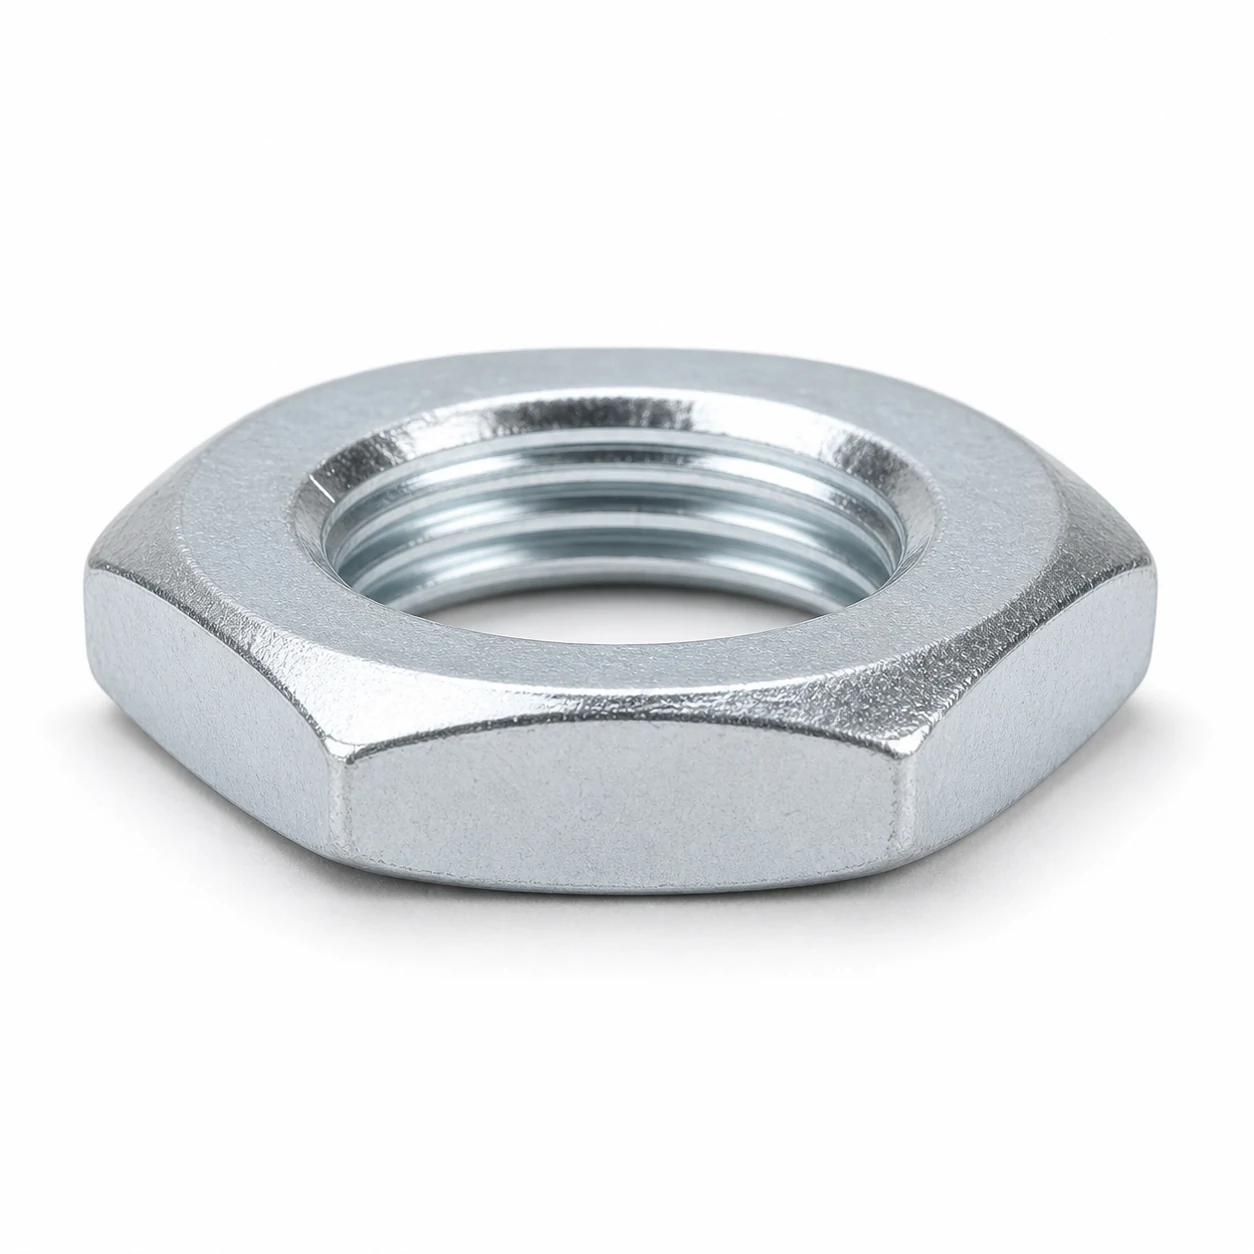
M3 Thin Hex Nuts are manufactured to ISO 4035. This page lists the controlling dimensions for the M3 size together with the drive and the installation notes for this type.
Values are taken from the governing standard rather than from a general machine-thread table, because this type is not selected on one.
M3 Dimensional Row (ISO 4035)
| Size | Pitch (mm) | Width across flats s (mm) | Width across corners e min (mm) | Nut height m (mm) | Reference standard |
|---|---|---|---|---|---|
| M3 | 0.5 | 5.5 | 6.01 | 1.8 | ISO 4035 / DIN 439 |
Spanner & Drive for M3 Thin Hex Nuts
M3 Thin Hex Nuts have a width across flats of 5.5 mm — fit a 5.5 mm open-ended spanner or socket. In tight access a 6-point socket on the 5.5 mm flats gives the most engagement per degree of swing. Where the joint is torqued to a figure, a click wrench is the only way to reproduce it across a batch.
Tightening Torque for M3
| Class 8.8 (dry, ~µ 0.125) | ≈ 1.3 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 2.2 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M3
Nuts are graded to ISO 898-2 by the proof load the nut itself will hold (classes 04, 05, 5, 6, 8, 10 and 12), not by the 8.8 / 10.9 / 12.9 scale used for bolts. A class-8 nut is the correct mate for a class-8.8 bolt, and the joint is designed on the bolt, so no bolt-tension figure is quoted here.
Mating Parts for M3
Pair M3 with the matching M3 bolt or screw, plus a M3 flat washer where required to distribute load on softer materials.
When to Step Up or Down from M3
When the joint preload approaches the proof load of M3 class 8.8, step up to M4 class 8.8 (or move to M3 class 10.9). When the joint is over-specified, M2 often saves weight and cost without losing the safety margin.
Custom manufacturing · Made to drawing
Need thin hex nuts in a size this table does not list?
This page covers M3 thin hex nuts. Height and across-flats are the two most often changed — a thinner nut for clearance, a larger hex for a tool that is already on the line. Made by cold heading or tapping.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.