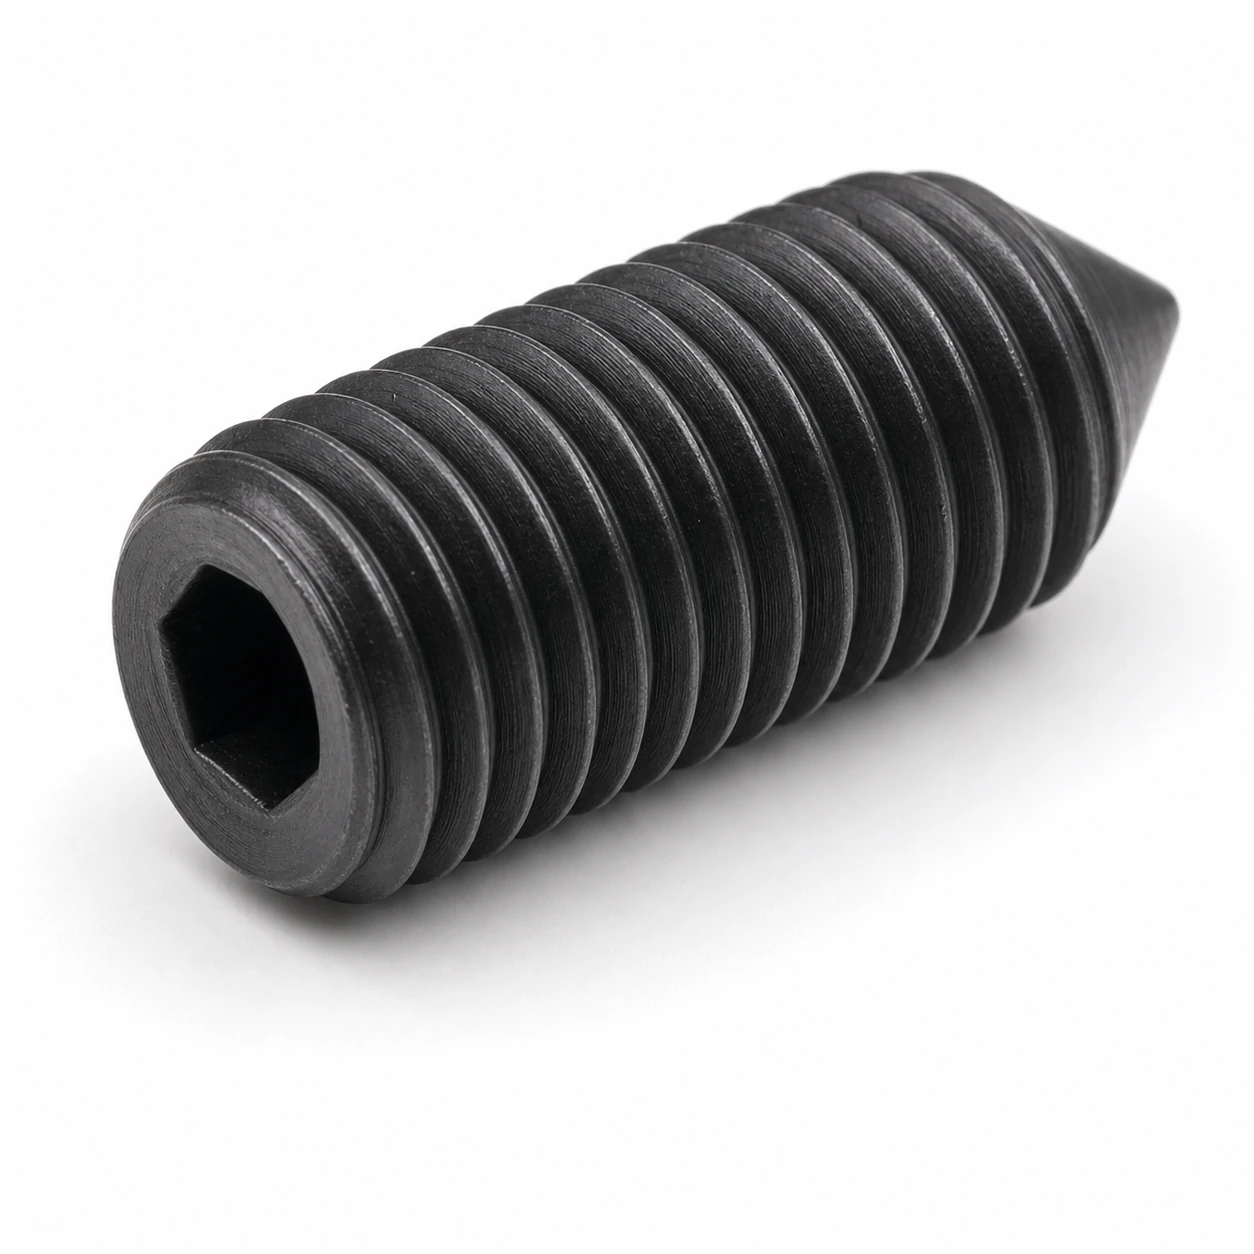
Dimensional and assembly data for M48 Socket Set Screws to ISO 4026 / ISO 4029 / DIN 913-916. Includes head size and width across flats, clearance-hole and tapping-drill diameters, tightening torque per property class, and the sizes to step up or down to when the joint requires it.
M48 Dimensional Row (ISO 4026 / ISO 4029 / DIN 913-916)
| Size | Pitch (mm) | Hex socket s (mm) | Engagement depth t min (mm) | Point diameter dp (mm) | End type | Reference standard |
|---|---|---|---|---|---|---|
| M48 | 5.0 | 22.0 | 28.0 | 36.0 | Flat point | ISO 4026 / DIN 913-916 |
Spanner & Drive for M48 Socket Set Screws
The hex socket for M48 Socket Set Screws is shown in the spec table — use the matching Allen / hex key (an ISO 2936 hex key set covers the full range). For a one-off, a T-handle key and a calibrated arm will do. For a batch, the only way to get the same preload twice is a torque-controlled driver.
Hole Sizes for M48
| Coarse-thread pitch (ISO 724) | 5 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 52 mm |
| Tapping drill, coarse thread | 43 mm |
Tightening Torque for M48
| Class 8.8 (dry, ~µ 0.125) | ≈ Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M48
Set screws are rated to ISO 898-5 by hardness, because they work in compression against a shaft rather than in tension. ISO 898-1 excludes them, and a set screw has no head to preload against, so neither a property class nor a preload torque applies. Seating torque depends on the point form and the shaft material.
Installation Tips for M48 Socket Set Screws
- Use a quality Allen key fully seated in the socket — partial engagement is the most common cause of stripped sockets at this size.
- For countersunk and button-head variants, chamfer the through-hole to seat the head flush without preloading the head/shank fillet.
- At M48 the stretch in the bolt becomes the controlling factor — for critical joints, use angle-controlled or stretch-controlled tightening instead of pure torque.
Mating Parts for M48
For M48, pair with a M48 hex nut (ISO 4032 / DIN 934) and, where used, a M48 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
Custom manufacturing · Made to drawing
Need socket set screws in a size this table does not list?
This page covers M48 socket set screws. Where the standard stops, the drawing takes over: fine pitches, left-hand threads, partial threading, and property classes above the catalogued grade where material and heat treatment allow. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.