Skip to content
Screws · Trade series (micro machine screws) · Application guide

What Are Micro Thin-Head Phillips Machine Screws Used For?

Typical applications, the industries that specify micro thin-head phillips machine screws, and how to choose the right size, material and finish for the joint.

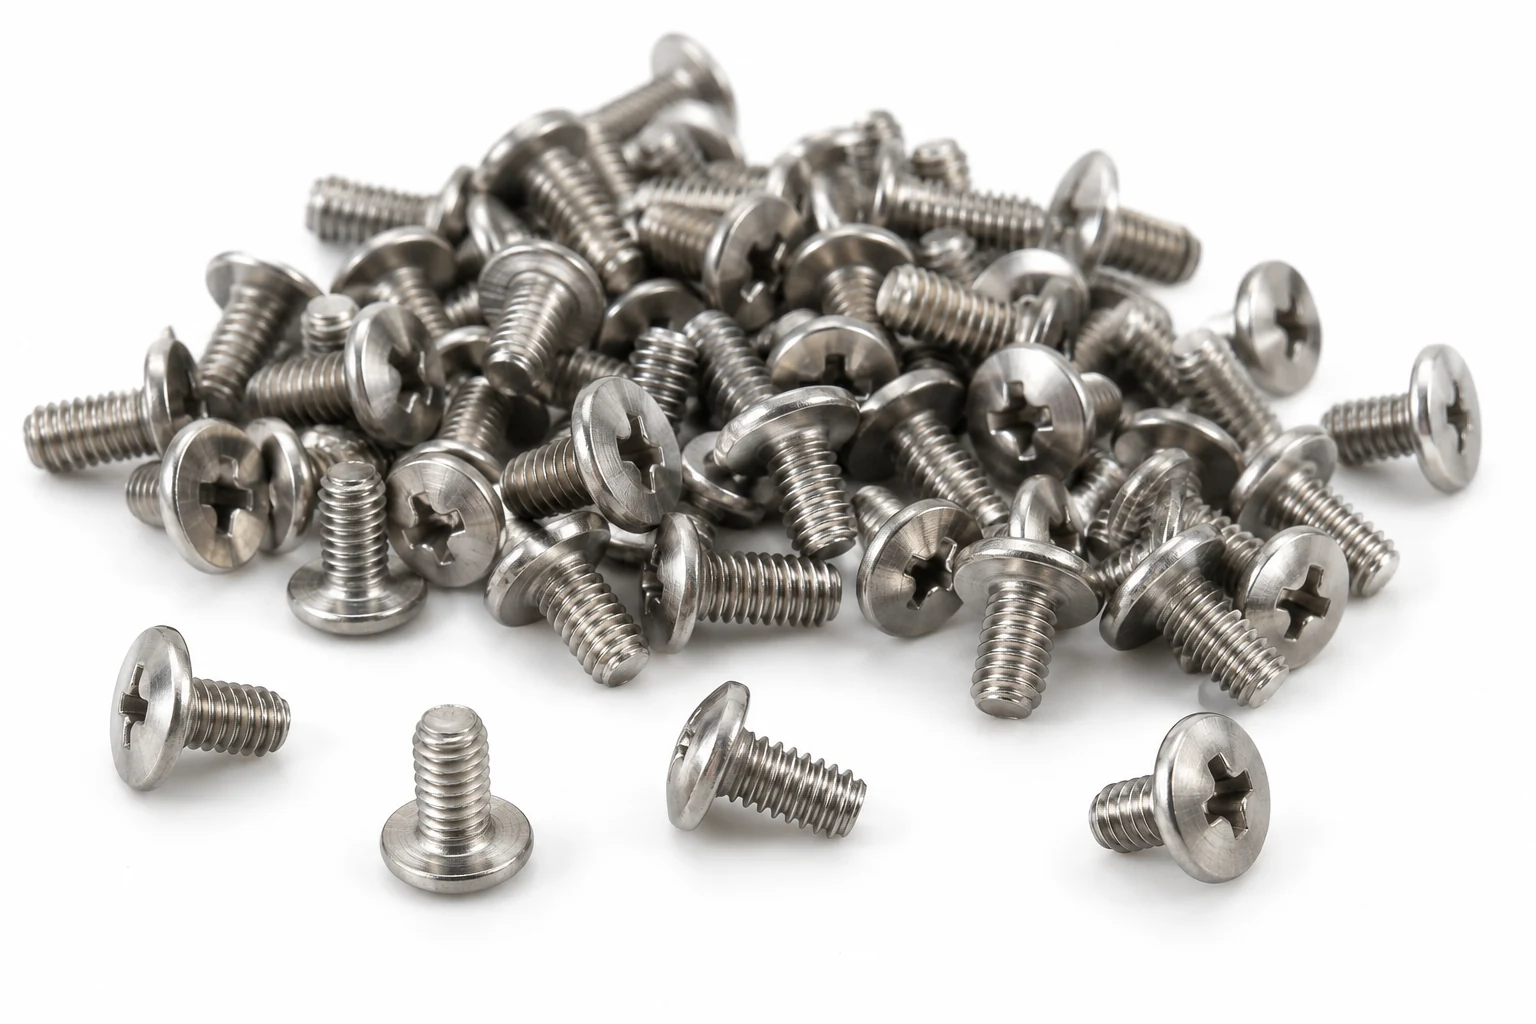
Micro Thin-Head Phillips Machine Screws are used for holding a thin cover where a conventional screw head would exceed the available clearance. They are manufactured to Trade series (micro machine screws), and the choice of size, property class and finish is driven by the load in the joint and the environment it sits in.

Primary duty
Holding a thin cover where a conventional screw head would exceed the available clearance
Governing standard
Trade series (micro machine screws)
Thread size range
M1.4 to M2.0
Category
Screws

Application notes are general engineering guidance. Verify the property class and any approval requirement against your own design calculation.

What Are Micro Thin-Head Phillips Machine Screws Used For? application image

Micro Thin-Head Phillips Machine Screws (Trade series (micro machine screws)) are specified where the joint requires holding a thin cover where a conventional screw head would exceed the available clearance. The sections below cover the typical end-uses by industry, the size and material decisions for each, assembly practice, and the applications this fastener type is not suited to. Stocked across roughly M1.4 to M2, they cover light-duty and instrument-scale work.

Typical Applications for Micro Thin-Head Phillips Machine Screws

The most common settings where these are specified:

  • Thin electronics: The 0.2 mm head thickness leaves clearance above miniature shields.
  • Sensors and optics: Low-profile Phillips hardware fits around lenses and adjustment mechanisms.
  • Compact mechanisms: Small heads secure covers where counterboring is not available.
  • Precision service: Short micro screws replace damaged hardware without adding head height.

How to Specify Micro Thin-Head Phillips Machine Screws for Your Application

  • Size: Match the nominal size to the mating thread or hole. This product spans M1.4–M2; check the full table below for the exact dimensions of each size.
  • Drive & head: Pick the drive (socket, cross, slot) and head style for the tool access and seating surface; a recessed drive resists cam-out under power tools.
  • Environment: For damp, coastal or chemical exposure prefer A4/316 stainless or a suitable coating; indoors, plated steel or A2 is usually sufficient.
  • Standard: This product is supplied to Trade series (micro machine screws). Quoting the standard on your order guarantees interchangeable dimensions between suppliers.

Installation & Assembly Practice

  • Match the driver exactly to the recess (PH ≠ PZ; hex key sizes per ISO 2936) and keep the tool axial — side load is the main cause of stripped drives.
  • In tapped holes, engage a thread length of at least 1× the nominal diameter in steel, 2× in aluminum.
  • Set power tools to a torque that seats the head without embedding it into the mating surface.

Common Selection Mistakes with Micro Thin-Head Phillips Machine Screws

  • Under-sizing the drive for the installation torque — a small recess at high torque strips before the screw is seated.
  • Using a countersunk head in thin sheet where the countersink removes most of the load-bearing material.
  • Specifying stainless in high-strength duty: A2-70 is roughly class 7 steel, not a 10.9 substitute.

Where Micro Thin-Head Phillips Machine Screws Are Not the Right Choice

Not for high-preload structural joints (use a property-class bolt and nut), and not in thin sheet where a self-drilling or self-tapping type suits better.
Technical Drawing

Customize the parameters below — every spec field is editable, and the drawing redraws to match the values you choose. Changing the size will snap the other fields to that size's standard values; you can then override any individual value.

Sends the selected values to the quote form below.

Request a Quote

The form below follows the current technical drawing configuration. Change the drawing values above and the request details update automatically.

Request a Quotation

Specification
Business Information

Dimensions & Specifications (Trade series (micro machine screws))

Thread sizeHead diameter (mm)Head thickness (mm)Typical length range (mm)DriveMaterial options
M1.42.50.22~10miniature Phillipssteel / stainless steel / brass
M1.62.80.22~10miniature Phillipssteel / stainless steel / brass
M1.73.00.22~10miniature Phillipssteel / stainless steel / brass
M2.03.50.22~10miniature Phillipssteel / stainless steel / brass
Inside the plant

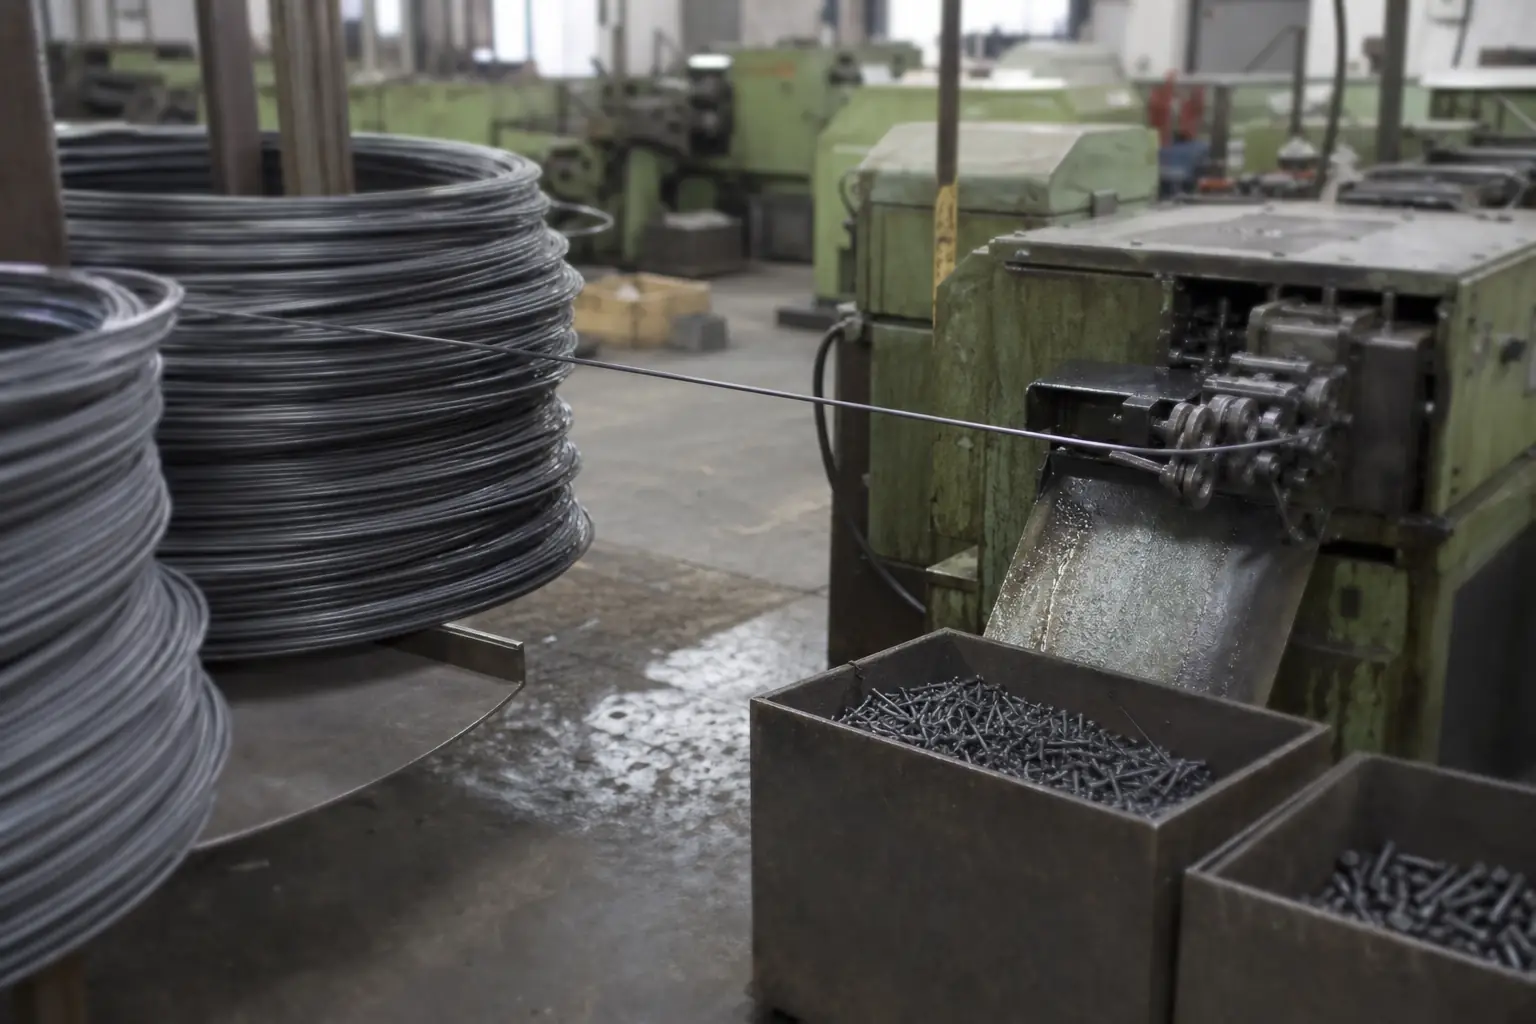
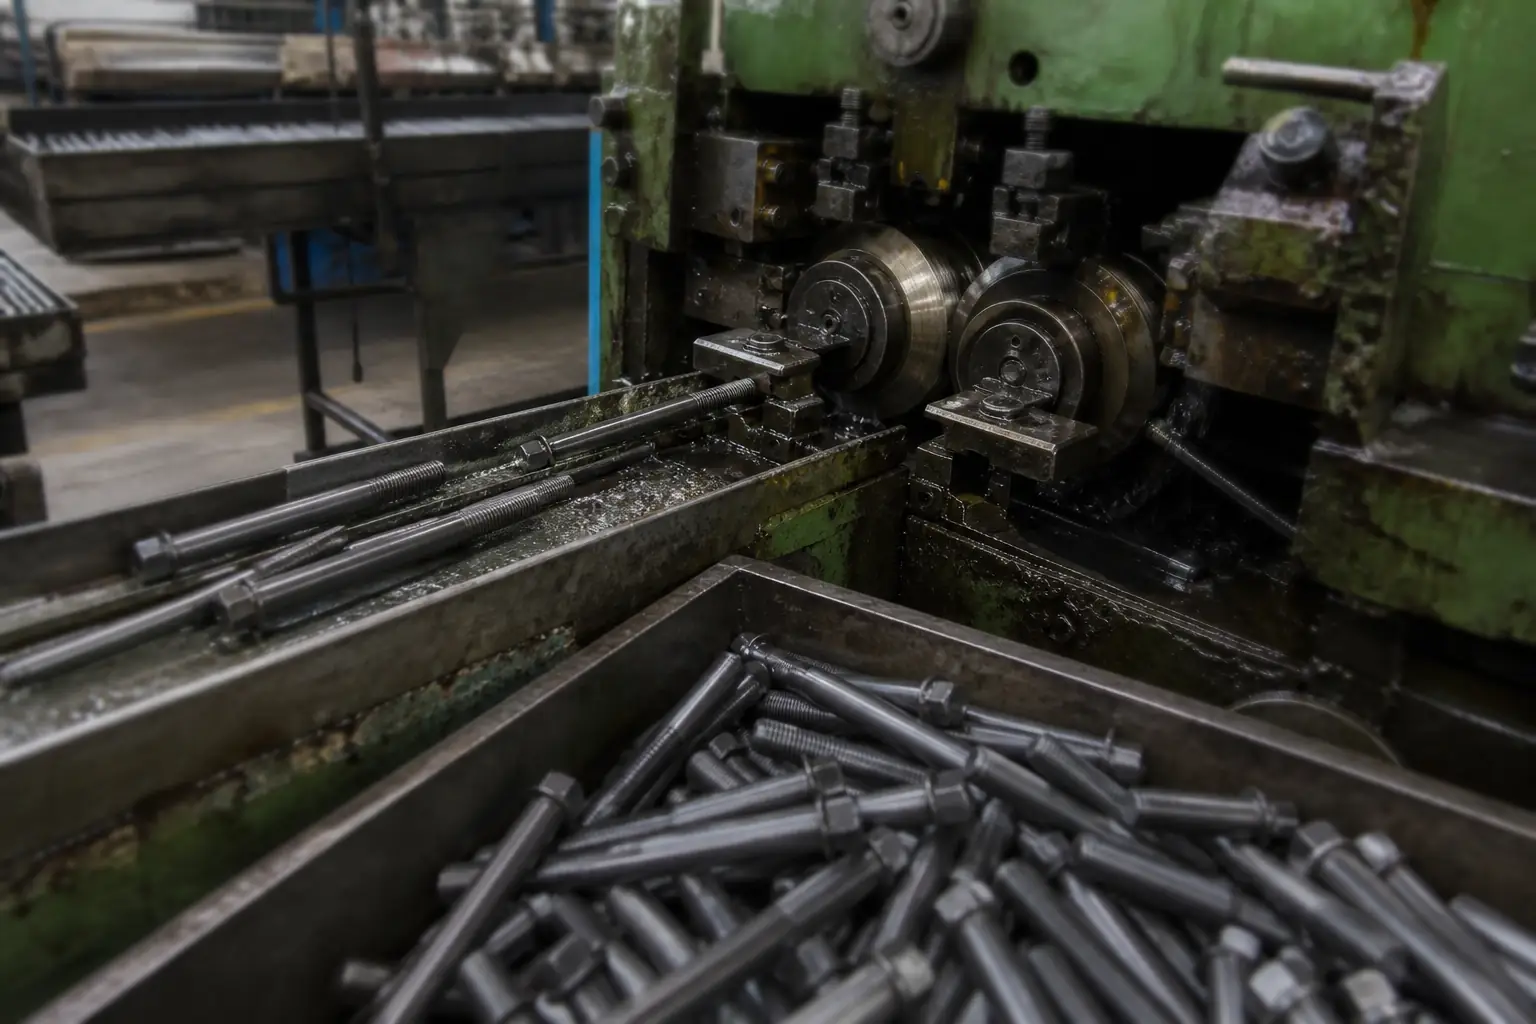
Manufactured in our own plant

This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.

  1. Wire rod feeding into a cold heading machine
    01

    Cold heading

    Wire rod is drawn to size and cold-formed into blanks. Forming rather than cutting keeps the grain flow continuous around the head, which is where a bolt is most likely to fail.

    Head dimensions and under-head radius checked at set-up and per shift.

  2. Thread rolling machine producing bolt threads
    02

    Thread rolling

    Threads are rolled between hardened dies rather than cut. Rolled threads are stronger in fatigue than cut threads and hold pitch and flank angle far more consistently across a batch.

    Go / no-go ring gauges to ISO 965 tolerance class 6g.

  3. Baskets of bolts staged for heat treatment
    03

    Heat treatment

    Quench-and-temper brings carbon and alloy steel to the property class ordered — 8.8, 10.9 or 12.9 — with the furnace charge tracked so a finished lot can be traced back to it.

    Core hardness and tensile tested per lot to ISO 898-1.

  4. Zinc plated bolts in a treatment basket
    04

    Surface treatment

    Zinc, zinc-nickel, hot-dip galvanizing, black oxide, phosphate and Dacromet, selected against the service environment rather than against the price list.

    Coating thickness and neutral salt spray hours to ISO 9227.

Frequently Asked Questions

What are Micro Thin-Head Phillips Machine Screws used for?

Holding a thin cover where a conventional screw head would exceed the available clearance. They are supplied to Trade series (micro machine screws).

Which industries use Micro Thin-Head Phillips Machine Screws?

They are commonly specified in thin electronics, sensors and optics and compact mechanisms, among other sectors.

How do I choose the right size of Micro Thin-Head Phillips Machine Screws?

Match the nominal size to the mating thread or hole. This product is available from M1.4 to M2; the full dimension table on this page lists each size.

What drive type do Micro Thin-Head Phillips Machine Screws use?

Drive depends on the head style — socket (hex key), cross (Phillips/Pozi) or slot. A recessed drive resists cam-out when driven with power tools; check the product head style on this page.

Can I get a quote for Micro Thin-Head Phillips Machine Screws in the size and material I need?

Yes. Use the technical drawing and quote form on this page to set the size and options, then send the exact configuration to our team for pricing and lead time.