Seals · Trade series (anaerobic adhesives for threaded assemblies)
EPDM Anaerobic Threadlockers and Thread Sealants
Temperature range, chemical and fluid compatibility, hardness and the full dimensional range for this compound.
EPDM Anaerobic Threadlockers and Thread Sealants are supplied to ethylene-propylene-diene rubber, typically 70 Shore A. Corrosion behaviour is excellent in water, steam, brake fluid and weathering; unsuitable for mineral oil, the material is non-magnetic, and the usable service range is approx. -45 °C to +150 °C. In practice this grade is the water, steam and outdoor-weathering elastomer.
Grade
ethylene-propylene-diene rubber, typically 70 Shore A
Corrosion resistance
Excellent in water, steam, brake fluid and weathering; unsuitable for mineral oil
Magnetic response
Non-magnetic
Service temperature
approx. -45 °C to +150 °C
Property values are typical for the grade. Certified mechanical test data is available on request for production orders.
Hidden Deck Fasteners Sourcing: Manufacturing, Types & Material Compatibility
Material specification page for anaerobic threadlockers and thread sealants in EPDM. Covers the grade designation (ethylene-propylene-diene rubber, typically 70 Shore A), corrosion and magnetic behavior, comparable grades and their trade-offs, and the sizes available to Trade series (anaerobic adhesives for threaded assemblies).
Why Choose EPDM for Anaerobic Threadlockers and Thread Sealants
The water, steam and outdoor-weathering elastomer. For anaerobic threadlockers and thread sealants, this matters when excellent in water, steam, brake fluid and weathering; unsuitable for mineral oil is the primary requirement.
Mechanical & Physical Properties
Grade designation
ethylene-propylene-diene rubber, typically 70 Shore A
Magnetic response
Non-magnetic
Service temperature
approx. -45 °C to +150 °C
Corrosion characteristic
Excellent in water, steam, brake fluid and weathering; unsuitable for mineral oil
Corrosion Behavior in Service
Carbon and alloy steel anaerobic threadlockers and thread sealants require a coating for corrosion protection. Zinc plating (with or without passivation) is the most common; hot-dip galvanizing is used for outdoor structural service; black-oxide is mainly a tarnish-prevention finish for tool-room use.
Comparable Grades
For anaerobic threadlockers and thread sealants, consider NBR for mineral oil and hydraulic service, which EPDM does not tolerate, or silicone for a wider temperature range in static duty. Elastomer selection is decided by the medium, the temperature range and whether the seal is static or dynamic — not by strength.
Sizes of Anaerobic Threadlockers and Thread Sealants Available in EPDM
Grade
Removal
Typical use
Notes
low strength
hand tools
set screws, adjusting screws, small fasteners
up to about M12
medium strength
hand tools
general assembly, machine screws
the usual default
high strength
heat and hand tools
studs, permanent assemblies
not for parts serviced in the field
thread sealant grade
hand tools
tapered pipe threads, hydraulic fittings
seals rather than locks
retaining compound
heat
bearings, bushes, cylindrical fits
not a thread product
Technical Drawing
Customize the parameters below — every spec field is editable, and the drawing redraws to match the values you choose. Changing the size will snap the other fields to that size's standard values; you can then override any individual value.
Sends the selected values to the quote form below.
Request a Quote
The form below follows the current technical drawing configuration. Change the drawing values above and the request details update automatically.
Dimensions & Specifications (Trade series (anaerobic adhesives for threaded assemblies))
Grade
Removal
Typical use
Notes
low strength
hand tools
set screws, adjusting screws, small fasteners
up to about M12
medium strength
hand tools
general assembly, machine screws
the usual default
high strength
heat and hand tools
studs, permanent assemblies
not for parts serviced in the field
thread sealant grade
hand tools
tapered pipe threads, hydraulic fittings
seals rather than locks
retaining compound
heat
bearings, bushes, cylindrical fits
not a thread product
Applications & Industries
Anaerobic Threadlockers and Thread Sealants are bought for a small number of well-defined jobs. These are the ones we ship them for. Stocked from low strength to retaining compound (inside diameter).
Industries that specify Anaerobic Threadlockers and Thread Sealants
Field maintenanceSecuring set screws.
Machine assemblyFasteners that must not loosen.
AutomotiveVibration-prone joints.
HydraulicsTapered thread sealing.
Process & food equipmentSealing at joints that are cleaned and inspected.
Hydraulics & pneumaticsStatic and dynamic sealing in cylinders and valve bodies.
Typical applications
allowing the stated cure time before loading the joint
choosing the grade by how the joint will be serviced
degreasing both threads before applying
using a sealant grade rather than a locking grade on pipe threads
excluding dust and moisture from a housing
sealing a joint against fluid or air pressure
Service conditions to specify against
Sealed joints
Used where the fixing has to keep water or air out as well as hold — the elastomer, not the fastener, decides service life.
Vibration
Specified where cyclic load would loosen a plain nut or screw — rotating plant, rail, mobile equipment and anything that is not re-torqued in service.
Where to use something else
Do not use a high-strength grade on anything that will be serviced in the field; removing it needs heat, and heat is rarely available where the fastener has to come out.
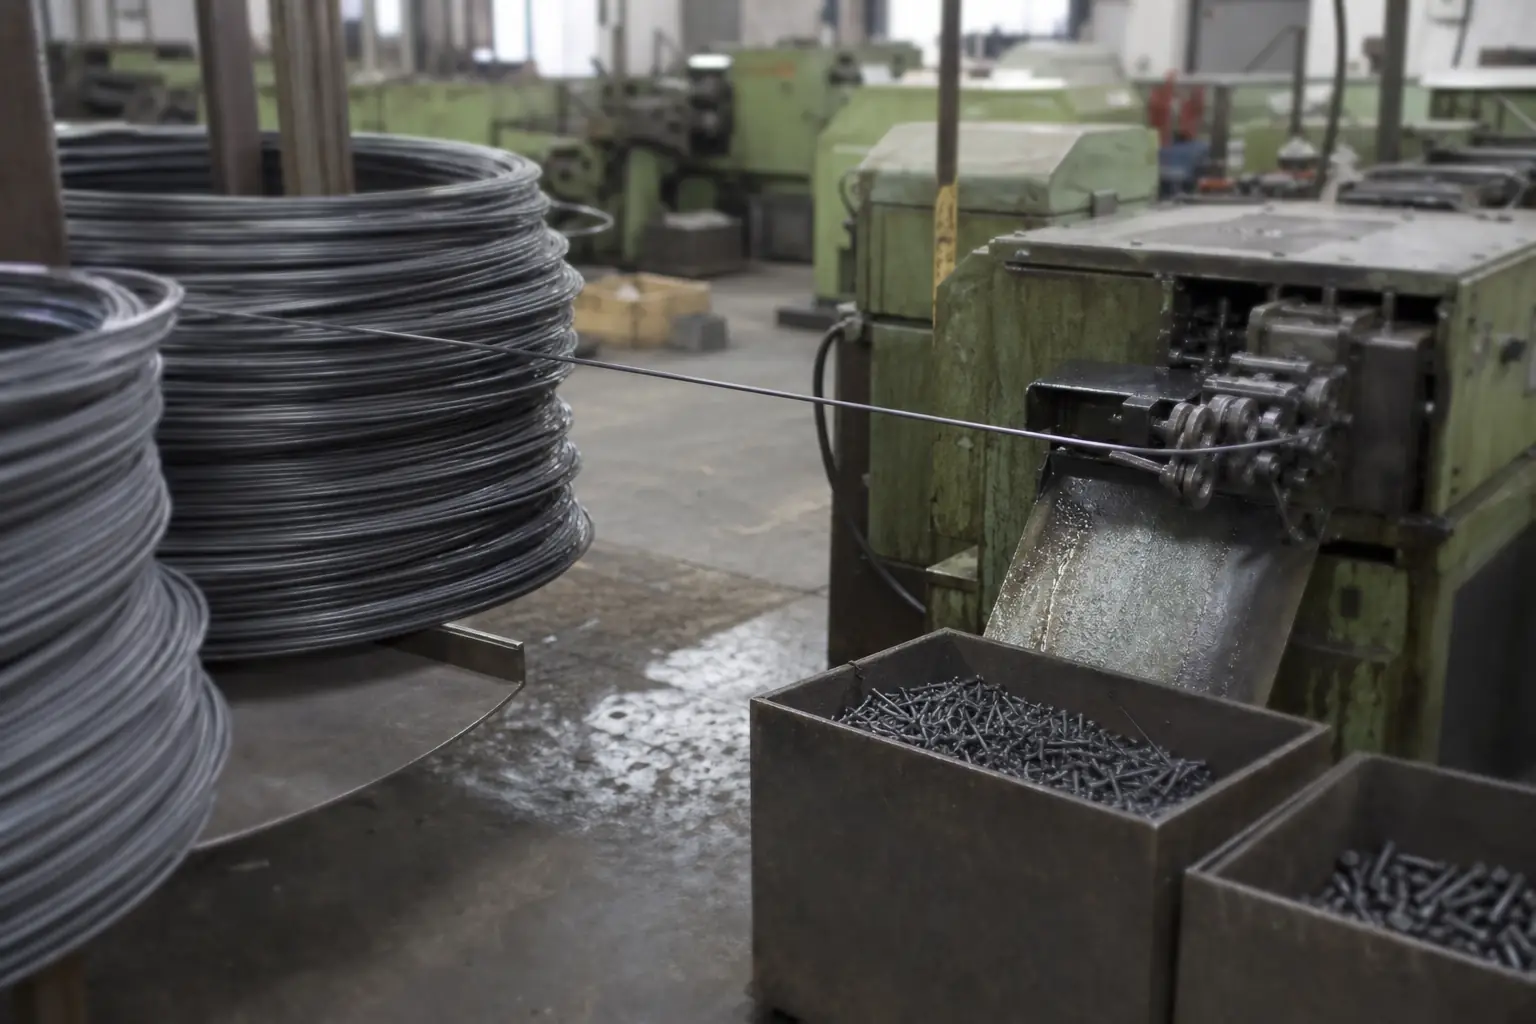
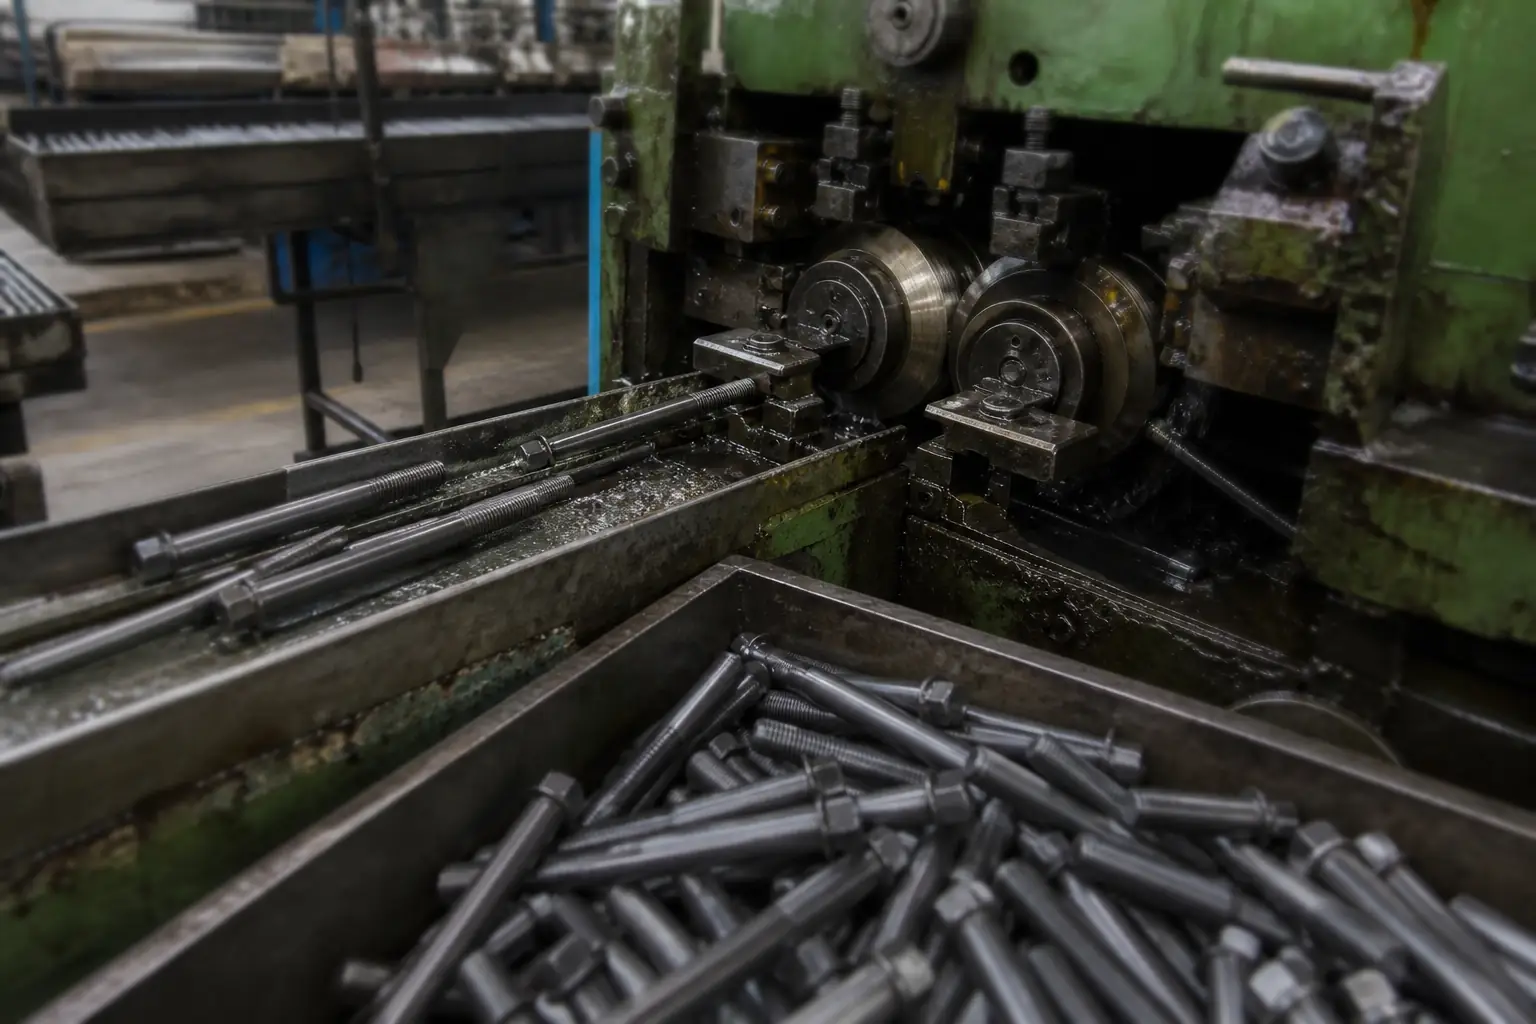
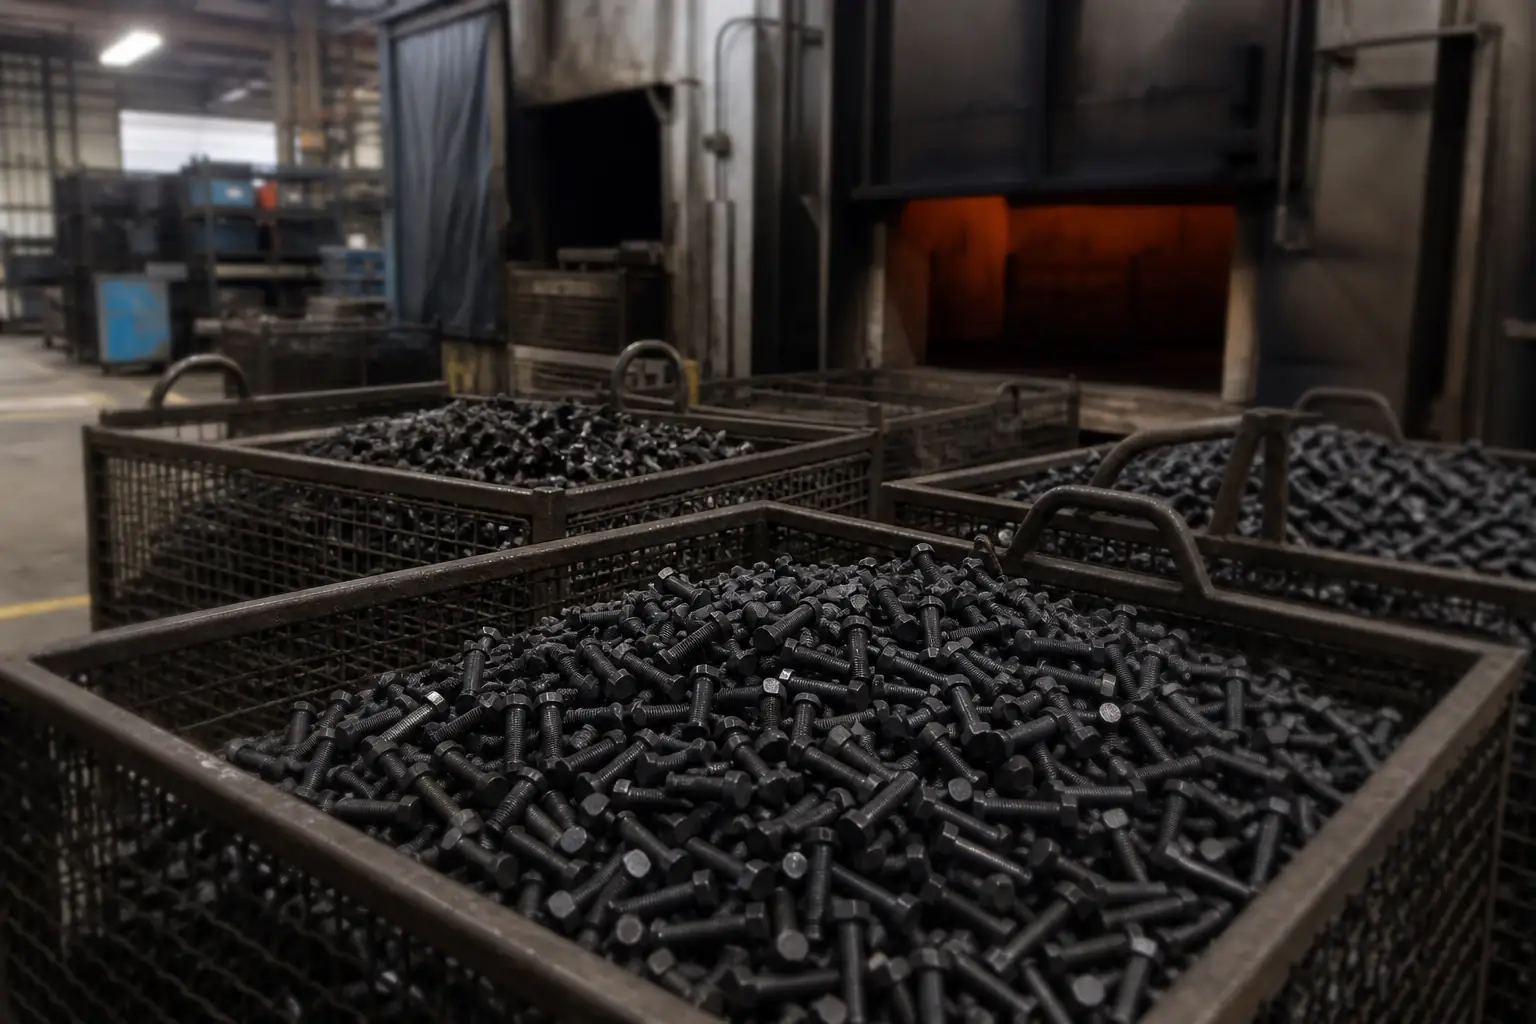
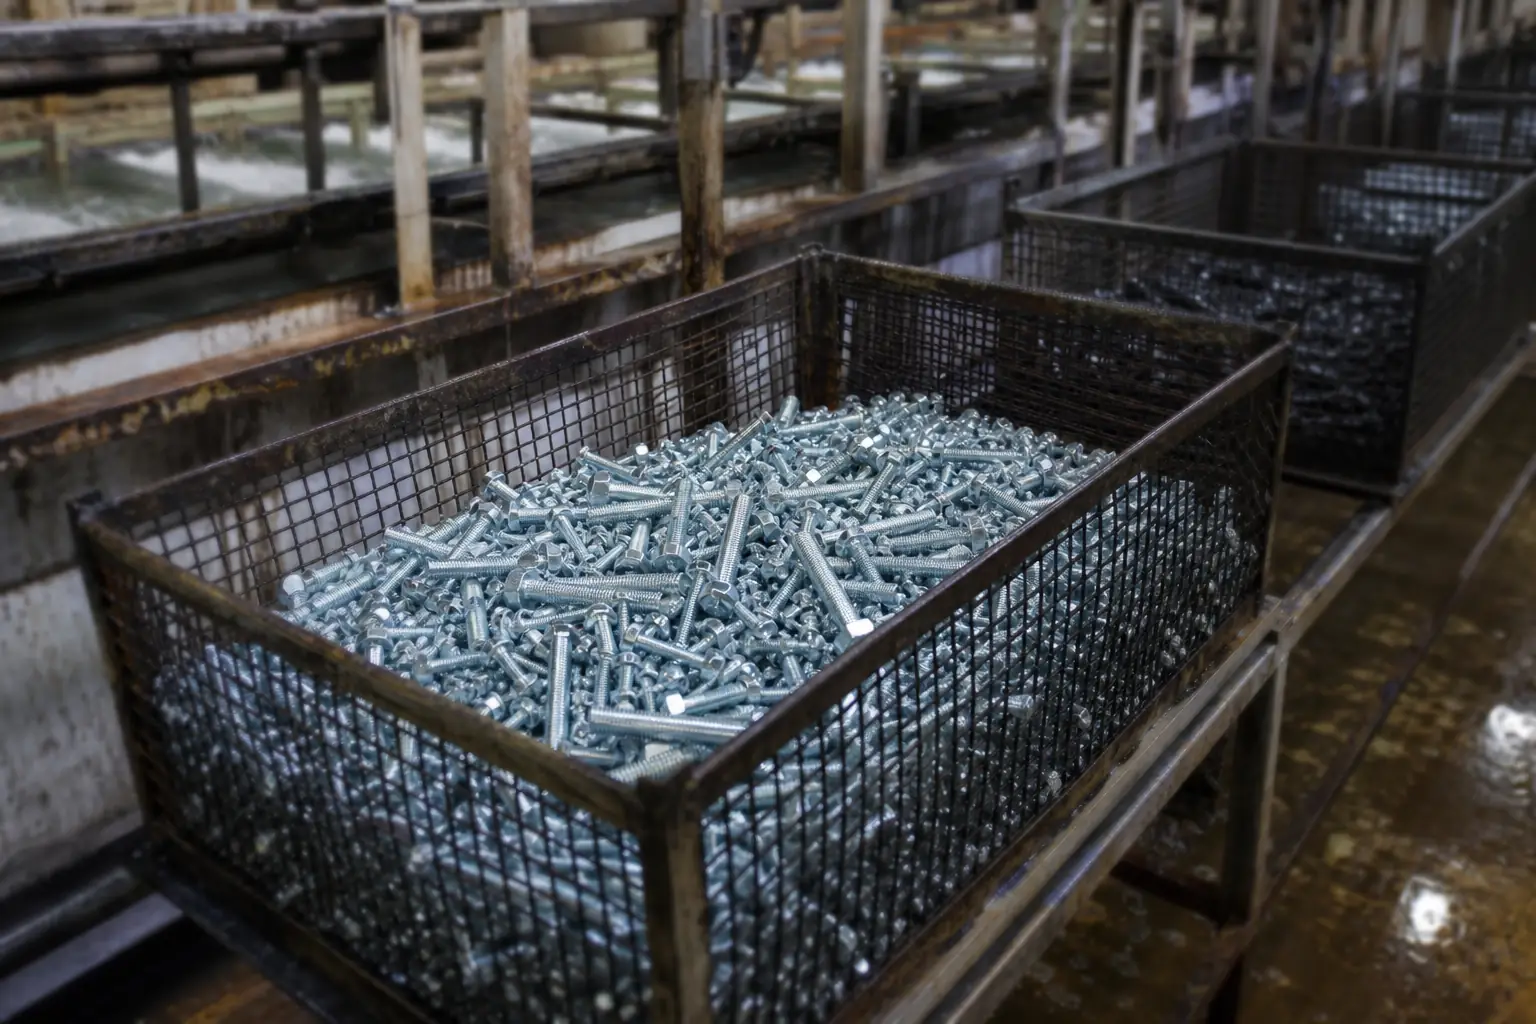
This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.
01
Cold heading
Wire rod is drawn to size and cold-formed into blanks. Forming rather than cutting keeps the grain flow continuous around the head, which is where a bolt is most likely to fail.
Head dimensions and under-head radius checked at set-up and per shift.
02
Thread rolling
Threads are rolled between hardened dies rather than cut. Rolled threads are stronger in fatigue than cut threads and hold pitch and flank angle far more consistently across a batch.
Go / no-go ring gauges to ISO 965 tolerance class 6g.
03
Heat treatment
Quench-and-temper brings carbon and alloy steel to the property class ordered — 8.8, 10.9 or 12.9 — with the furnace charge tracked so a finished lot can be traced back to it.
Core hardness and tensile tested per lot to ISO 898-1.
04
Surface treatment
Zinc, zinc-nickel, hot-dip galvanizing, black oxide, phosphate and Dacromet, selected against the service environment rather than against the price list.
Coating thickness and neutral salt spray hours to ISO 9227.
Frequently Asked Questions
What corrosion resistance do EPDM Anaerobic Threadlockers and Thread Sealants offer?
EPDM Anaerobic Threadlockers and Thread Sealants provide excellent in water, steam, brake fluid and weathering; unsuitable for mineral oil with a service range of approx. -45 °C to +150 °C.
When should I move from ethylene-propylene-diene rubber, typically 70 Shore A to class 8.8 for Anaerobic Threadlockers and Thread Sealants?
Step up to class 8.8 when the joint preload approaches the proof load of the current class. The higher class adds preload at the same diameter, often saving size and weight.
Is EPDM prone to hydrogen embrittlement?
Class 10.9 and above can be susceptible to hydrogen embrittlement when electroplated. Specify post-plating baking, or use mechanical-zinc / zinc-flake finishes which avoid the cathodic plating step.
Which finish is best for outdoor Anaerobic Threadlockers and Thread Sealants?
For outdoor service in steel, hot-dip galvanizing gives the longest life; zinc-flake (Geomet/Delta-Tone family) gives a thinner film with excellent salt-spray performance; standard zinc plating is the lowest-cost option for general indoor / shielded outdoor use.
How do I request a quotation?
Use the technical drawing on this page to pick the exact configuration, then submit it with the quote form. We respond within one business day.
This website uses only necessary and functional cookies to operate, secure, and improve basic website performance.
We do not use advertising cookies, Google Analytics, or cross-site tracking technologies.
Privacy Policy