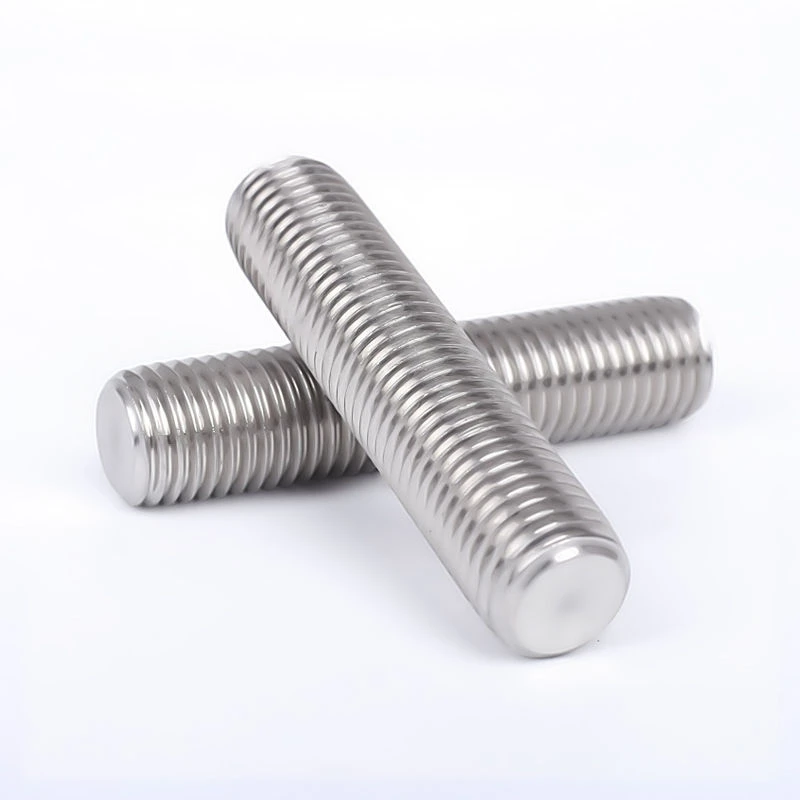
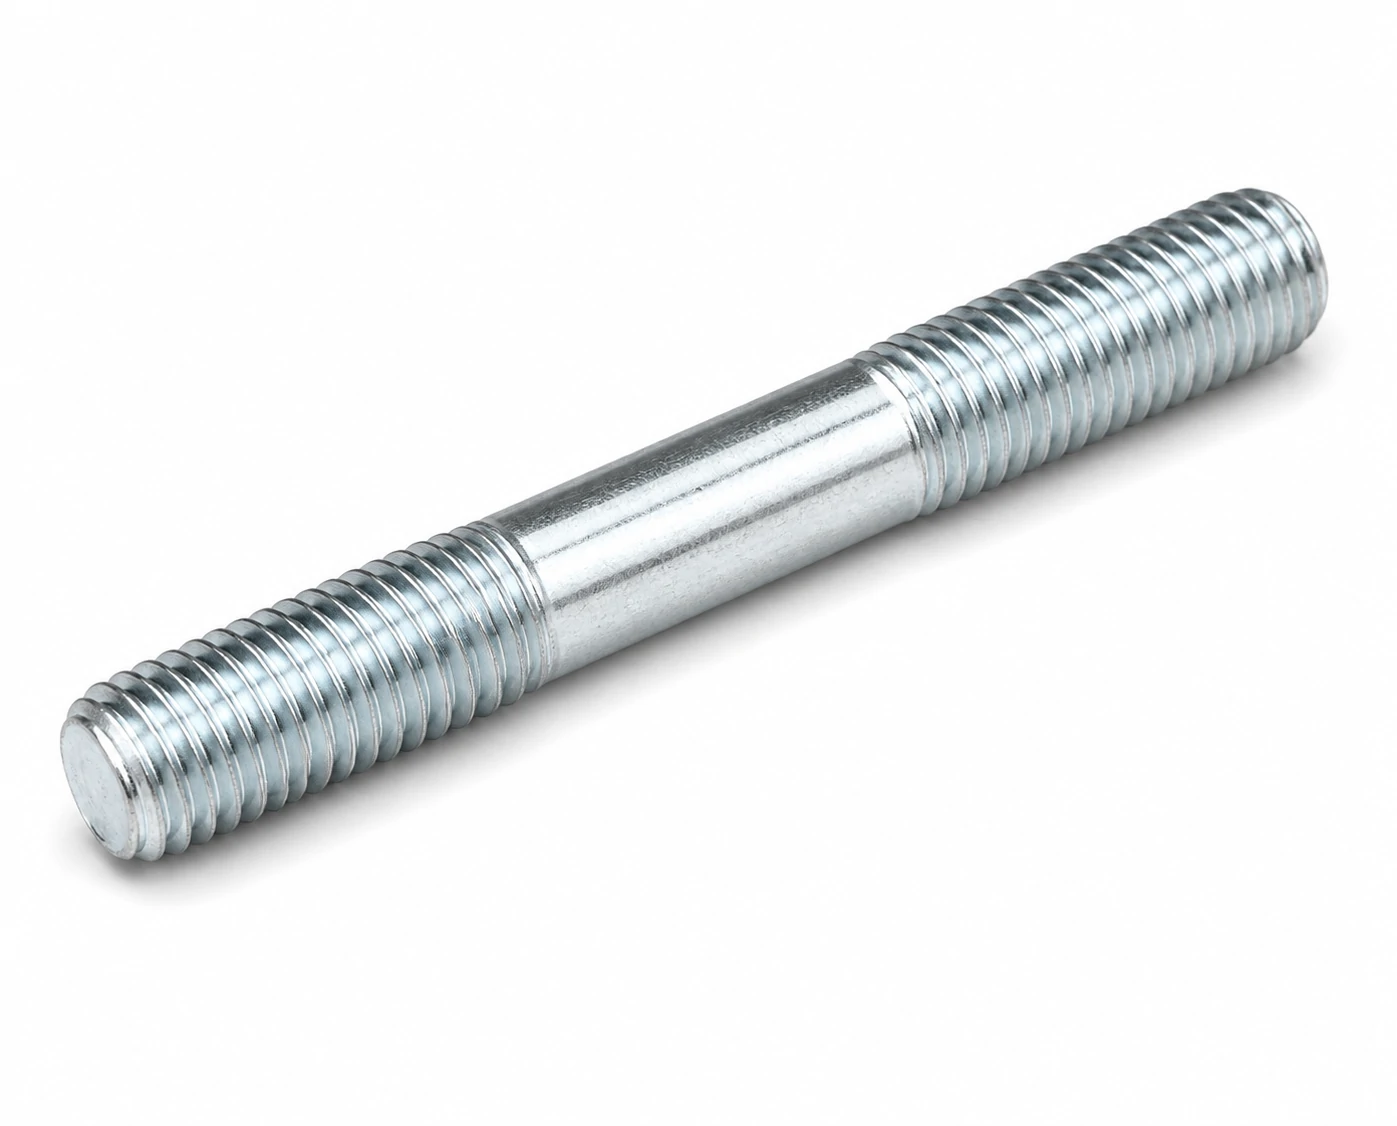
Dimensional and assembly data for M12 Double-End Studs (DIN 938 / 939 / 940) to DIN 938. Includes head size and width across flats, clearance-hole and tapping-drill diameters, tightening torque per property class, and the sizes to step up or down to when the joint requires it.
M12 Dimensional Row (DIN 938)
| Thread size | Metal end bm (mm) | For parent material | Nut end (mm) | Common overall length (mm) | Property class | Reference standard | Sibling standard |
|---|---|---|---|---|---|---|---|
| M12 | 12 | Steel | 12 | 40~120 | 8.8 | DIN 938 | DIN 939 = 15 mm, DIN 940 = 24 mm |
Hole Sizes for M12
| Coarse-thread pitch (ISO 724) | 1.75 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 13.5 mm |
| Tapping drill, coarse thread | 10.25 mm |
Tightening Torque for M12
| Class 8.8 (dry, ~µ 0.125) | ≈ 84 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 124 Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 145 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M12
| Tensile stress area As (ISO 724) | 84.3 mm² |
|---|---|
| Proof load, class 8.8 | 49 kN |
| Proof load, class 10.9 | 70 kN |
| Proof load, class 12.9 | 82 kN |
| Min. ultimate tensile load, class 8.8 | 67 kN |
Proof load = tensile stress area × the proof stress Sp of the class, per ISO 898-1 — Sp is a lower figure than the yield stress Rp0.2 and the two are not interchangeable. The stress area is computed from this size's own diameter and pitch, so a fine-pitch designation gives the fine-pitch figure. Design the joint so the working preload stays below the proof load of the class selected.
Mating Parts for M12
For M12, pair with a M12 hex nut (ISO 4032 / DIN 934) and, where used, a M12 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
When to Step Up or Down from M12
When the joint preload approaches the proof load of M12 class 8.8, step up to M16 class 8.8 (or move to M12 class 10.9). When the joint is over-specified, M10 often saves weight and cost without losing the safety margin.
Custom manufacturing · Made to drawing
Need double-end studs (din 938 / 939 / 940) in a size this table does not list?
This page covers M12 double-end studs (din 938 / 939 / 940). Dimensions, material, finish and form are specified from the drawing — a bolt outside the standard range is a variation on existing tooling rather than a new design. Made by cold heading or hot forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.