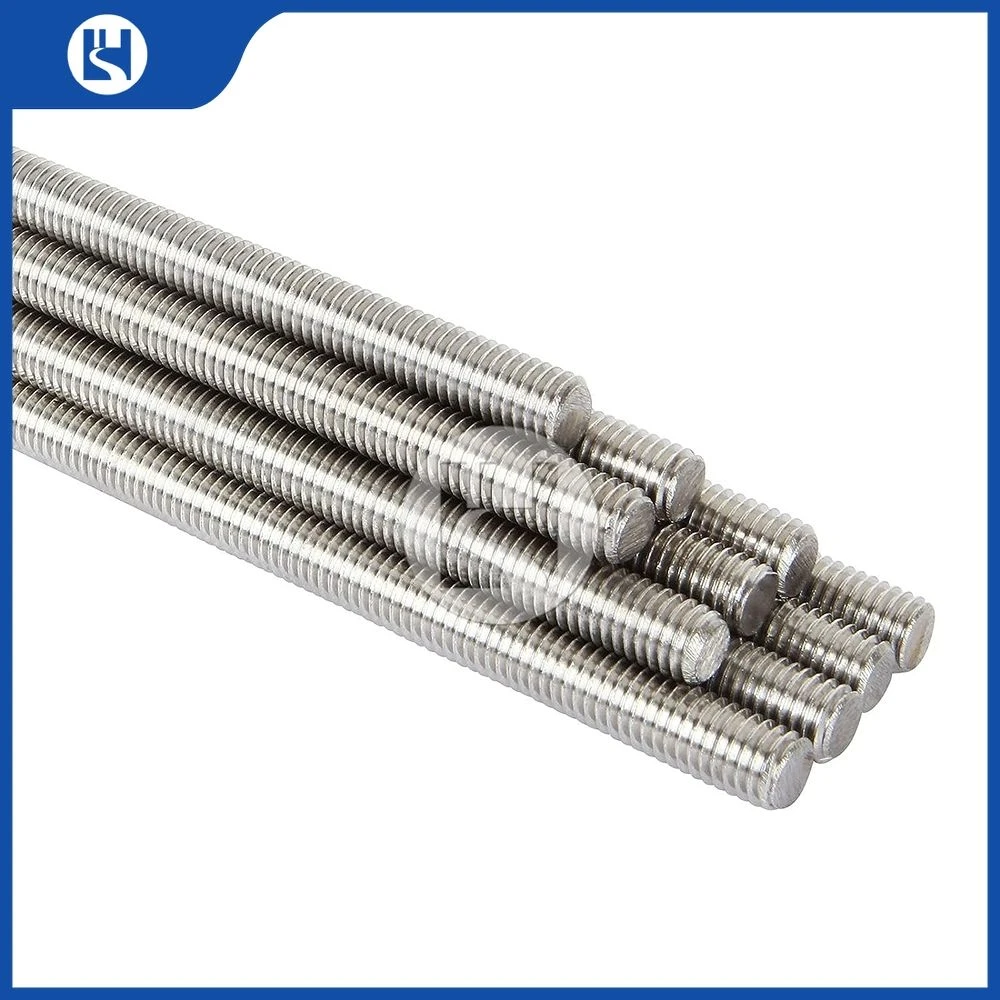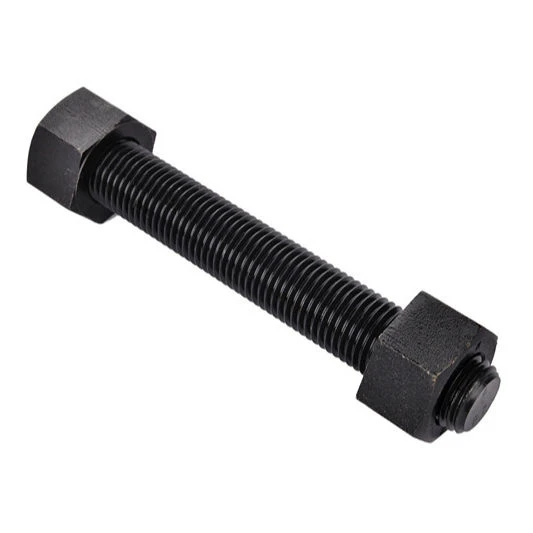
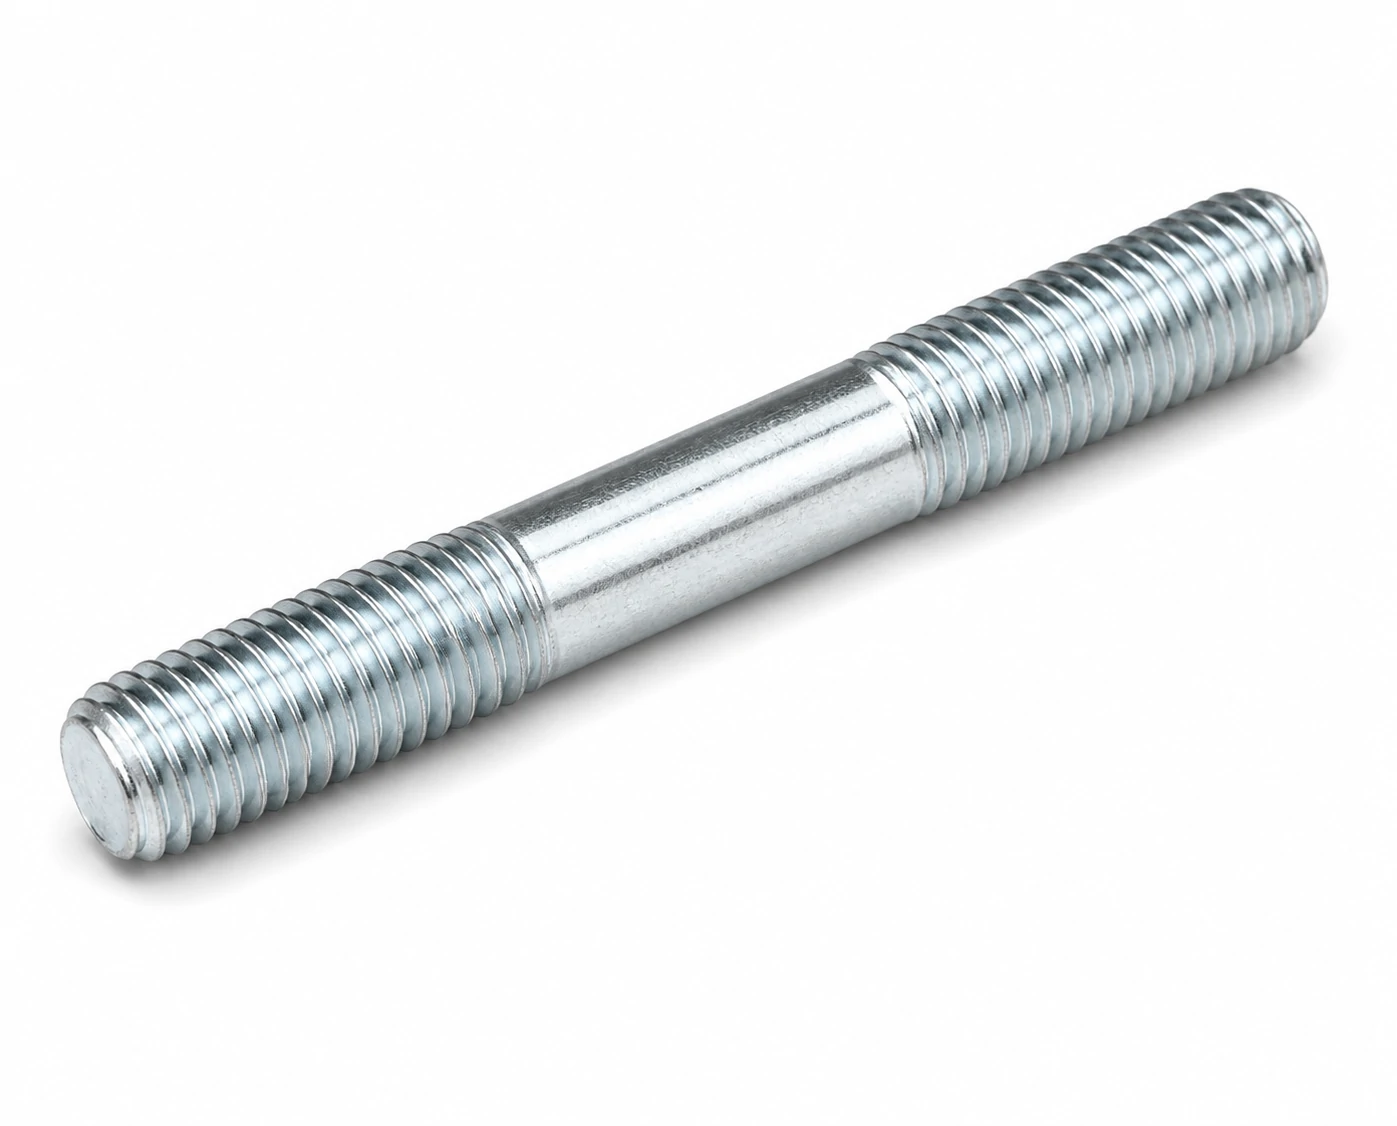
M24 Double-End Studs (DIN 938 / 939 / 940) are manufactured to DIN 938 with a coarse thread pitch of 3 mm. This page lists the controlling dimensions for the M24 size — head geometry, width across flats, matching spanner size — together with the clearance hole, tapping drill and tightening torque used at assembly.
M24 Dimensional Row (DIN 938)
| Thread size | Metal end bm (mm) | For parent material | Nut end (mm) | Common overall length (mm) | Property class | Reference standard | Sibling standard |
|---|---|---|---|---|---|---|---|
| M24 | 24 | Steel | 24 | 70~240 | 8.8 | DIN 938 | DIN 939 = 30 mm, DIN 940 = 48 mm |
Hole Sizes for M24
| Coarse-thread pitch (ISO 724) | 3 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 26 mm |
| Tapping drill, coarse thread | 21 mm |
Tightening Torque for M24
| Class 8.8 (dry, ~µ 0.125) | ≈ 726 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 1034 Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 1210 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M24
| Tensile stress area As (ISO 724) | 353 mm² |
|---|---|
| Proof load, class 8.8 | 212 kN |
| Proof load, class 10.9 | 293 kN |
| Proof load, class 12.9 | 342 kN |
| Min. ultimate tensile load, class 8.8 | 293 kN |
Proof load = tensile stress area × the proof stress Sp of the class, per ISO 898-1 — Sp is a lower figure than the yield stress Rp0.2 and the two are not interchangeable. The stress area is computed from this size's own diameter and pitch, so a fine-pitch designation gives the fine-pitch figure. Design the joint so the working preload stays below the proof load of the class selected.
Mating Parts for M24
For M24, pair with a M24 hex nut (ISO 4032 / DIN 934) and, where used, a M24 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
Custom manufacturing · Made to drawing
Need double-end studs (din 938 / 939 / 940) in a size this table does not list?
This page covers M24 double-end studs (din 938 / 939 / 940). A non-standard bolt is quoted from the drawing; where one already exists in the catalog, the special is usually a variation on its tooling. Made by cold heading or hot forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.