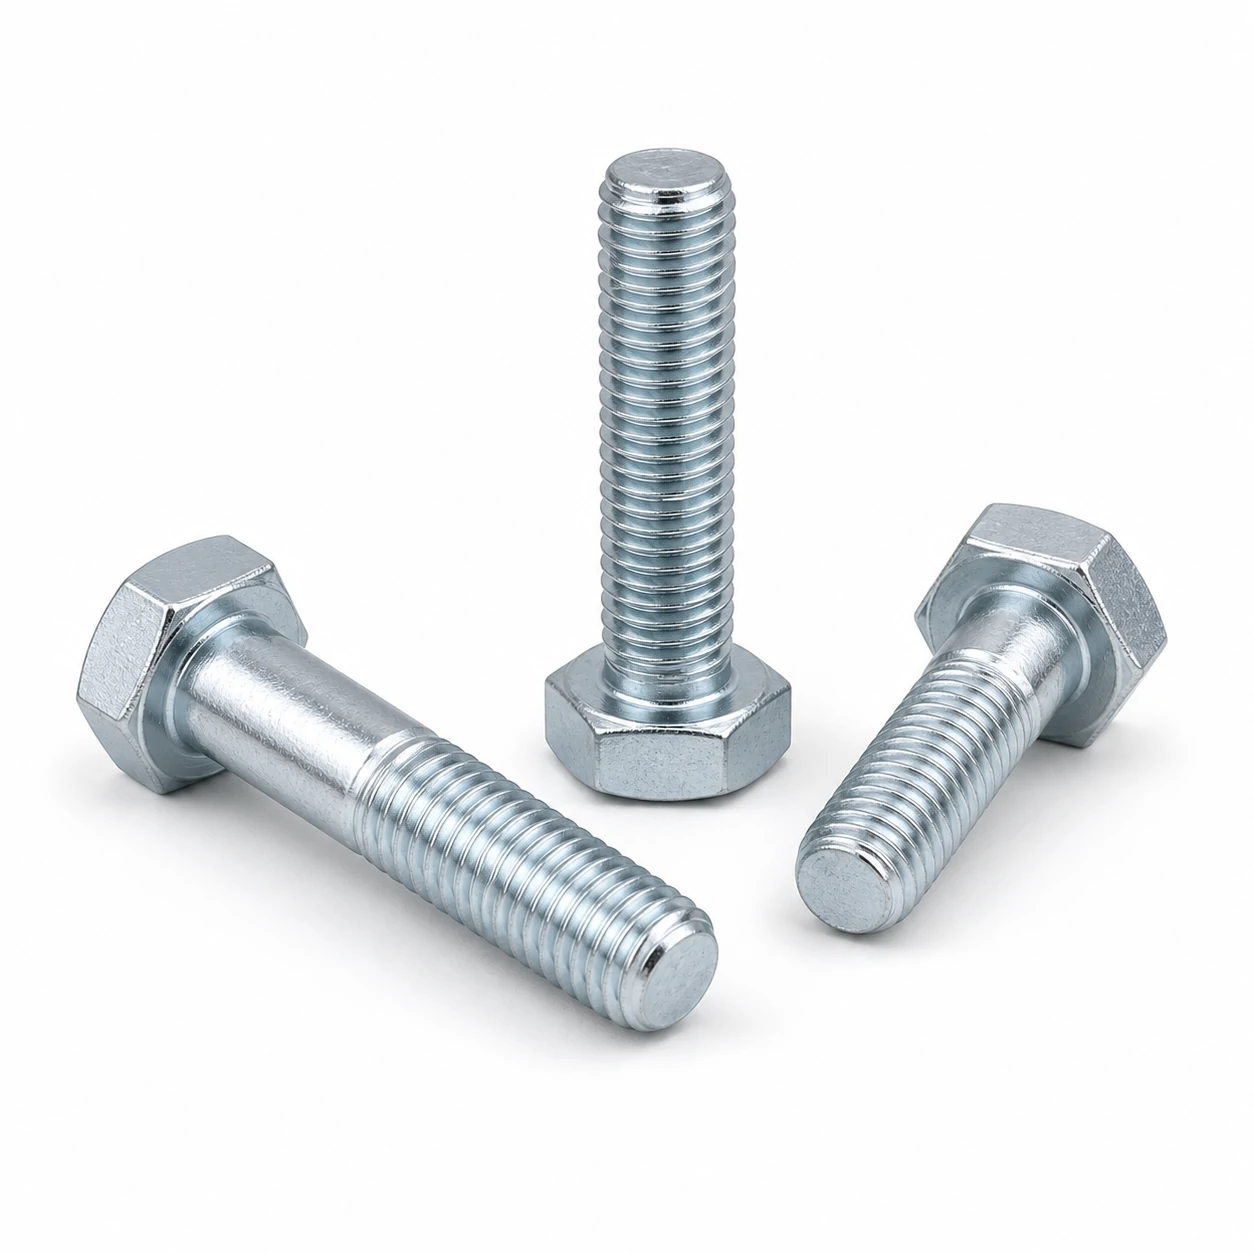
Dimensional and assembly data for M36 Hex Bolts, Grade C to ISO 4016. Includes head size and width across flats, clearance-hole and tapping-drill diameters, tightening torque per property class, and the sizes to step up or down to when the joint requires it.
M36 Dimensional Row (ISO 4016)
| Size | Pitch (mm) | Width across flats s (mm) | Width across corners e min (mm) | Head height k (mm) | Product grade | Reference standard |
|---|---|---|---|---|---|---|
| M36 | 4.0 | 55.0 | 60.79 | 23.35 | Grade C | ISO 4016 / DIN 601 |
Spanner & Drive for M36 Hex Bolts, Grade C
M36 Hex Bolts, Grade C have a width across flats of 55.0 mm — fit a 55.0 mm open-ended spanner or socket. In tight access a 6-point socket on the 55.0 mm flats gives the most engagement per degree of swing. Where the joint is torqued to a figure, a click wrench is the only way to reproduce it across a batch.
Hole Sizes for M36
| Coarse-thread pitch (ISO 724) | 4 mm |
|---|---|
| Through-hole / clearance (ISO 273 medium) | 39 mm |
| Tapping drill, coarse thread | 32 mm |
Tightening Torque for M36
| Class 8.8 (dry, ~µ 0.125) | ≈ 2523 Nm |
|---|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ 3593 Nm |
| Class 12.9 (dry, ~µ 0.125) | ≈ 4204 Nm |
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M36
| Tensile stress area As (ISO 724) | 817 mm² |
|---|---|
| Proof load, class 8.8 | 490 kN |
| Proof load, class 10.9 | 678 kN |
| Proof load, class 12.9 | 792 kN |
| Min. ultimate tensile load, class 8.8 | 678 kN |
Proof load = tensile stress area × the proof stress Sp of the class, per ISO 898-1 — Sp is a lower figure than the yield stress Rp0.2 and the two are not interchangeable. The stress area is computed from this size's own diameter and pitch, so a fine-pitch designation gives the fine-pitch figure. Design the joint so the working preload stays below the proof load of the class selected.
Installation Tips for M36 Hex Bolts, Grade C
- Use a 6-point socket where access allows — 12-point sockets are more prone to rounding the corners on smaller sizes.
- Serrated flanges need to sit directly on the joint face. A washer between the two removes the bite and leaves an ordinary bolted joint that is believed to be a locking one.
- At M36 the stretch in the bolt becomes the controlling factor — for critical joints, use angle-controlled or stretch-controlled tightening instead of pure torque.
Mating Parts for M36
For M36, pair with a M36 hex nut (ISO 4032 / DIN 934) and, where used, a M36 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
Custom manufacturing · Made to drawing
Need hex bolts, grade c in a size this table does not list?
This page covers M36 hex bolts, grade c. Lengths and thread lengths outside the standard table are the commonest request, followed by a drive the standard does not offer and a head marked with your own part number. Made by cold heading or hot forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.