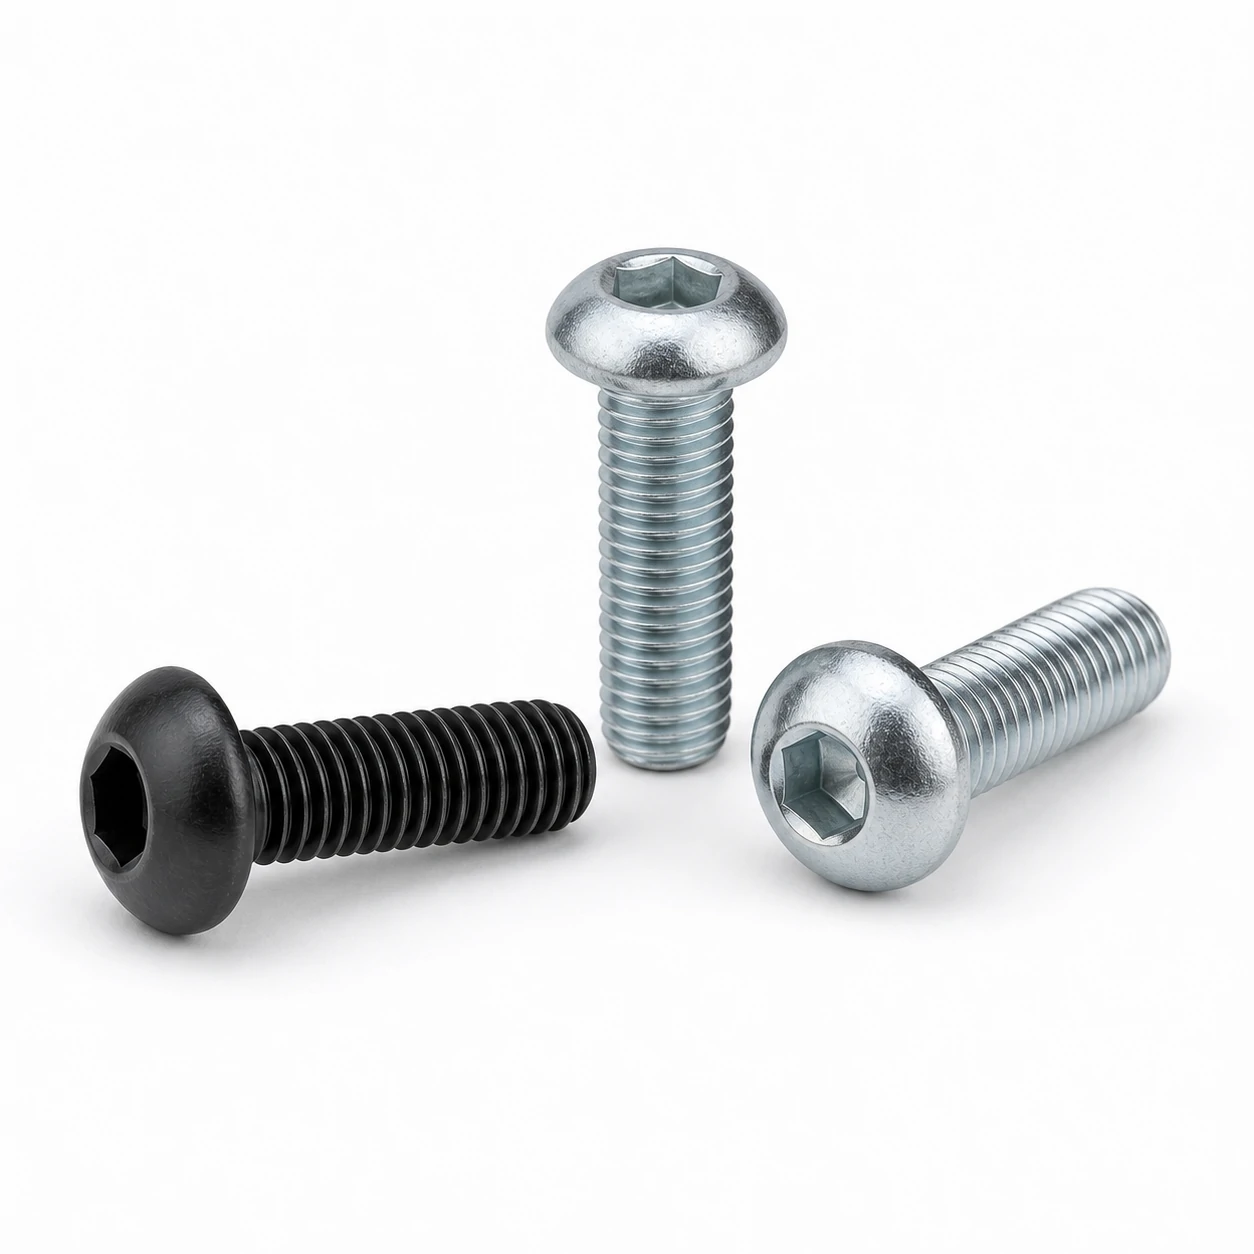
M3 Button Head Socket Screws dimensions to ISO 7380: head diameter 5.7 mm, head height 1.65 mm, coarse thread pitch 0.5 mm, clearance hole (ISO 273 medium) 3.4 mm. Tighten to approximately 1.3 Nm at property class 8.8 in a dry, as-supplied condition.
- Head diameter
- 5.7 mm
- Head height
- 1.65 mm
- Coarse thread pitch
- 0.5 mm
- Clearance hole (ISO 273 medium)
- 3.4 mm
- Tightening torque (class 8.8)
- 1.3 Nm
Figures are nominal values from the governing standard. Confirm against the tolerance class for your application before machining or ordering.
M3 Button Head Socket Screws (ISO 7380) are specified by thread size, length and head dimensions. The M3 row from the standard is reproduced below, followed by the drill sizes, spanner size and torque values used when installing this size.
M3 Dimensional Row (ISO 7380)
| Size | Pitch (mm) | Head diameter dk (mm) | Head height k (mm) | Hex socket s (mm) | Reference standard |
|---|
| M3 | 0.5 | 5.7 | 1.65 | 2.0 | ISO 7380-1 / DIN 7380 |
Spanner & Drive for M3 Button Head Socket Screws
The hex socket for M3 Button Head Socket Screws is shown in the spec table — use the matching Allen / hex key (an ISO 2936 hex key set covers the full range). For a one-off, a T-handle key and a calibrated arm will do. For a batch, the only way to get the same preload twice is a torque-controlled driver.
Hole Sizes for M3
| Coarse-thread pitch (ISO 724) | 0.5 mm |
|---|
| Through-hole / clearance (ISO 273 medium) | 3.4 mm |
|---|
| Tapping drill, coarse thread | 2.5 mm |
|---|
Tightening Torque for M3
| Class 8.8 (dry, ~µ 0.125) | ≈ 1.3 Nm |
|---|
| Class 10.9 (dry, ~µ 0.125) | ≈ Nm |
|---|
| Class 12.9 (dry, ~µ 0.125) | ≈ 2.2 Nm |
|---|
Indicative dry-joint values. Lubrication can lower the required torque by 15–25%. Always confirm against the joint design, especially when going up a strength class.
Proof Load & Strength for M3
This is a reduced-height head. The head, not the thread, limits what the screw will carry — ISO 7380-1 caps a button head at roughly 80% of the thread's capacity — so the thread's proof load overstates the assembly. Size the joint on the head, or use a cap screw where the full class strength is needed.
Mating Parts for M3
For M3, pair with a M3 hex nut (ISO 4032 / DIN 934) and, where used, a M3 flat washer (ISO 7089 / DIN 125A) under the head and under the nut.
When to Step Up or Down from M3
When the joint preload approaches the proof load of M3 class 8.8, step up to M4 class 8.8 (or move to M3 class 10.9). When the joint is over-specified, M2 often saves weight and cost without losing the safety margin.
Custom manufacturing · Made to drawing
Need button head socket screws in a size this table does not list?
This page covers M3 button head socket screws. Where the standard stops, the drawing takes over: fine pitches, left-hand threads, partial threading, and property classes above the catalogued grade where material and heat treatment allow. Made by cold heading or warm forging.
Minimum order from 2,000 pieces; samples within 7 days of drawing approval.
Custom screw manufacturingSend a drawing
Applications & Industries for M3 Button Head Socket Screws
The sectors that buy Button Head Socket Screws to ISO 7380, and the duty each one buys them for. Stocked from M3 to M20.
Industries that specify Button Head Socket Screws
-
Automotive & transport
Chassis, driveline and body fixings that see vibration and are assembled to a controlled preload.
-
Steel fabrication
Bolted connections in frames, enclosures, walkways and weldments, on the bench and on site.
-
Energy & infrastructure
Tower, pipework, switchgear and plant fixings specified for long service life and inspectable joints.
-
Maintenance & MRO
Stocked replacements matched to an existing property class, thread and finish.
-
Food, pharma & cleanroom
Stainless assemblies that are washed down, where the finish matters as much as the strength.
-
Machine building & OEM
The default fastener on production equipment: covers, brackets, motor mounts and sub-assemblies tightened to a specified torque.
Typical applications
- bolting brackets, motors and gearboxes to a frame
- assemblies that are dismantled for service and re-torqued
- joints where the property class is stated on the drawing
- clamping two machined faces to a calculated preload
Service conditions to specify against
- Marine and coastal
- Available in A4 (316) stainless for chloride exposure — coastal structures, pool halls, water treatment and deck hardware, where A2 will eventually pit.
- High load
- Supplied in ISO 898-1 property classes, so the joint can be designed to a stated proof load and tightened to a calculated torque rather than by feel.
- Torque and preload
- The joint is designed around bolt tension, so lubrication, coating and the friction coefficient all change the torque figure — state them together.
Where to use something else
- Do not use a machine thread into unthreaded sheet or timber; use a tapping screw, rivet nut or insert made for that parent material.
Full application guide: where Button Head Socket Screws are used, how to specify them, and the cases they are wrong for